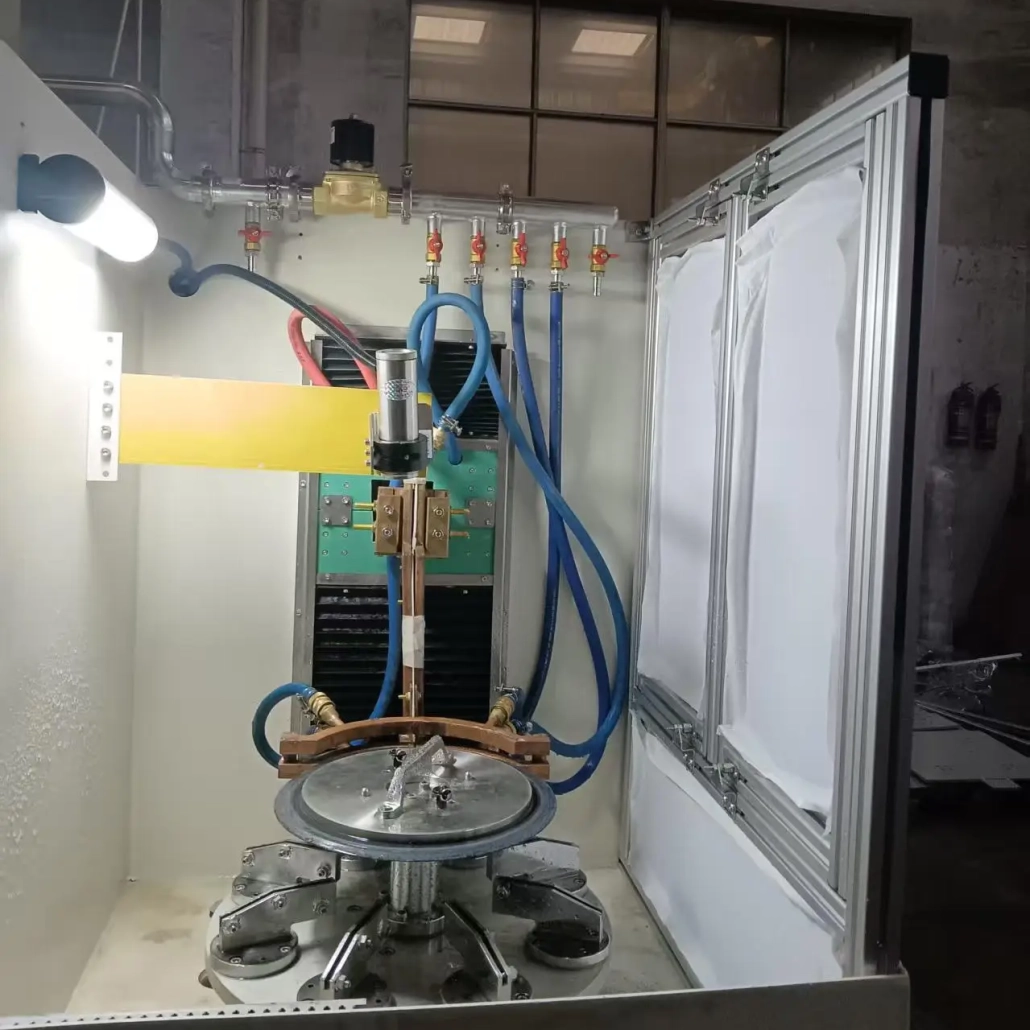
Автоматическая машина индукционной закалки лезвий
Ⅰ. See the Blade Hardening Machine in Operation
The two videos show the same induction hardening system processing two different blade designs.
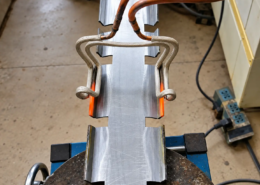
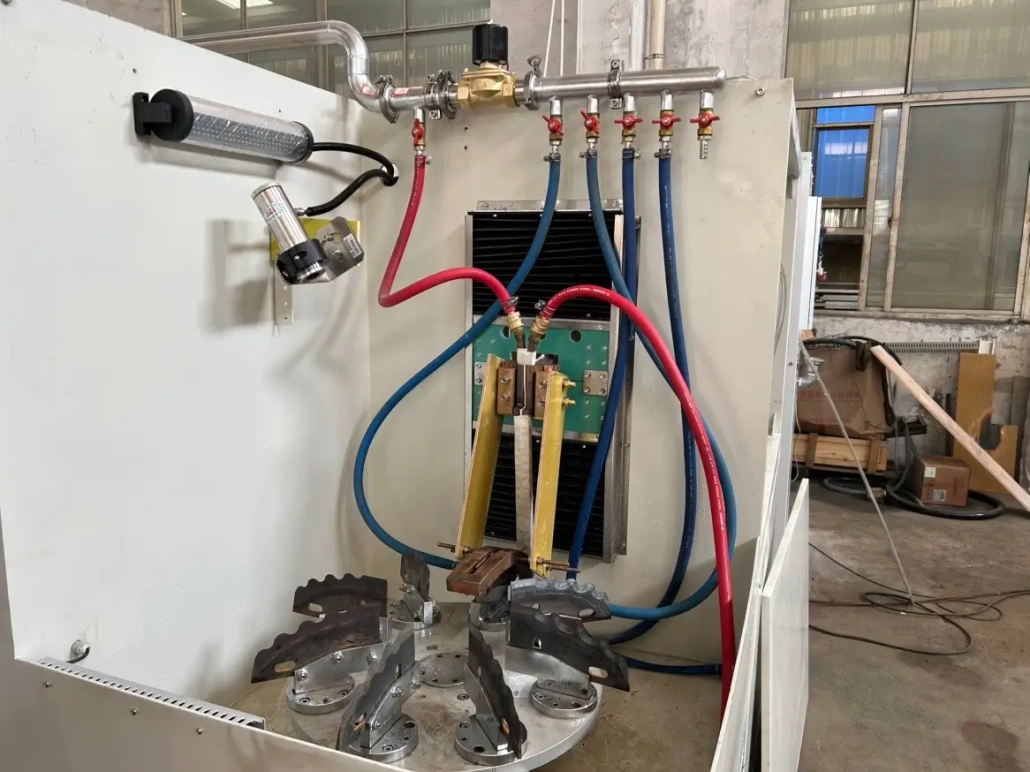
The first application uses a dedicated fixture and compact inductor for an irregular-profile cutting blade. Several blades are positioned in the fixture for repeated edge hardening.
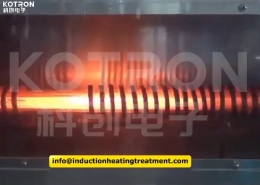
The second application uses a different support arrangement for a circular blade. Its outer edge passes through an inductor positioned around the blade edge while the workpiece rotates through the heating zone.
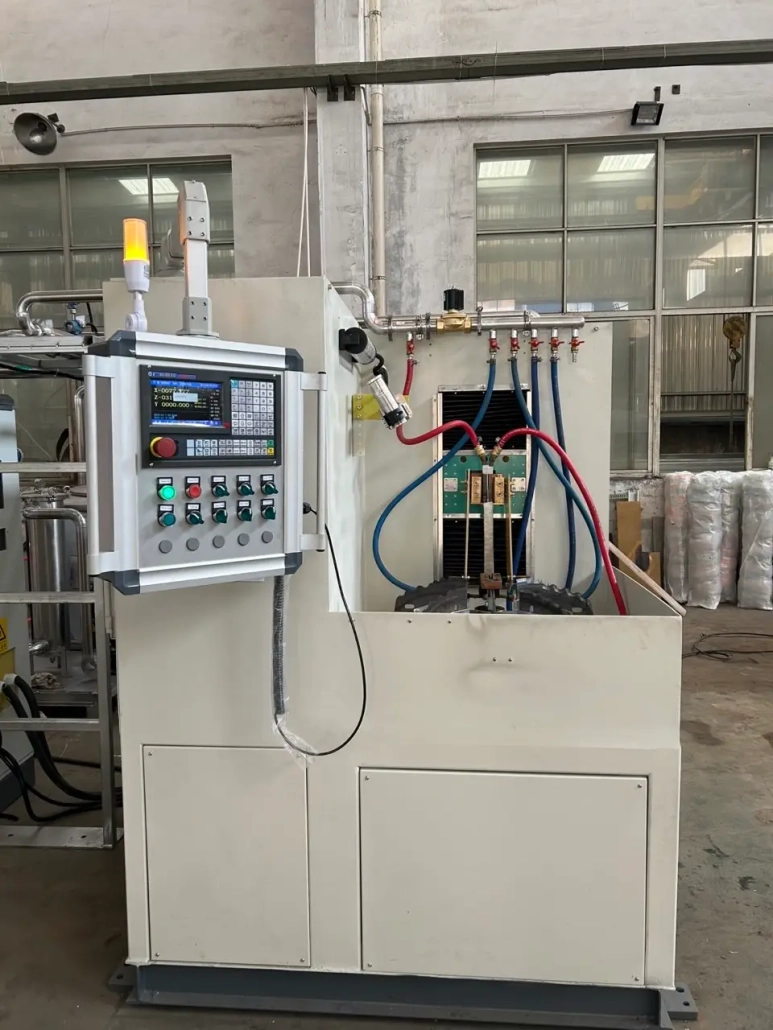
The machine platform is the same. The tooling and hardening method change with the blade.
Irregular Blade Induction Hardening Machine | Custom Hardening Solution
Circular Blade Induction Hardening Machine | Edge Hardening Process
Ⅱ. Two Blade Profiles, Two Hardening Approaches
These two applications show why blade hardening cannot be treated as a single standard process.
For the irregular-profile blade, the cutting edge follows a shaped contour. The workpiece is located in a dedicated fixture so that the required edge area remains correctly positioned relative to the inductor.
A compact inductor concentrates heating on the cutting area, while the quenching arrangement is positioned close to the heating zone. This allows the heated edge to be cooled immediately after the required heating cycle.
The circular blade requires a different solution.
It is supported around the center while the outer edge passes through an inductor positioned on both sides of the blade edge. The inductor does not mechanically clamp the workpiece; a controlled gap is maintained between the blade and the heating element.
As the blade rotates, the circumference passes continuously through the same heating zone.
The two processes are different, but the engineering principle is the same:
Blade profile → приспособление → Индуктор → Movement → Heating zone → закалка
Ⅲ. Why Use Localized Edge Hardening?
The cutting edge and the blade body do different jobs.
After grinding, the cutting edge has a relatively thin geometry and is the part directly exposed to friction, wear and repeated contact during operation. It therefore requires sufficient hardness and wear resistance to maintain its cutting performance.
The blade body, однако, still needs suitable toughness for mechanical loading, vibration or impact.
Индукционный нагрев allows the thermal input to be concentrated on the selected edge area instead of heating the complete blade in the same way.
For blade applications, the objective is not simply to increase hardness across the whole workpiece. The process is developed around the area that actually needs hardening.
Ⅳ. Custom Fixture and Inductor Design
The fixture and индукционная катушка are two of the most important parts of a blade hardening solution.
A blade with an irregular edge cannot be positioned in the same way as a circular blade. Their heating paths, support points and available space around the cutting edge are different.
The fixture establishes the relationship between the blade and the induction coil during processing. В зависимости от заготовки, it may need to provide:
The induction coil is then designed around the area that must be heated.
For the irregular blade shown in the first video, the inductor is concentrated around a relatively small edge-heating area.
For the circular blade, the inductor surrounds the outer edge from both sides while the workpiece rotates through the heating zone.
There is no universal blade fixture or induction coil that is suitable for every blade geometry.
Ⅴ. Built for Batch Blade Hardening
The system is intended for repeated blade production rather than occasional manual heating.
In the first application, several blades are positioned in a dedicated fixture. This allows the relationship between each cutting edge and the hardening position to be established by the tooling instead of being recreated manually for every part.
Для batch heat treatment, this repeatable positioning matters.
Small changes in the distance or orientation between the cutting edge and the induction coil can affect the heating condition. A purpose-built fixture helps reduce this variation from one workpiece to the next.
The final production arrangement can be developed according to:
The equipment layout does not need to remain identical for every blade project.
Ⅵ. Digital Induction Power and Process Control
Repeatable positioning must be matched by controlled induction heating.
The digital induction power system can display and monitor operating information such as:
These operating values help the operator follow the heating process and check whether the equipment is running within the established production condition.
Different blade geometries may require different heating settings. The values shown in the video are therefore the real-time operating condition of that particular process, not universal specifications for every blade.
Additional recipe management, тревога, data-recording or automation functions can be configured according to the final control system required for the project.
Ⅶ. A Hardening Solution Configured Around Your Blade
The two blade applications shown on this page were processed on the same equipment platform, but they do not use the same tooling or heating method.
That is the point of the system.
For a new blade, the process starts with the workpiece rather than with a fixed machine specification.
We evaluate factors such as:
Из этой информации, приспособление, индукционная катушка, позиция нагрева, movement and quenching arrangement can be developed together.
Some new products may require only a different fixture and inductor. Others may require changes to the workpiece support, motion or production sequence.
The machine is therefore better understood as a proven blade-hardening platform that can be adapted to different cutting-tool applications.
Ⅷ. What We Need From Your Blade
A workpiece drawing is usually the best starting point for a blade hardening project.
Пожалуйста, предоставьте следующую информацию, если она доступна.:
For irregular blades, marking the required hardened area directly on the drawing is particularly useful.
На основе этой информации, we can evaluate the workholding method, индукционная катушка, процесс нагрева, quenching arrangement and production configuration together.
Ⅸ. Часто задаваемые вопросы
Нажмите на вопрос, чтобы развернуть ответ.
Can one machine process different blade profiles?
Does every blade need a different induction coil?
Can only the cutting edge be hardened?
What determines the hardened depth?
Can the system be automated further?
Request a Custom Hardening Solution for Your Blade
Send your blade drawing and requirements. We will evaluate the fixture, индукционная катушка, heating process and quenching arrangement together.
Send Your Blade Drawing →
Request a Custom Hardening Solution