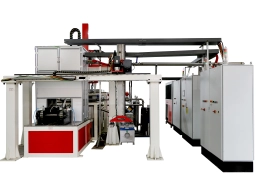
Станок для индукционной закалки винтовых валов с ЧПУ для ходовых винтов и резьбовых валов
Ⅰ. CNC Induction Hardening for Screw Shafts and Lead Screws
CNC Induction Hardening for Screw Shafts and Lead Screws
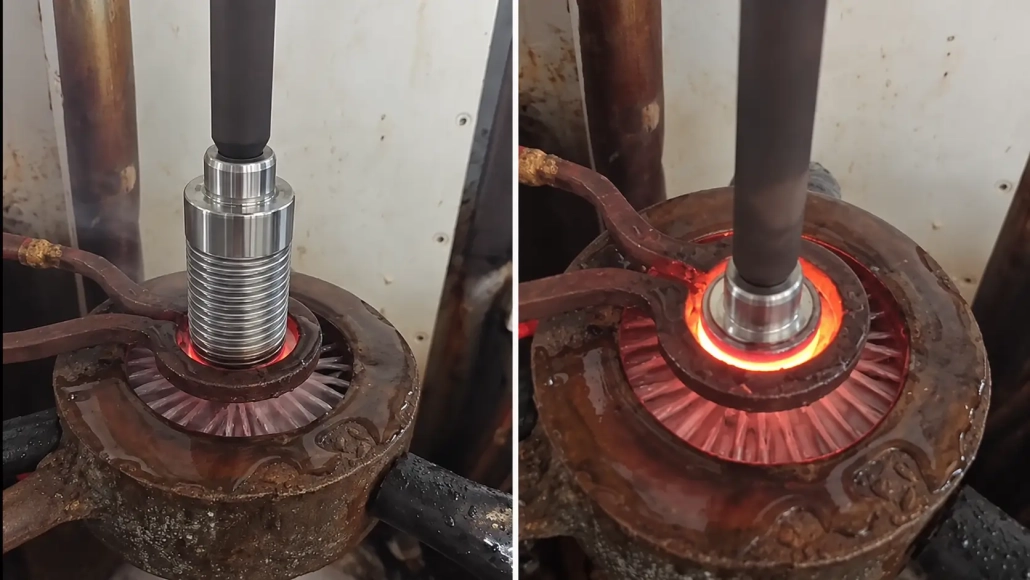
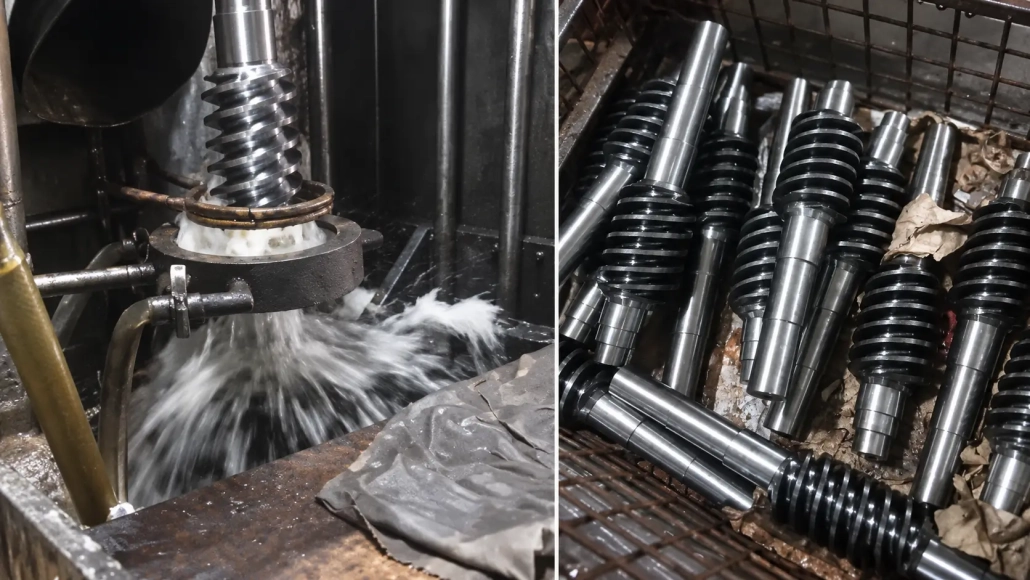
The video shows continuous scan heating along the threaded section of a screw shaft.
Instead of heating the entire threaded length at once, the heating zone travels progressively along the workpiece. CNC control maintains the programmed scan movement through the required treatment area.
This type of process is suited to screw shafts where the hardened zone extends over a relatively long threaded section.
Scan hardening sequence
①Set the scan start point, end point and treatment length
②Heating zone travels progressively along the threaded section
③CNC control maintains the programmed scan movement
Ⅱ. Why Threaded Shafts Require Different Process Control
А smooth shaft presents a relatively simple cylindrical surface to the induction field. A screw shaft does not.
Its working surface consists of:
•thread crests
•thread flanks
•thread roots
•a continuous helical profile
The local relationship between the workpiece surface and the inductor changes across that profile. Как результат, the crest and root may not heat at the same rate under the same process conditions.
For screw shaft induction hardening, the objective is therefore not simply to heat the outside diameter. The heating pattern needs to cover the required thread profile and follow the specified working length.
Inductor arrangement, муфта, scan speed and electrical settings all need to be matched to the actual part. The required result should ultimately be judged against the drawing and hardening specification rather than by appearance during heating.
Ⅲ. Controlled Scan Heating Along the Threaded Section
The main process feature of this machine is CNC-controlled scan hardening.
A controlled scan speed helps maintain more repeatable heat input as the heating zone travels along the screw. The scan start point, end point and treatment length can be set according to the required hardening area.
For precision threaded parts, this is particularly useful when only the functional thread section needs to be hardened.
The appropriate scan conditions depend on factors such as:
•thread geometry
•threaded length
•workpiece diameter
•Материал
•требуемую закаленную область
•требуемая твердость и глубина корпуса, когда указано
These factors need to be considered together. Increasing power alone, например, does not necessarily correct an unsuitable hardening pattern between the thread crest and root.
Ⅳ. Hardening Across the Thread Crest and Root
The thread profile is the main difference between lead screw hardening and ordinary cylindrical shaft hardening.
The crest is more exposed, while the root is recessed between adjacent threads. Because of this geometry, an unsuitable process may concentrate heating in one part of the profile while another part receives less effective heating.
The machine and process are intended to support a more even hardening pattern across the functional thread surface, including the crest and root.
The achievable result still depends on the actual thread profile, Материал, inductor relationship and selected process settings. Для критически важных деталей, hardness distribution and case depth should be verified according to the customer’s inspection requirements.
Ⅴ. Typical Workpieces
The machine can be configured around different screw-shaft geometries within the intended processing range.
Типичные области применения включают в себя:
Precision Screw Shafts
Threaded shafts where wear resistance and dimensional control of the working section are important.
Trapezoidal Lead Screws
Lead screws with trapezoidal thread profiles used in mechanical transmission or linear-motion systems.
Conveyor Screws
Screw-type components with helical working surfaces that require localized hardening of the wear area.
Other Threaded Shafts
Externally threaded shaft components where the required hardening zone extends along part or all of the threaded working section.
Different thread profiles, diameters and pitches may require different process settings and tooling. They should not be treated as interchangeable applications simply because the overall shaft diameter is similar.
Ⅵ. Long Screw Shafts and Dimensional Control
Precision screw shafts can be sensitive to dimensional change during heat treatment, particularly when the hardened section is long.
Heating distribution along the shaft should therefore be considered together with the required straightness, runout and final dimensional tolerance.
Controlled scanning can help avoid abrupt changes in heat input along the treatment length, but the final dimensional result also depends on the workpiece geometry, material condition and the complete hardening process.
For parts with tight dimensional requirements, those limits should be identified before the process and machine configuration are finalized.
Ⅶ. Information Used to Configure the Machine
The machine should be selected around the actual screw shaft rather than from shaft length or power alone.
| Workpiece information | Почему это важно |
|---|---|
| Screw or thread profile | Affects heating distribution and tooling arrangement |
| Major and minor diameter | Defines the working geometry around the thread |
| Threaded-section length | Determines the required scan range |
| Overall part dimensions | Affects workpiece support and machine travel |
| Материал | Influences the hardening response |
| Требуемая закаленная площадь | Defines where the scan should start and stop |
| Твёрдость / case depth requirement | Used to establish the process target when specified |
| Требования к размерам | Relevant for precision and long screw shafts |
| Производственное требование | Helps determine the appropriate machine configuration |
A part drawing with the required hardened area marked is usually enough to begin the technical evaluation.
Ⅷ. Часто задаваемые вопросы
Нажмите на вопрос, чтобы развернуть ответ.
+ Can both the thread crest and thread root be hardened?
The process can be developed to provide hardening coverage across the thread profile, including the crest and root. The final pattern depends on the actual thread geometry, material and process conditions.
+ Is CNC scan hardening suitable for long lead screws?
It can be suitable when the required hardened area extends along a long threaded section. The heating zone is scanned along the specified treatment length rather than requiring the complete section to be heated at one time.
+ Can the same machine process different screw shafts?
A machine can be configured for multiple parts within its designed range, but changes in diameter, pitch and thread profile may require different tooling and process settings.
+ Is higher power the main way to improve root hardening?
Сама по себе — нет. Heating distribution also depends on the thread geometry, муфта, расположение индуктора, frequency and scan conditions. Power should be considered as part of the complete process rather than as an independent solution.
Ⅸ. Send Your Screw Shaft Drawing
Для первоначальной оценки, send us the screw shaft drawing or basic part dimensions together with the required hardening area. If hardness or case-depth requirements are already specified, их тоже можно включить. We can then evaluate the scan-hardening arrangement and machine configuration according to the application.