
Validação do Processo de Endurecimento por Indução: Qualificação, Teste e Requalificação
Como verificar os resultados do endurecimento, Assess Process Changes and Determine When Requalification Is Needed
An induction-hardened component may meet its surface hardness requirement but still have insufficient case depth, an incorrect hardened pattern, or inconsistent results between parts. A passing hardness test alone does not prove that the process is suitable for production.
Induction hardening process validation establishes evidence that a defined combination of equipment, ferramentas, material, configurações de aquecimento, and quenching conditions can produce parts meeting specified requirements. It also establishes the basis for deciding whether later process changes require additional verification or requalification.
2. How to Validate an Induction Hardening Process
3. When Is Induction Hardening Requalification Required?
4. What If Induction Hardening Process Validation Fails?
5. Qualification Records and Production Control
1. What Is Induction Hardening Process Validation?
Process validation demonstrates that an induction hardening process can achieve its intended results under defined conditions. Process qualification refers to the formal acceptance of that process under the applicable approval procedure.
Before qualification trials, the manufacturer must establish the component’s acceptance requirements:
•Material and initial condition: Classe de aço, tratamento térmico prévio, and starting microstructure can influence hardenability and the resulting hardened case.
•Required hardened region: The drawing should identify the surfaces and locations where hardening is required.
•Dureza e profundidade da caixa: Acceptance criteria must specify the required hardness, measurement locations, and applicable case-depth definition.
•Additional requirements: Dependendo do componente, these may include hardened-pattern evaluation, inspeção de fissuras, microestrutura, distorção, or dimensional checks.
Qualification must also identify the process conditions that affect these results.
| Process Condition | Potential Effect |
|---|---|
| Potência, frequência, e o tempo de aquecimento | Heating characteristics and thermal cycle |
| Inductor geometry and coil-to-part gap | Heating distribution and hardened-pattern location |
| Scan speed and workpiece positioning | Heating exposure and consistency |
| Quench flow, distribution, temperatura, and timing | Cooling conditions and hardening response |
| Material and initial condition | Hardenability and resulting case characteristics |
The objective is to establish a qualified process window supported by actual trials, not simply record the settings available on the machine.
2. How to Validate an Induction Hardening Process
A practical validation procedure connects the component requirements with representative trials and documented inspection results.
①Define the Qualification Scope
Identify the workpiece, condição material, drawing revision, equipamento, indutor, luminária, heating program, and quenching arrangement.
②Establish Trial Conditions
Develop initial heating and quenching settings based on the required hardened region, material, geometria, e configuração de equipamentos.
These are development settings until qualification evidence supports their approval.
③Conduct Representative Trials
Use workpieces representative of the intended production process. Consider relevant variation in material condition, geometria, posicionamento, and production conditions.
Para têmpera indutiva por varrimento, the trial plan may need to examine the scan-start, central, and scan-end regions. If an operating range is proposed, its relevant limits must be evaluated rather than assuming that one successful nominal setting qualifies the entire range.
④Verify the Hardening Results
Compare the tested parts with the specified acceptance criteria. Dependendo da aplicação, this may involve surface hardness, travessias de dureza, profundidade efetiva da caixa, hardened-pattern location, inspeção de fissuras, e verificações dimensionais.
For detailed inspection methods, ver Como inspecionar peças endurecidas por indução: Por que a dureza superficial por si só não é suficiente.
⑤Approve the Qualified Conditions
If the required results are achieved, document the process configuration, supported operating limits, inspection evidence, and approvals.
Passing product inspection demonstrates compliance for the tested parts. It does not automatically qualify untested materials, equipment configurations, or parameter ranges.
Exemplo: Scanned Induction Hardening of a Shaft
Considere uma steel shaft requiring a specified hardened length, dureza da superfície, and effective case depth.
Trial shafts are processed using a defined inductor, scanning program, heating conditions, and quench arrangement. Inspection covers the required hardened region, including relevant start and end locations.
If the surface hardness is acceptable but the case depth is insufficient near the scan-start area, the process has not met all qualification requirements.
The manufacturer must investigate the result, adjust the process where necessary, and verify the affected characteristics again before approval.
The resulting qualification applies to the defined material, configuração do equipamento, and supported process conditions. It does not automatically extend to a redesigned coil or a different steel grade.
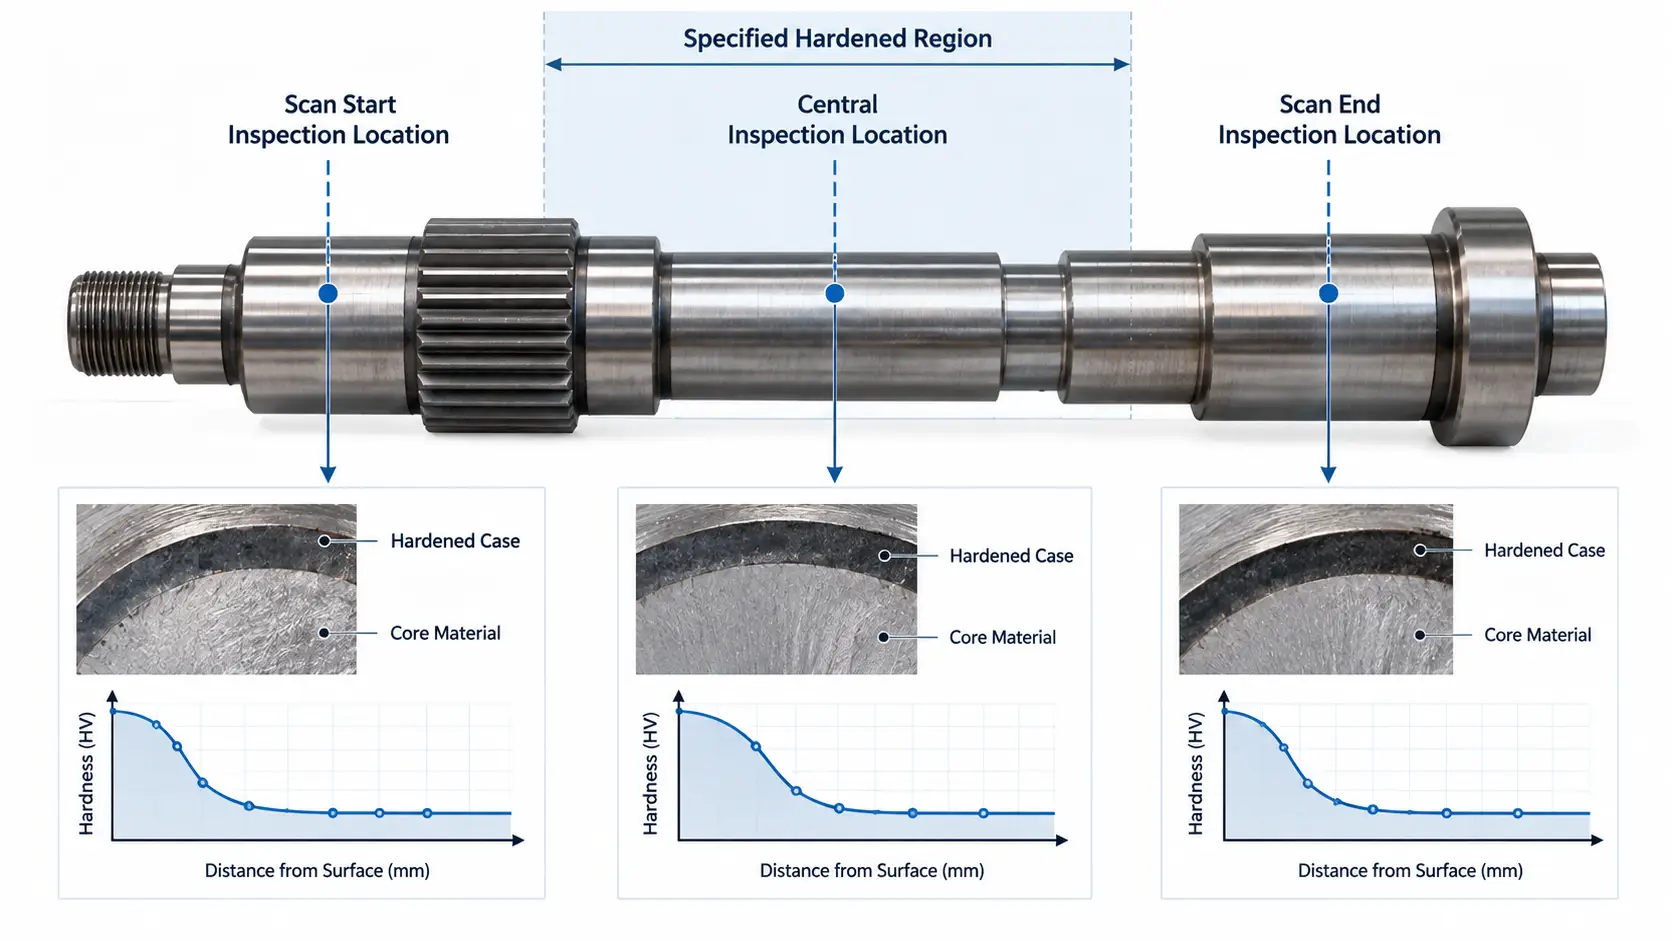
Shaft inspection locations for scanned induction hardening validation.
3. When Is Induction Hardening Requalification Required?
Requalification may be necessary when a change affects conditions covered by the original qualification.
Not every adjustment requires complete requalification. The decision depends on the nature of the change, its potential effect on the hardening result, and applicable customer or quality requirements.
| Process Change | What Should Be Evaluated |
|---|---|
| Induction coil replacement or redesign | Coil equivalence, distribuição de aquecimento, and hardened-pattern consistency |
| Power supply or heating program change | Effects on the heating cycle and approved operating limits |
| Scan speed or fixture adjustment | Posicionamento da peça, heating exposure, and hardened-region location |
| Quenching system modification | Fluxo, spray distribution, as condições de arrefecimento, and hardening response |
| Material or workpiece change | Temperabilidade, geometria, and applicability of existing qualification evidence |
| Equipment relocation or process transfer | Equipment equivalence and the need for additional verification |
Por exemplo, replacing an inductor with a verified equivalent may require a different level of evaluation from installing a redesigned inductor that changes the heating distribution.
Three questions help determine the appropriate response:
①Is the change within the qualified configuration and approved operating limits?
②Could it affect hardness, profundidade de camada, hardened-pattern location, or another specified characteristic?
③Do customer specifications or applicable procedures require additional testing or formal approval?
Depending on the answers, the response may involve documented engineering review, targeted product verification, additional qualification trials, or complete requalification.
The important distinction is whether the existing evidence still supports the changed process.
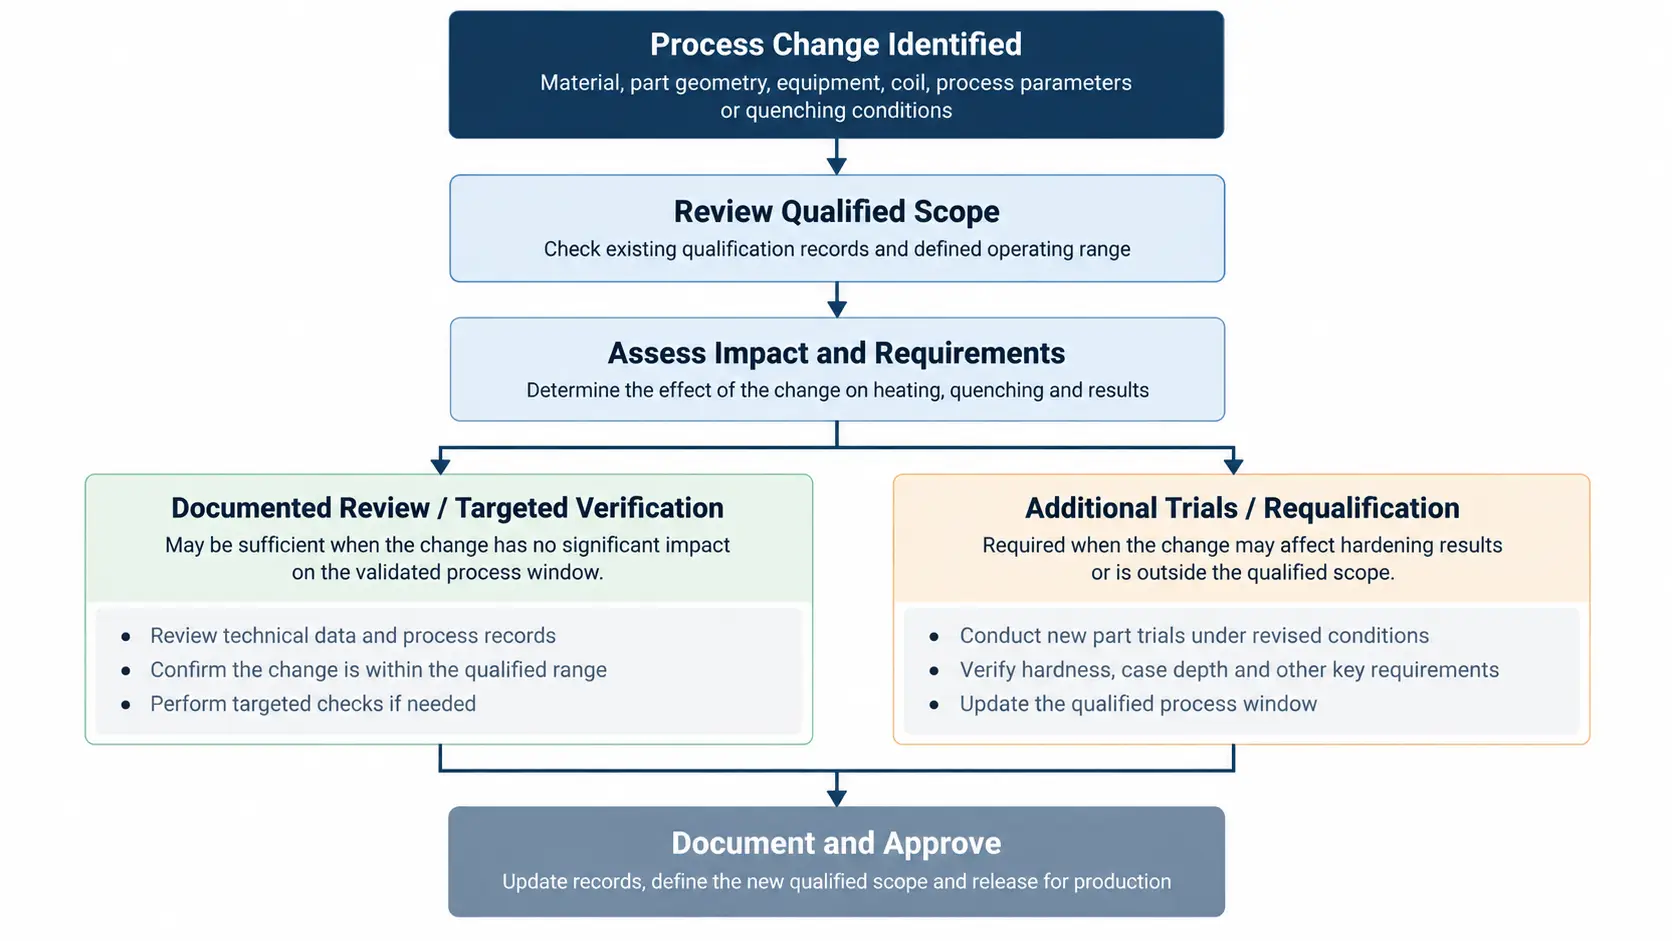
Process change evaluation for induction hardening requalification.
4. What If Induction Hardening Process Validation Fails?
A failed validation result means that the tested conditions have not demonstrated compliance with all specified requirements.
Investigation should begin with the failed characteristic and its location rather than immediately changing machine settings.
| Resultado observado | Investigação Inicial |
|---|---|
| Surface hardness passes, but case depth is insufficient | Confirm the hardness traverse and measurement location; examine the heating cycle, material response, and quenching conditions |
| Hardened pattern is shifted or incomplete | Check inductor position, folga entre bobina e peça, fixture alignment, and workpiece motion |
| Results vary between workpieces | Compare material batches, posicionamento, heating records, and quench delivery |
| Cracks or unacceptable distortion | Examine material condition, geometria, heating and cooling history, and relevant mechanical constraints |
Estas são possíveis direções de investigação, diagnósticos não definitivos.
Por exemplo, an incomplete hardened pattern does not necessarily mean insufficient power. Incorrect coil positioning or workpiece motion may produce a similar result.
After identifying the likely cause, the manufacturer should make controlled adjustments, repeat the necessary tests, and document the results before approving the process.
If a problem is discovered during production, potentially affected parts must be evaluated under the applicable nonconforming-product procedure. Correcting the process does not automatically make previously produced parts acceptable.
5. Qualification Records and Production Control
Once qualified, the approved process should be maintained through controlled production instructions and monitoring.
Relevant records may include material identification, equipment and inductor configuration, heating program, motion settings, condições de têmpera, inspection results, and approved operating limits.
Routine monitoring helps confirm that production follows the qualified conditions, but machine signals alone do not replace required verification of hardness, profundidade de camada, or other product characteristics.
Changes to equipment, ferramentas, materiais, or process settings should follow the applicable change-control procedure.
Industry documents such as ASTM A1100, SAE ARP4715, and AIAG CQI-9 may be relevant to qualification or heat-treating quality requirements. They serve different purposes and are not universally mandatory for every induction hardening application. Their current editions and applicability should be confirmed against the customer’s requirements.
Perguntas frequentes
Clique em uma pergunta para expandir a resposta.
What is the difference between process validation and process qualification?
Process validation demonstrates, through trials and inspection evidence, that the process can achieve its intended results under defined conditions. Process qualification is the formal acceptance of that validated process under the applicable approval procedure.
Does every process change require full requalification?
Não necessariamente. The required response depends on the nature of the change and its potential effect on the hardening result. A change within the qualified configuration and approved operating limits may need only documented review, while a redesigned coil or a different material may require additional trials or complete requalification.
Is a passing hardness test enough to qualify an induction hardening process?
Não. A component can meet its surface hardness requirement yet still have insufficient case depth, an incorrect hardened pattern, or inconsistent results between parts. Qualification evidence should cover every specified characteristic, including case depth, hardened-pattern location, and crack or dimensional checks where required.
Induction Hardening Equipment and Process Development
KOTRON supplies induction heating equipment and customized induction hardening systems for shafts, engrenagens, and other steel components. Share your workpiece drawing and requirements for equipment selection and process development.










