Endurecimento por indução de componentes flyweight para motores diesel marítimos
Ⅰ. Automatic Flyweight Induction Hardening in Operation
Automatic induction hardening of flyweight components for marine diesel engines using a rotary indexing workholding system
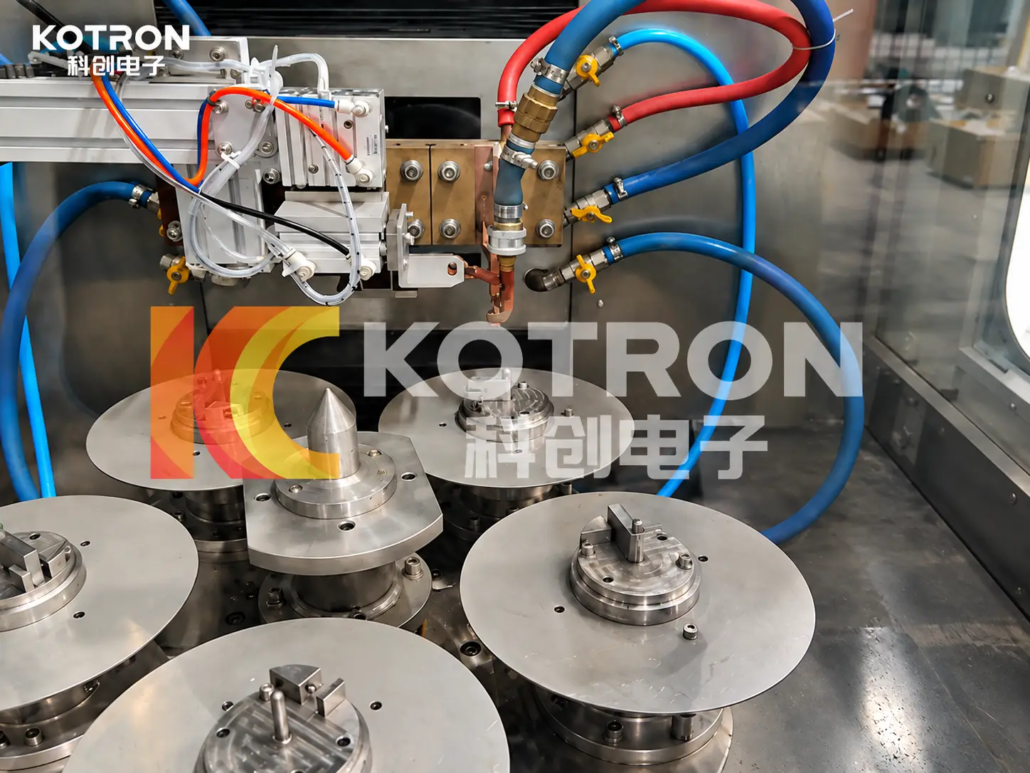
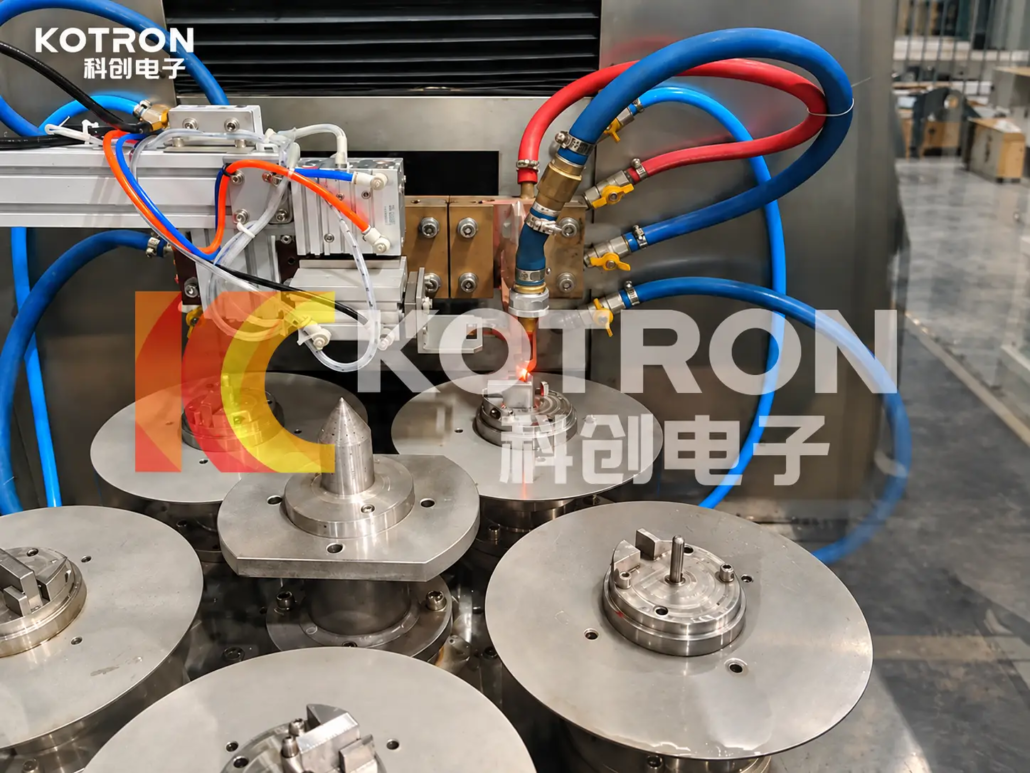
The video shows an enclosed induction hardening machine with several circular workholding plates arranged around a rotary table.
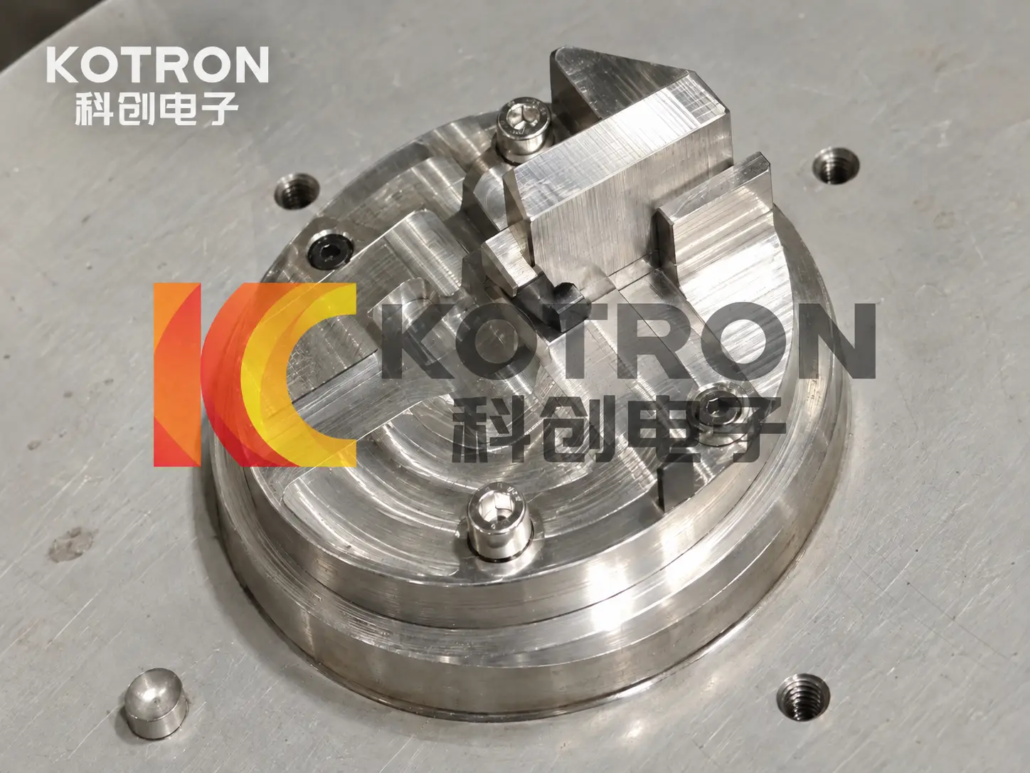
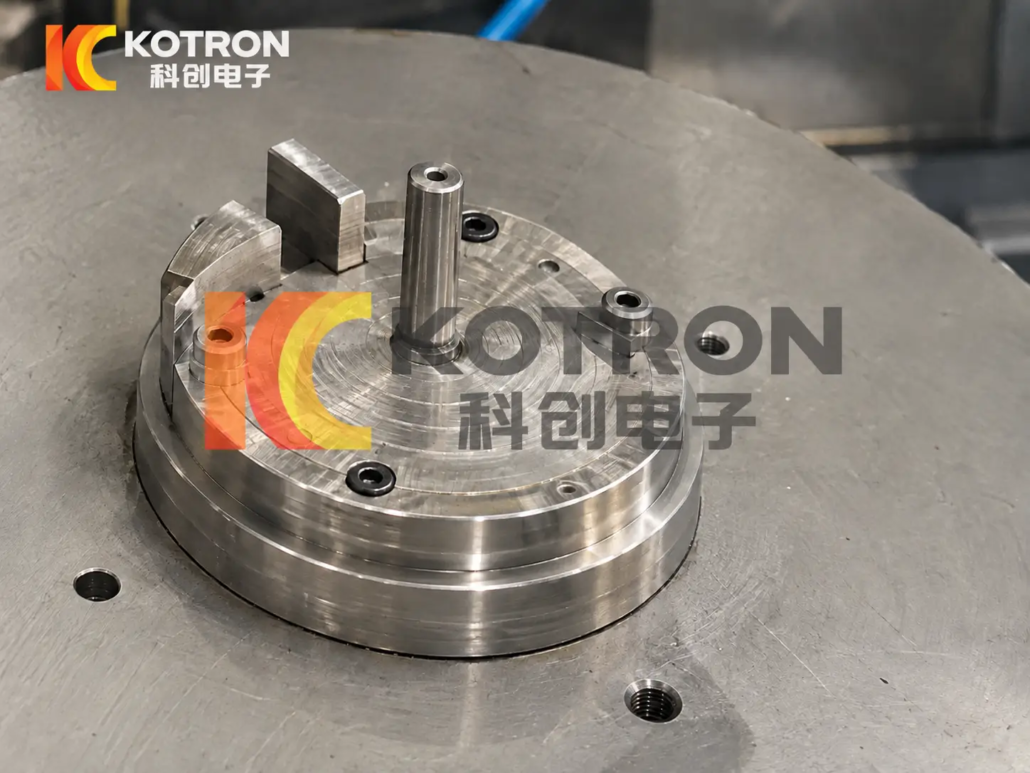
Each plate is fitted with a central locating and clamping fixture for positioning the workpiece. An induction heating head is mounted beside the processing area, with electrical connections and red and blue hoses leading to the assembly.
During the demonstrated heating operation, a localized red-hot region is visible at the workpiece position.
The equipment uses automatic indexing and automatic loading and unloading, allowing the workpieces to be handled and positioned through a coordinated operating sequence.
Configuração do Projeto
| Item | Descrição |
|---|---|
| Peça de Trabalho | Flyweight components |
| Aplicação | Marine diesel engine components |
| Processo | Localized induction hardening |
| Fixação de trabalho | Multiple circular fixtures on a rotary indexing table |
| Arranjo de aquecimento | Induction heating head positioned at the processing station |
| Posicionamento da peça | Automatic rotary indexing |
| Manuseamento de Materiais | Automatic loading and unloading |
| Equipment Structure | Enclosed processing area with observation panels |
| Controlo do Processo | Coordinated heating, indexing and material handling |
The project identifies the workpieces as flyweight components for marine diesel engines. Their precise function within the engine assembly has not been specified.
The footage shows the heating arrangement and localized heating stage. The exact quenching method, installed power supply specifications and final hardness results have not been provided.
Ⅱ. Rotary Indexing and Automatic Workpiece Handling
The rotary indexing arrangement allows several flyweight components to be positioned on the machine while a dedicated induction head performs localized heating at the processing position.
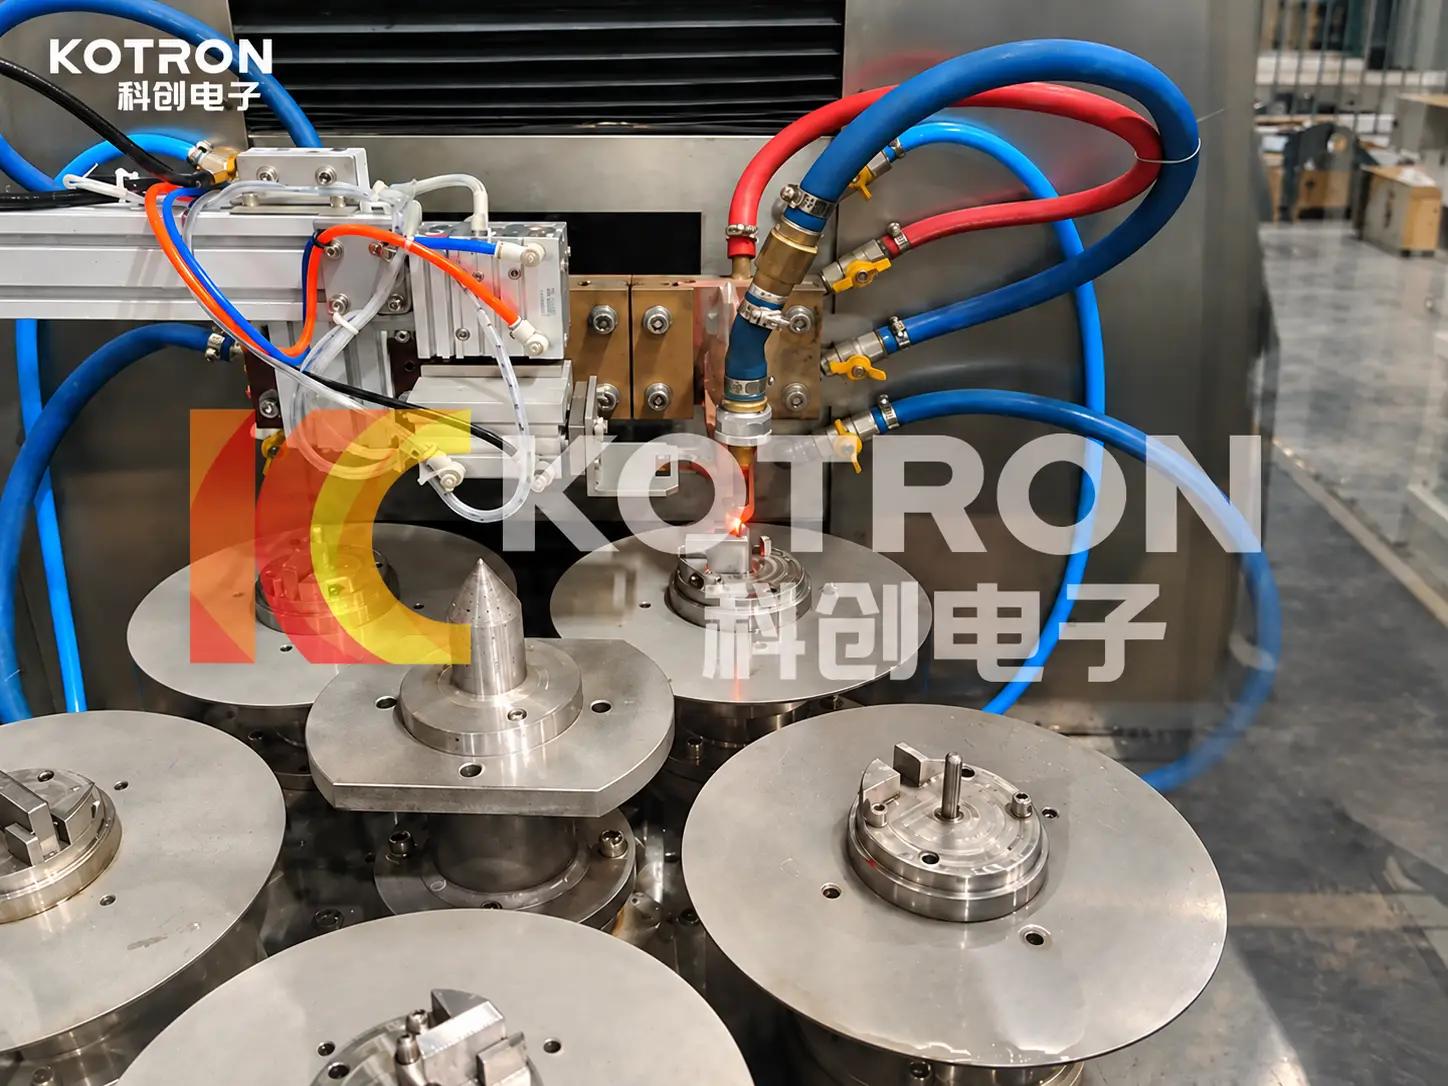
This is different from a conventional shaft scanning hardening machine, where the inductor travels along a relatively long workpiece.
Automatic Loading and Positioning
The machine incorporates automatic loading and unloading to reduce the need for manual handling between processing cycles.
Flyweight components are located in dedicated fixtures mounted on circular workholding plates.
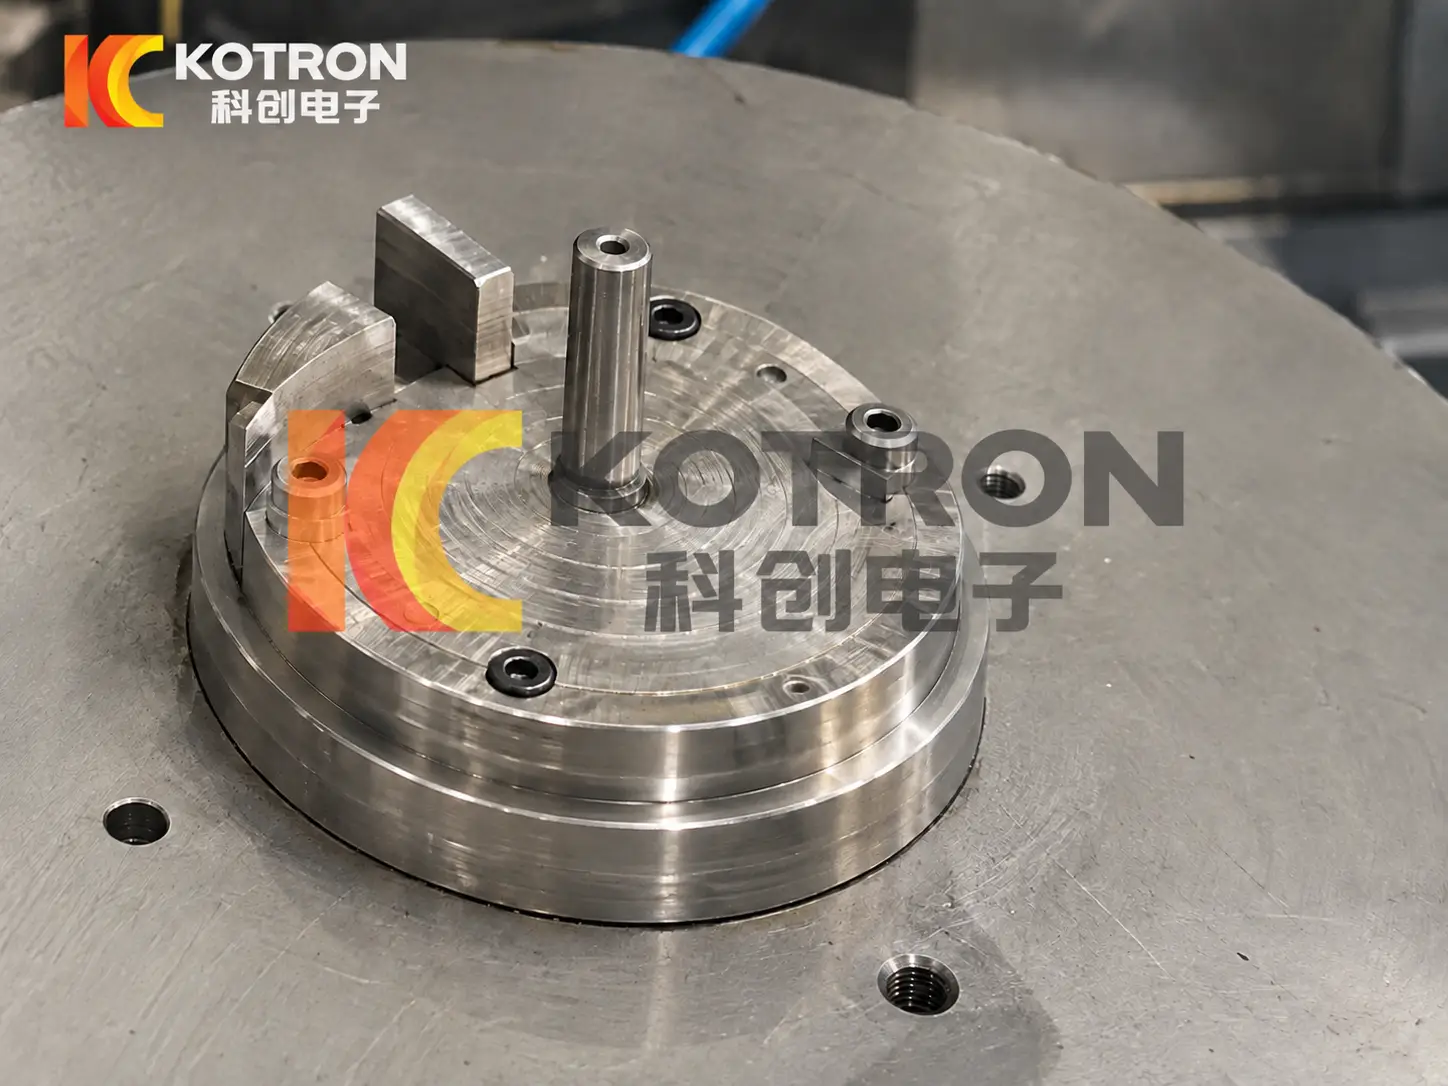
The fixtures must hold each component in the required orientation while providing access to the area selected for hardening. Consistent positioning is particularly important for small components because a change in the distance between the inductor and workpiece can affect electromagnetic coupling and the resulting heating pattern.
Rotary Indexing Process
The indexing mechanism moves the workholding positions through the machine’s operating sequence.
Its movement must be coordinated with workpiece positioning and the induction heating cycle so that heating takes place only when the component is correctly located.
The arrangement supports repeated processing of small components without requiring an operator to manually position every workpiece at the heating head.
The exact indexing sequence and individual station functions are established by the machine design.
Ⅲ. Localized Induction Hardening of Flyweight Components
Flyweight components may have working surfaces that require greater resistance to wear or repeated contact.
For suitable hardenable materials, localized induction hardening can increase surface hardness in selected areas while limiting the need to heat the entire component to the same temperature.
The required hardening pattern must be determined from the actual component drawing and operating conditions.
Custom Inductor and Heating Area
In the demonstrated machine, the induction heating head approaches a defined position on the workpiece held in its fixture.
Projeto de indutor must account for the component’s geometry, the location of the required hardened area and the clearance available around the fixture.
For a small or irregularly shaped part, the relationship between the heating conductor and the target surface can be more important than the overall size of the component.
The principal engineering considerations include:
•Workpiece material and geometry
•Location and extent of the required hardened area
•Inductor shape and coil-to-workpiece clearance
•Available heating power and operating frequency
•Heating time and workpiece positioning
•Dureza necessária e profundidade da caixa, onde especificado
The inductor is developed for the actual component rather than selected solely from the workpiece name.
Heating and Quenching
Induction hardening requires a suitable heating cycle followed by cooling at a rate appropriate for the workpiece material and required hardened structure.
The heating stage must establish the intended temperature distribution in the target area. The subsequent quenching process must then provide the cooling conditions needed for the specified hardening result.
For small components, acesso ao indutor, fixture design and quenching arrangements need to be considered together.
The quenching method and its location within the machine are determined by the project configuration.
Hardening Quality
The finished hardening result depends on the steel grade, heating conditions, quenching process and the geometry of the selected surface.
Surface hardness, effective case depth and the extent of the hardened area can be checked against the customer’s specification through appropriate inspeção and process trials.
The visible red-hot region demonstrates localized heating, but does not by itself establish the final hardness or hardened depth.
Ⅳ. Induction Hardening Equipment and Automation Configuration
Kechuang supplies induction hardening equipment for small mechanical components, with the power supply, workholding system and automation developed around the required processing sequence.
The flyweight project demonstrates an integrated machine arrangement rather than a standalone induction heating power supply.
Main Equipment and Functions
| Componente | Configuração |
|---|---|
| Fonte de Alimentação por Indução | Selected for the material, heating area and required cycle |
| Custom Inductor | Designed for the flyweight geometry and localized heating position |
| Rotary Indexing System | Positions workholding locations during the operating sequence |
| Workpiece Fixtures | Locate and secure components for processing |
| Automatic Loading and Unloading | Handles workpieces during the production sequence |
| Hardening and Cooling Arrangement | Selected for the required material and hardening process |
| Machine Control | Coordinates heating, indexing and automatic workpiece handling |
| Protective Enclosure | Provides a defined enclosed processing area |
Power Supply and Process Coordination
Kechuang’s induction heating equipment includes fonte de alimentação controlada digitalmente opções.
The required power and operating frequency are selected according to the flyweight material, dimensões do componente, inductor design and specified hardening area.
For an automated indexing machine, heating settings must be coordinated with workpiece positioning and the machine’s operating sequence.
The control arrangement is developed around the required production cycle, including the timing of loading, indexação, heating and unloading.
Fixtures and Production Requirements
A rotary indexing system is especially relevant when multiple components need to be processed in a repeated production sequence.
No entanto, the appropriate number of workholding positions and the handling arrangement depend on the actual component and production requirements.
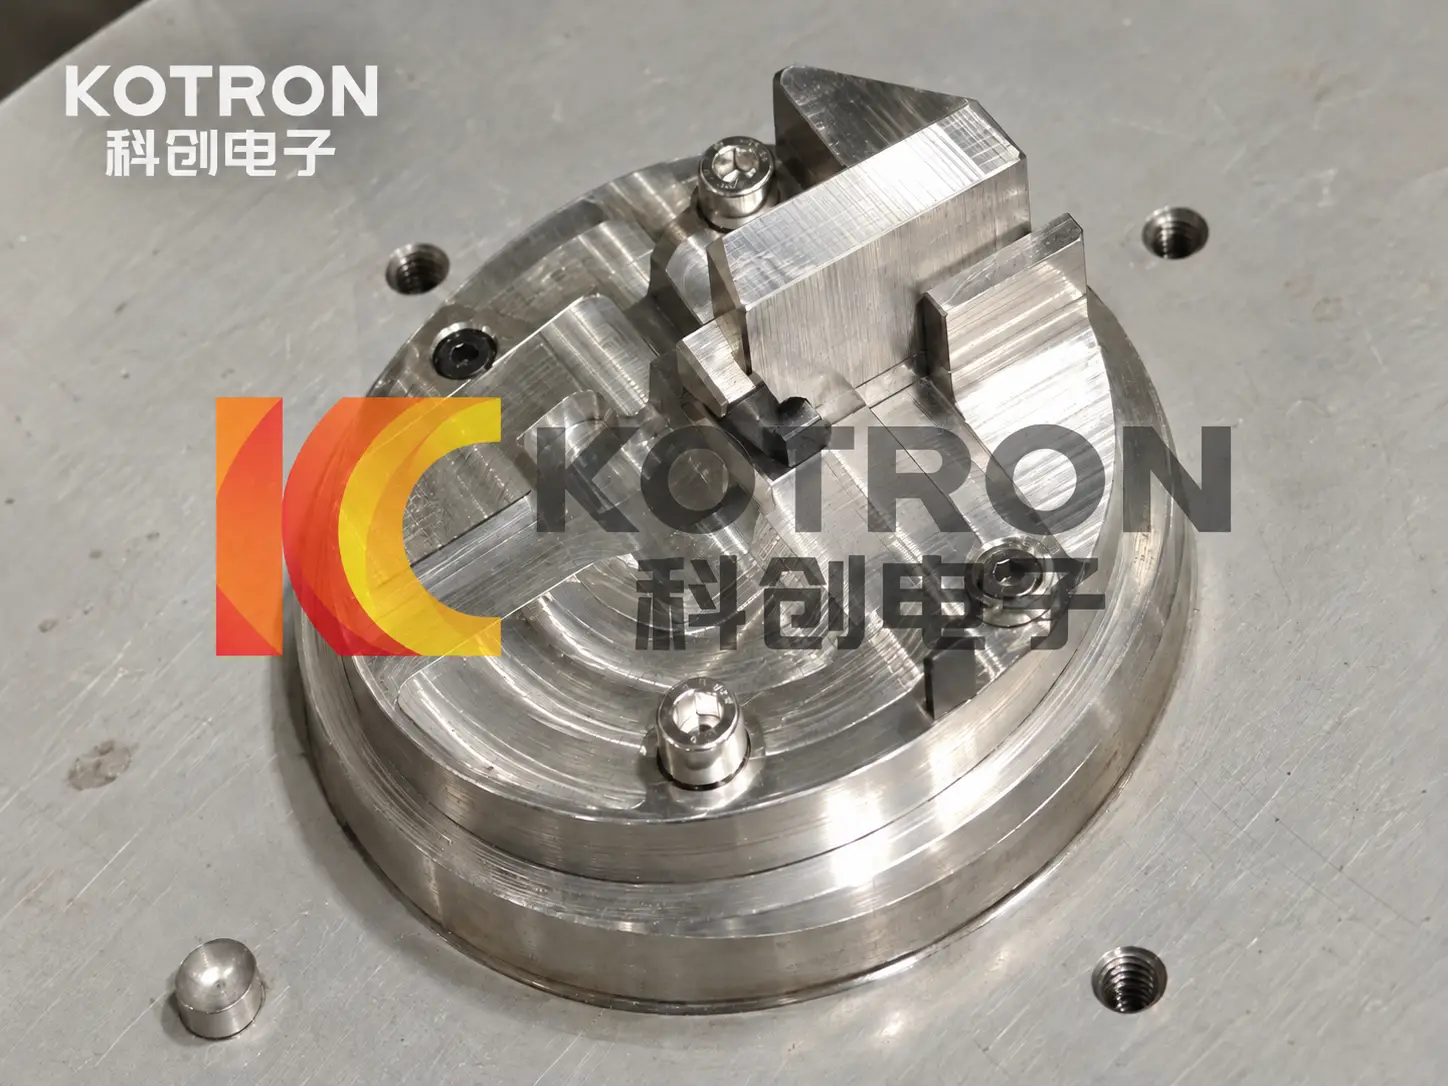
Changes in flyweight geometry may require different locating fixtures, inductor designs or positioning arrangements.
Ⅴ. Request a Customized Flyweight Induction Hardening Solution
Kechuang provides customized induction hardening systems for flyweight components and other small mechanical parts used in marine diesel engines and industrial machinery.
Para uma avaliação técnica inicial, por favor forneça:
•Workpiece drawings or photographs
•Material ou classe de aço
•Main component dimensions
•Área de endurecimento necessária
•Production quantity or target cycle time
Se disponível, please also include the target surface hardness, effective case depth and any existing inspection requirements.
Based on your workpiece and production needs, podemos avaliar a fonte de alimentação de indução, indutor personalizado, rotary indexing fixtures, quenching arrangement and automatic loading and unloading system.