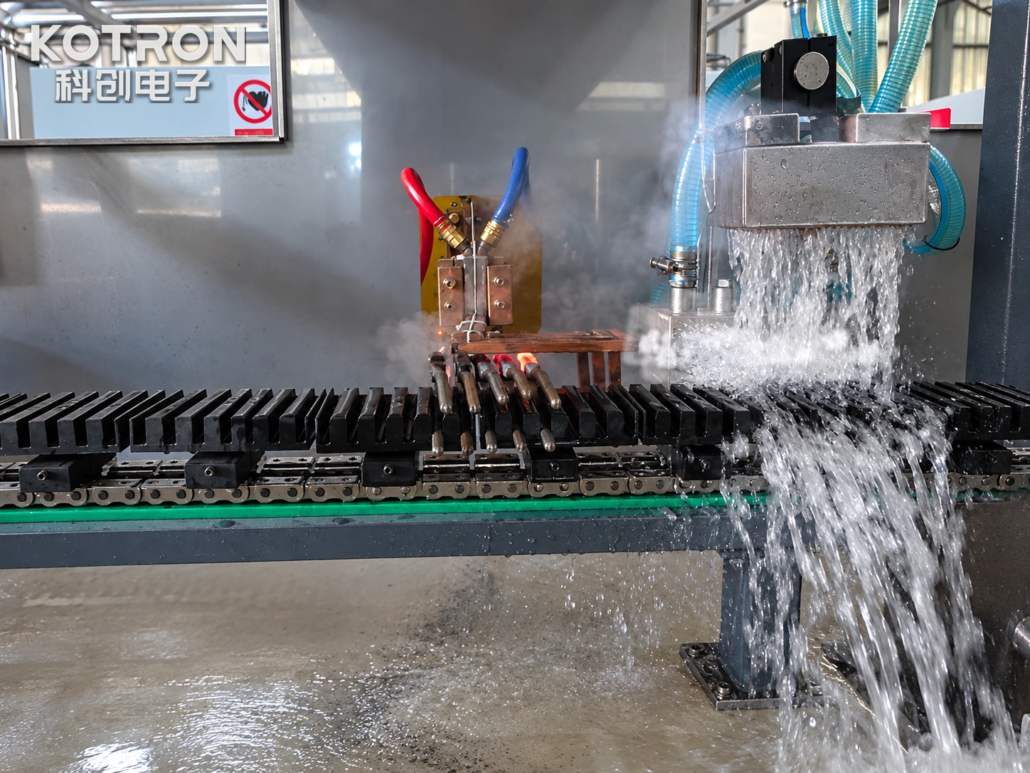
Автоматическая индукционная закалочная машина для губок плоскогубцев
Ⅰ. Automatic Pliers Jaw Induction Hardening in Operation
Видео: Continuous induction heating and spray quenching of pliers jaws, followed by mesh-belt conveyor discharge.
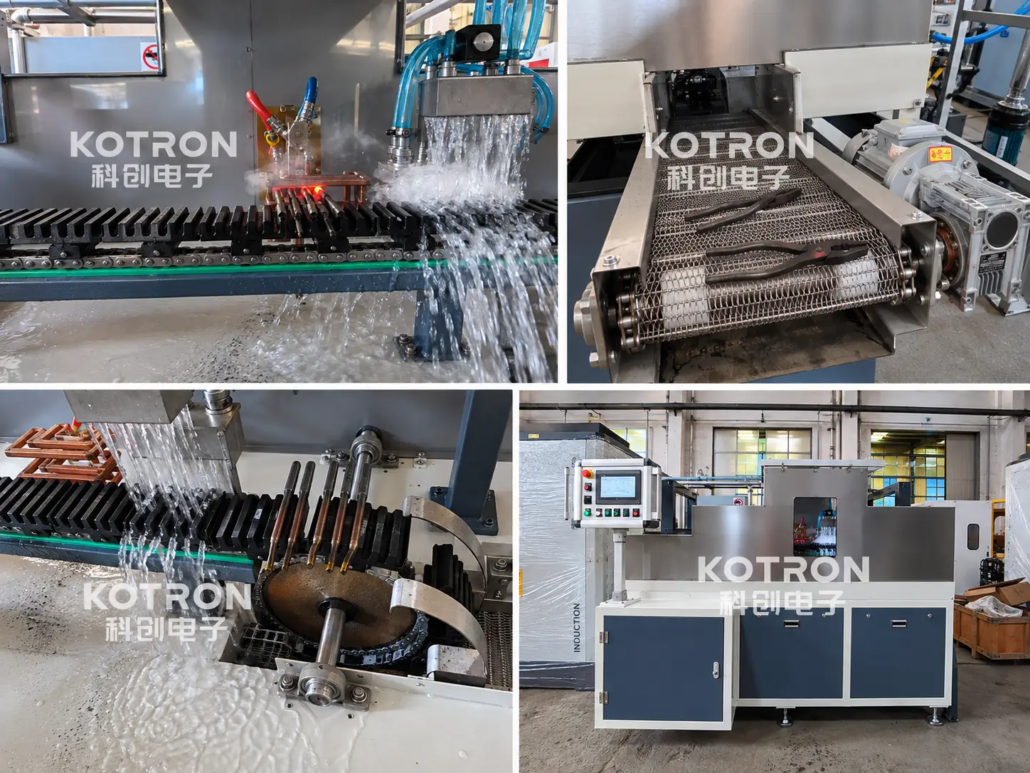
The operating footage shows multiple pliers carried through an enclosed processing area by a guided transport mechanism.
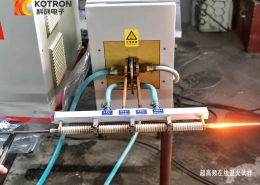
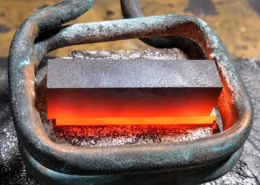
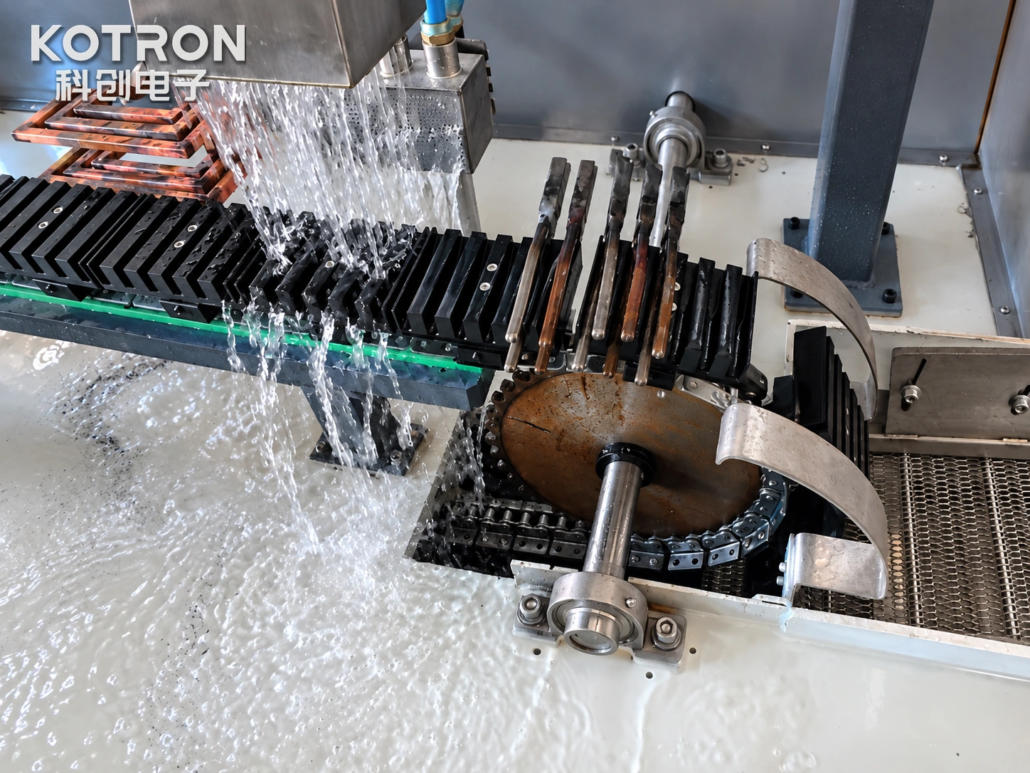
At the heating station, the front working portions of the pliers pass through the induction heating area. A localized red-hot region is visible near the jaws, while the handles remain outside the primary heating zone.
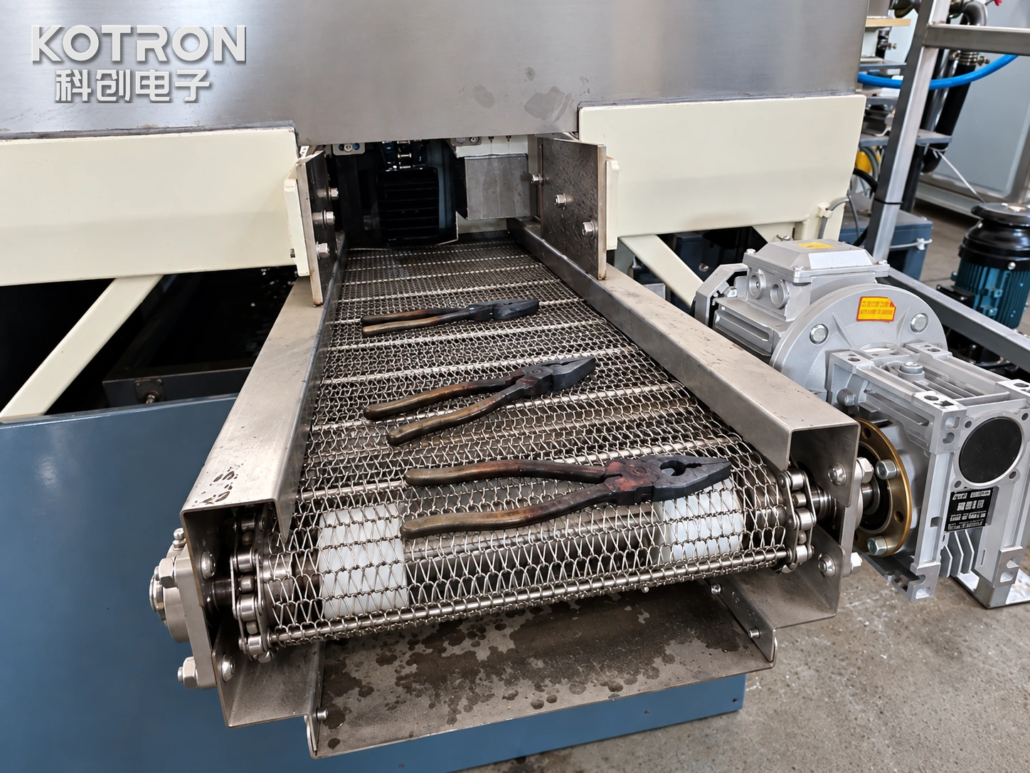
The workpieces then pass through an adjacent spray quenching section, where cooling liquid is applied to the heated region. Another view shows pliers being discharged on a metal mesh-belt conveyor.
This arrangement integrates localized heating, quenching and workpiece transport within one processing line.
Обзор оборудования
| Элемент | Описание |
|---|---|
| Оборудование | Pliers Induction Hardening Machine |
| Заготовка | Pliers and compatible jaw-type tools |
| Hardening Area | Selected front working area of the jaws |
| Процесс | Localized induction heating and spray quenching |
| Перемещение заготовки | Guided continuous transport |
| Heating Station | Induction heating assembly |
| Quenching Arrangement | Spray cooling section |
| Увольнять | Metal mesh-belt conveyor |
| Применение | Pliers and hand tool manufacturing |
Ⅱ. Localized Induction Hardening of Pliers Jaws
The working surfaces of pliers are subject to gripping pressure, contact and, for certain tool designs, cutting loads. Their hardening requirements depend on the function of the jaws and the material used.
This equipment focuses индукционный нагрев on the specified front working area. The process does not require the handles to be intentionally heated to the same hardening temperature.
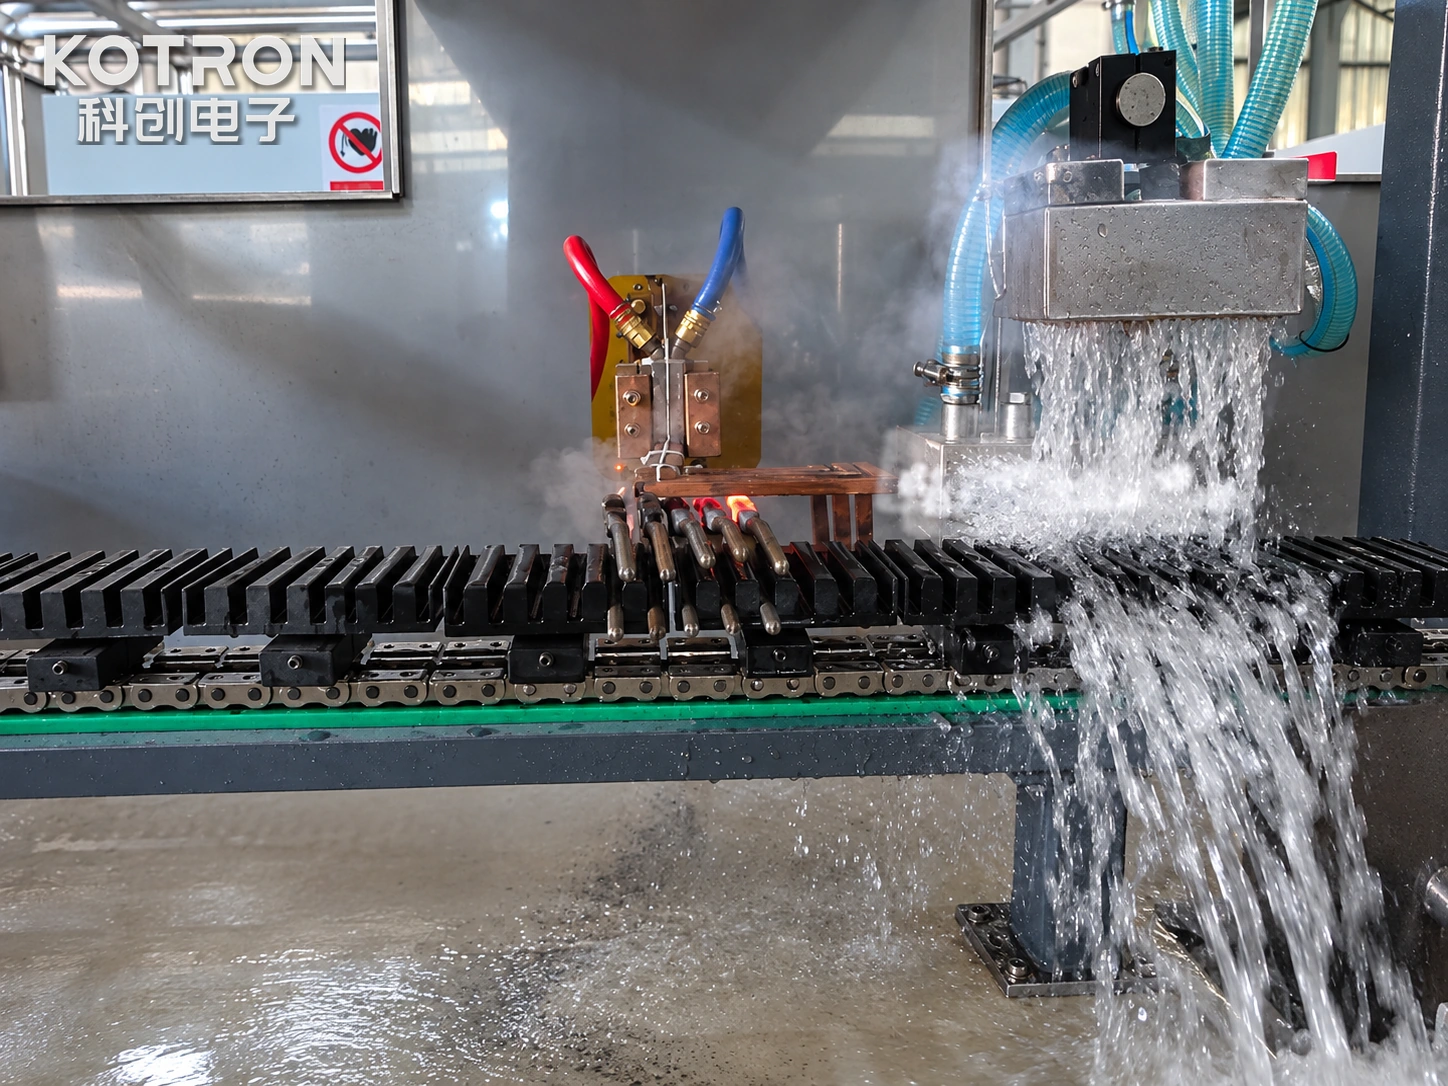
Localized heating area and inductor position for pliers jaws.
Inductor Design for Jaw Geometry
The induction heating assembly must deliver heat to the intended region while allowing the workpieces to pass through the processing station.
Jaw width, thickness, profile and orientation influence the required inductor shape and its position relative to the workpiece. The available clearance around the transport mechanism must also be considered.
For pliers with different jaw geometries, the inductor and workpiece positioning arrangement may need adjustment or replacement. Compatibility is determined by the range of parts considered during machine design.
Hardening Area and Process Requirements
The heating pattern is established around the customer’s specified working surface. Depending on the pliers design, this may involve a gripping surface, serrated jaw region or cutting edge.
These features have different geometries and should not be treated as identical applications.
The required heating conditions are determined from the workpiece material, target hardening area and specified hardness or case depth, где это применимо.
The final hardened condition depends on both the induction heating cycle and the subsequent quenching process. The required settings should be established through suitable process trials and inspection.
Ⅲ. Continuous Workpiece Transport and Spray Quenching
The production line uses a guided transport mechanism to carry pliers through the treatment area.
In the demonstrated arrangement, multiple workpieces are held in sequence, with their front working regions presented toward the induction heating station.
Workpiece Positioning and Transport
The transport mechanism must maintain the required relationship between the pliers jaws and the inductor during heating.
Workpiece spacing, support geometry and travel movement are considered together when developing the machine layout.
For a new pliers design, the required positioning arrangement depends on the head shape, overall dimensions and the location of the surfaces to be treated.
Координация нагрева и закалки
The закалка распылением section is positioned after the induction heating area along the processing path.
The heating and cooling operations must be coordinated with workpiece movement so that the selected area receives the intended thermal cycle.
Relevant process factors include heating duration, movement through the stations, spray coverage and the cooling requirements of the material.
Spray arrangement and quenching conditions are established for the particular application rather than assumed to be identical for all pliers.
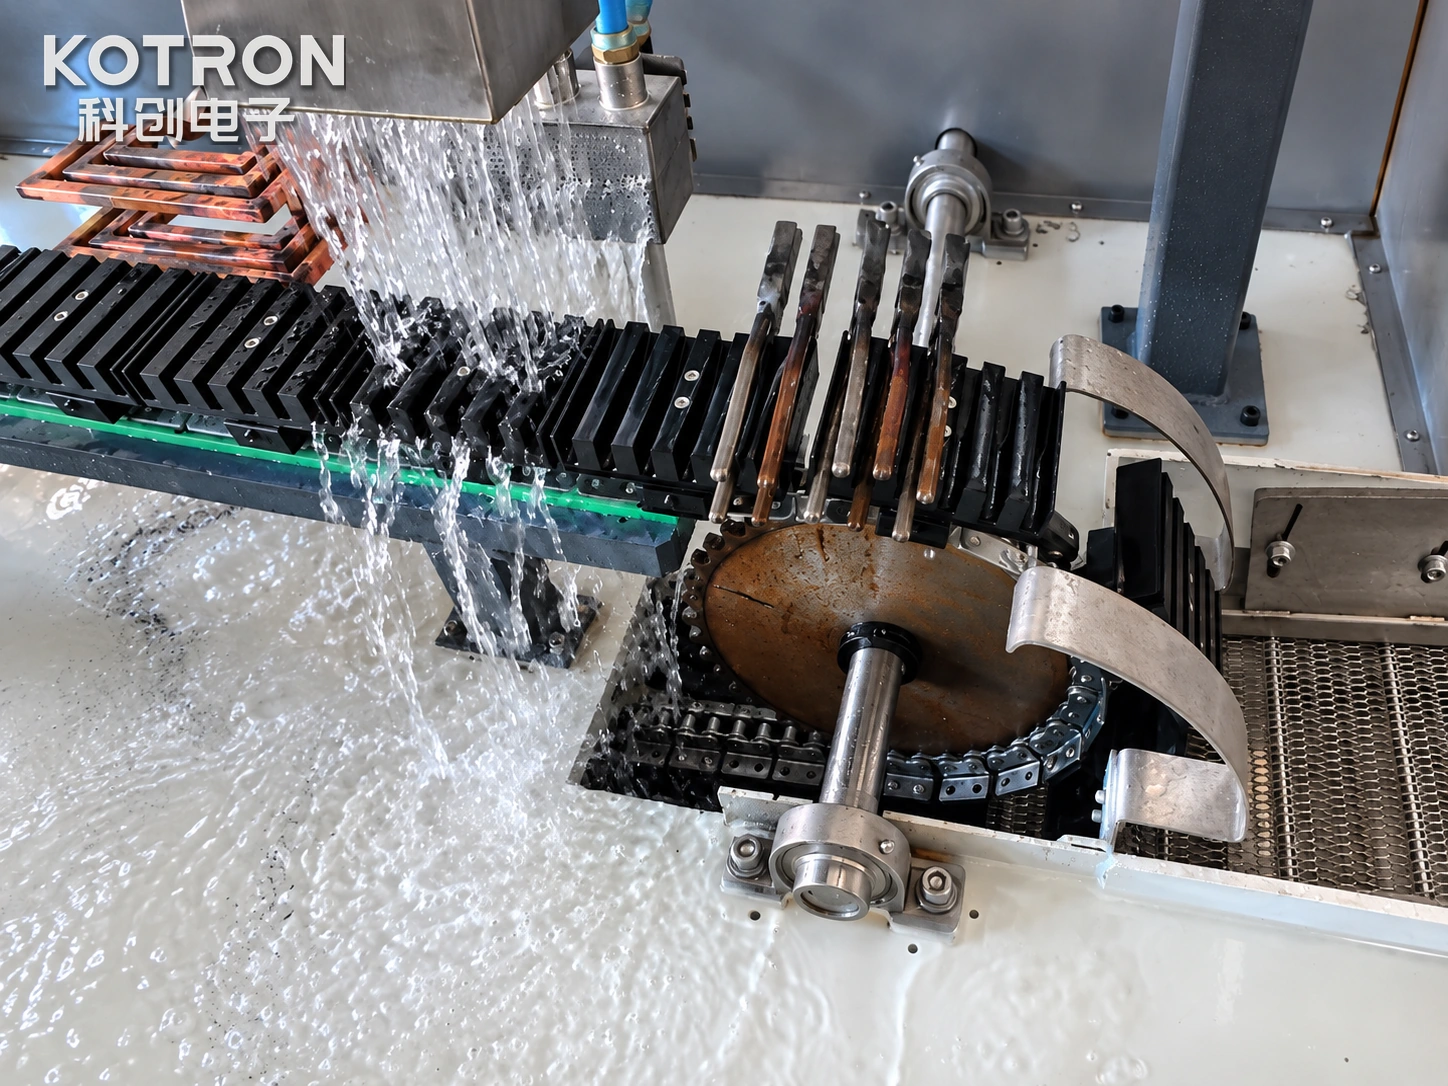
Spray quenching and workpiece transport mechanism.
Mesh-Belt Conveyor Discharge
After treatment, the pliers are transferred to a metal mesh-belt conveyor for discharge.
The conveyor provides a separate outfeed section for processed workpieces. Its layout and dimensions are selected according to the handling requirements of the production line.
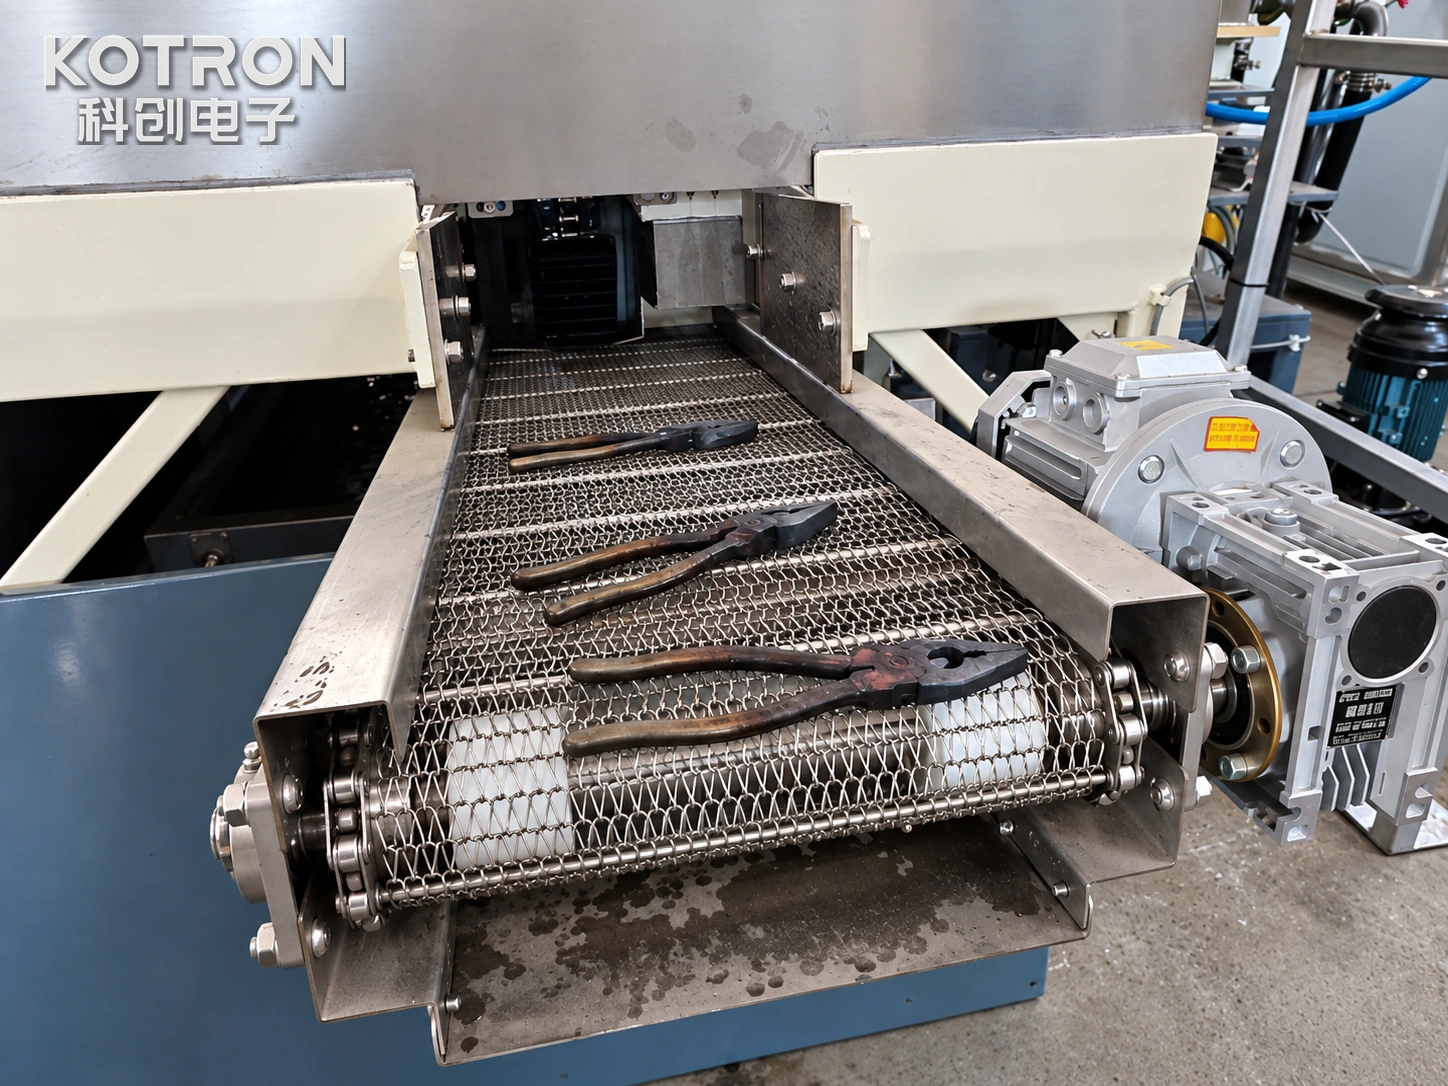
Mesh-belt conveyor with processed pliers.
Ⅳ. Machine Configuration and Customization
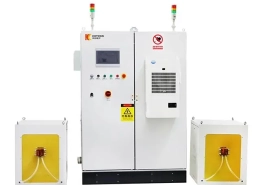
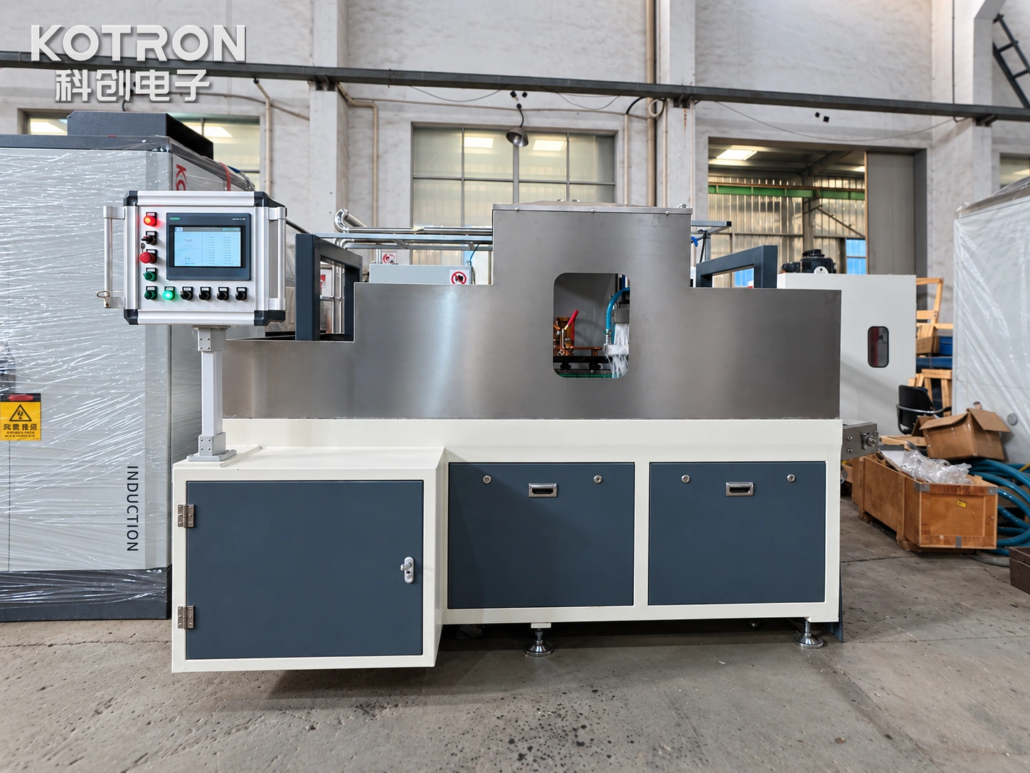
Kechuang develops pliers induction hardening equipment as an integrated system, combining the induction power supply with the heating assembly, workpiece transport and quenching arrangement.
The demonstrated machine uses continuous guided transport and spray quenching. Other project configurations are evaluated according to the workpiece and required production sequence.
Основные компоненты системы
| Компонент | Function and Configuration Considerations |
|---|---|
| Индукционный источник питания | Selected according to the heating load, Материал, inductor and process requirements |
| Custom Inductor | Designed around the target jaw area and available operating clearance |
| Workpiece Supports and Guides | Position the pliers during travel through the heating station |
| Transport Mechanism | Moves workpieces through the processing sequence |
| Spray Quenching System | Applies the specified cooling process after induction heating |
| Conveyor Discharge | Transfers treated workpieces away from the processing section |
| Machine Controls | Coordinate heating operation and workpiece movement; control functions are defined by the project |
Power Supply and Heating Configuration
Power and operating frequency are selected according to the required heating pattern, материал заготовки, dimensions and inductor design.
The индукционный источник питания alone does not determine the hardening result. Индуктор, положения заготовки, heating cycle and quenching conditions must be evaluated as a complete process.
Automation and Production Requirements
The appropriate automation arrangement depends on the intended production flow.
For a conveyor-based pliers hardening system, the transport movement and heating cycle need to operate in coordination. Additional handling functions, such as automatic loading or collection, are specified separately where required.
Production capacity, workpiece changeover and the range of compatible pliers should be evaluated during equipment selection rather than assumed from the machine layout alone.
Ⅴ. Request a Customized Pliers Induction Hardening Machine
Kechuang provides customized induction hardening machines and production-line solutions for pliers manufacturers requiring localized treatment of jaw working surfaces.
Для первоначальной оценки оборудования, пожалуйста, предоставьте:
— Чертежи или фотографии деталей
— Материал или марка стали
— Main dimensions and jaw geometry
— Required heating and hardening area
— Expected production quantity or cycle requirement
Если уже указано, целевой твердостью, effective case depth and inspection requirements can also be included.
Our engineering team can review the workpiece and propose an appropriate induction heating arrangement, transport mechanism, spray quenching configuration and equipment layout.
Request a Customized Pliers Induction Hardening Machine
Часто задаваемые вопросы
Нажмите на вопрос, чтобы развернуть ответ.
Which pliers designs can this machine harden?
The system is developed for pliers and compatible jaw-type hand tools, including gripping surfaces, serrated jaw regions and cutting edges. Compatibility depends on the jaw geometry, overall dimensions and the location of the surfaces to be treated.
Are the handles hardened too?
Нет. The equipment concentrates heating on the specified front working area of the jaws. The handles remain outside the primary heating zone and do not need to reach the same hardening temperature.
Can the machine run different pliers sizes?
For different jaw geometries, the inductor and workpiece positioning arrangement may need adjustment or replacement. The range of compatible parts is established during machine design.
How is the hardening result determined?
The final hardened condition depends on both the induction heating cycle and the subsequent quenching process. Required settings are established through process trials and inspection, including target hardness and case depth where applicable.
What do you need to prepare a quote?
Чертежи или фотографии деталей, material or steel grade, main dimensions and jaw geometry, the required heating and hardening area, and the expected production quantity or cycle requirement. Target hardness and case depth can also be included if specified.