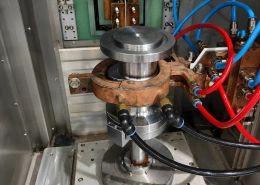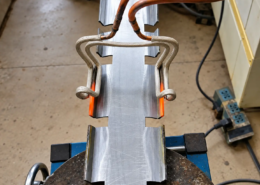
Lutowanie indukcyjne płytą miedzianą za pomocą systemu ręcznego
Ⅰ. Watch the Copper Plate Induction Brazing Process
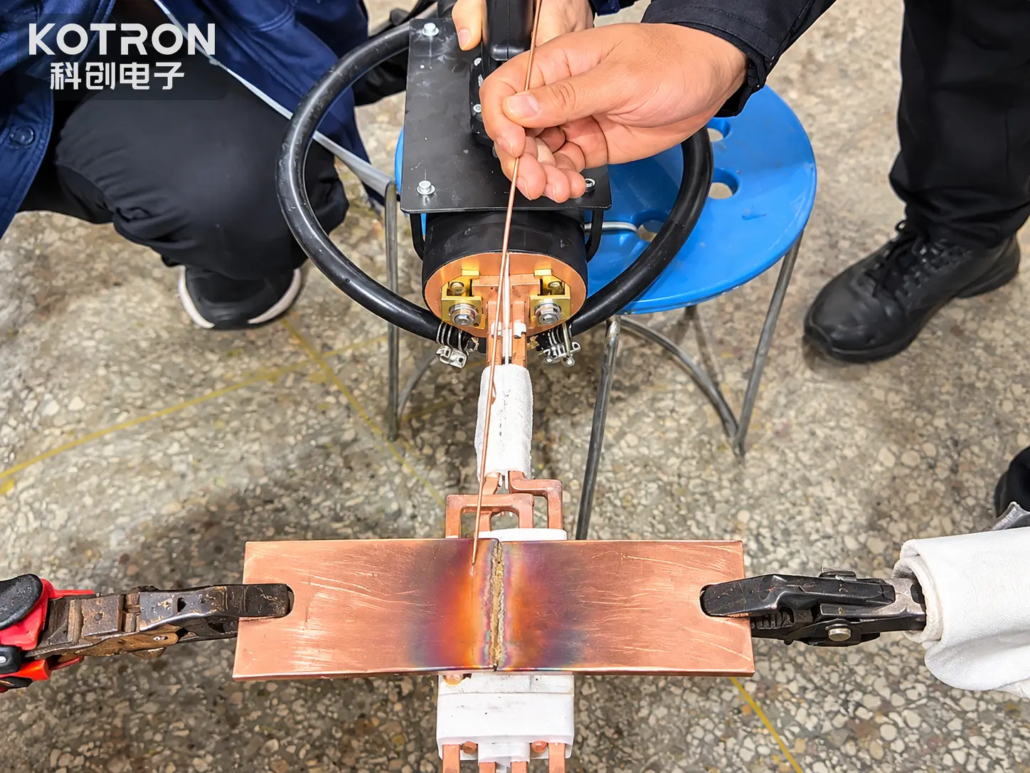
The video shows two copper plates positioned for joining, with a handheld induction workhead placed near their butt joint.
As the joint area is heated, the operator brings a thin metallic filler wire into contact with the heated region and moves it along the connection. The filler wire is progressively consumed during the brazing operation.
Several features of the process can be observed:
•Localized induction heating at the copper plate joint
•Manual positioning of the handheld induction workhead
•External clamping and support of the workpieces
•Manual application of brazing filler wire
•Visible heating concentrated around the joining area
This is a manually operated brazing demonstration rather than an automated copper joining production line.
The video focuses on the actual heating and filler application process. It does not establish a particular production cycle, joint strength or industrial quality certification.
Ⅱ. Copper Plate Butt Joint Configuration
The workpieces in this application are flat copper plates arranged with their ends meeting at a butt joint.
Unlike a lap joint, where one component overlaps another, a butt joint connects two components along their opposing edges or ends.
For copper plate brazing, the joint arrangement needs to provide suitable contact, alignment and filler metal distribution.
Important considerations include:
Copper plate thickness and width
The cross-sectional dimensions influence the amount of heat required and how rapidly energy is conducted away from the joining area.
Joint alignment
The two copper plates should be positioned and supported so that unwanted movement does not occur during heating and filler application.
prześwit łączenia
The clearance between the mating surfaces must be compatible with the selected brazing filler alloy and joint design.
Filler metal selection
The brazing alloy must be suitable for copper and the intended operating requirements of the finished connection.
In this demonstration, external clamps are used to hold the workpieces while the joint is heated.
The specific copper grade, wymiary płyty, joint clearance and filler alloy are not identified in the available video.
Ⅲ. How Induction Brazing Joins Copper Plates
Induction brazing uses indukcja elektromagnetyczna to generate heat in electrically conductive workpieces.
When the induction workhead is energized, an alternating magnetic field produces electrical currents within the copper near the inductor. The resulting electrical losses generate heat in the metal.
As the joint approaches the required brazing temperature, the filler metal melts and wets the prepared copper surfaces.
In a properly designed brazed joint, the molten filler metal distributes through the joint clearance by wetting and capillary action. After cooling and solidification, it forms the connection between the copper components.
The key difference between brazing and fusion welding is that the copper base metal is not intentionally melted during brazing.
For the process shown in the video, the operating sequence can be described as follows:
① Workpiece positioning
The copper plates are aligned and secured at the intended joining location.
② Induction heating
The handheld workhead is positioned near the joint, concentrating the heating process on the required area.
③ Filler wire application
The operator introduces filler wire into the heated joint area as the copper reaches an appropriate brazing condition.
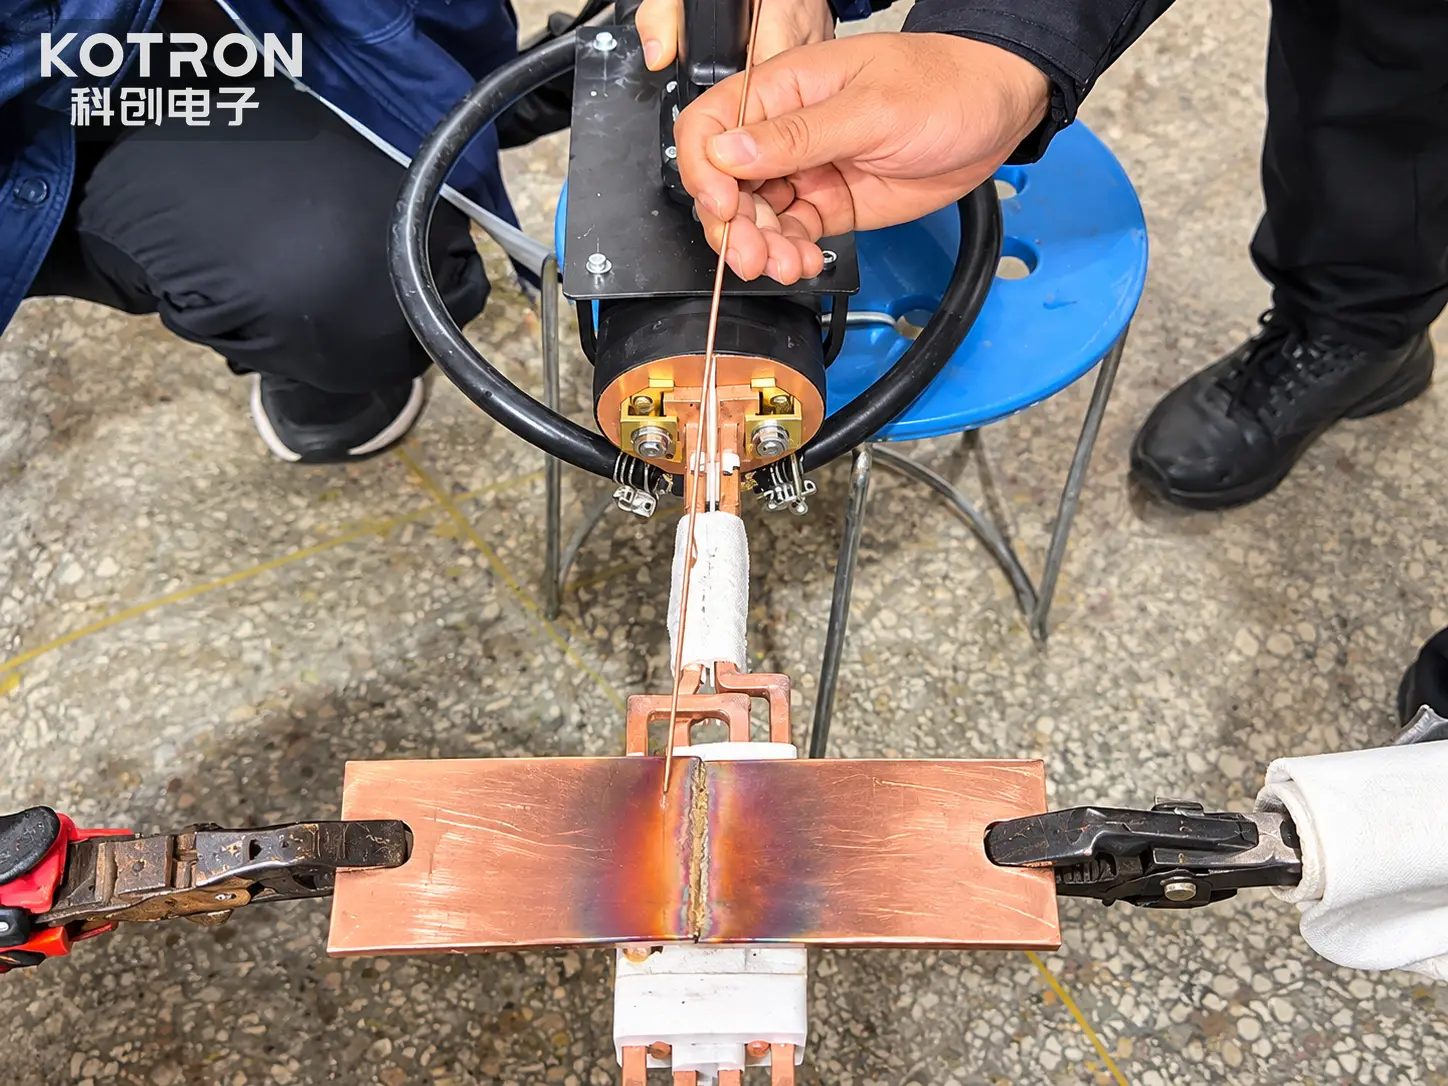
④ Joint formation
The filler metal melts and distributes over the prepared joining surfaces according to the joint geometry, temperature distribution and filler properties.
⑤ Cooling
After heating stops, the brazed connection must cool sufficiently before the joint is subjected to further handling or loading.
The actual heating temperature, time and cooling conditions should be established through process testing for each workpiece.
Ⅳ. Why Use Induction Heating for Copper Plate Brazing?
Copper is an excellent thermal conductor. During brazing, heat introduced at the joint can spread rapidly into adjacent areas of the workpiece.
This makes heat delivery, inductor positioning and filler application important parts of the joining process.
Induction heating offers several practical capabilities for copper plate brazing.
Localized energy input
The induction field can be arranged around the required joint region rather than exposing the complete workpiece to an open flame.
Adjustable heating conditions
The induction power supply allows heating power and operating time to be adjusted according to the copper dimensions and joining requirements.
Adaptable inductor design
Different inductor geometries can be developed for flat copper plates, strips and other conductive components.
Flameless heating
Heat is generated in the workpiece through electromagnetic induction, without the need for a fuel-gas flame at the joining location.
Potential for repeatable processing
Once suitable heating conditions are established, the power settings, układ induktora, fixture and operating sequence can be standardized for recurring workpieces.
These capabilities can be valuable for manufacturers evaluating alternatives to conventional flame brazing.
Jednak, induction heating does not automatically guarantee faster production, lower energy consumption or better joint quality. Such benefits depend on the actual workpiece, machine configuration and validated process.
V.. Handheld Induction Heating Equipment Used in This Application
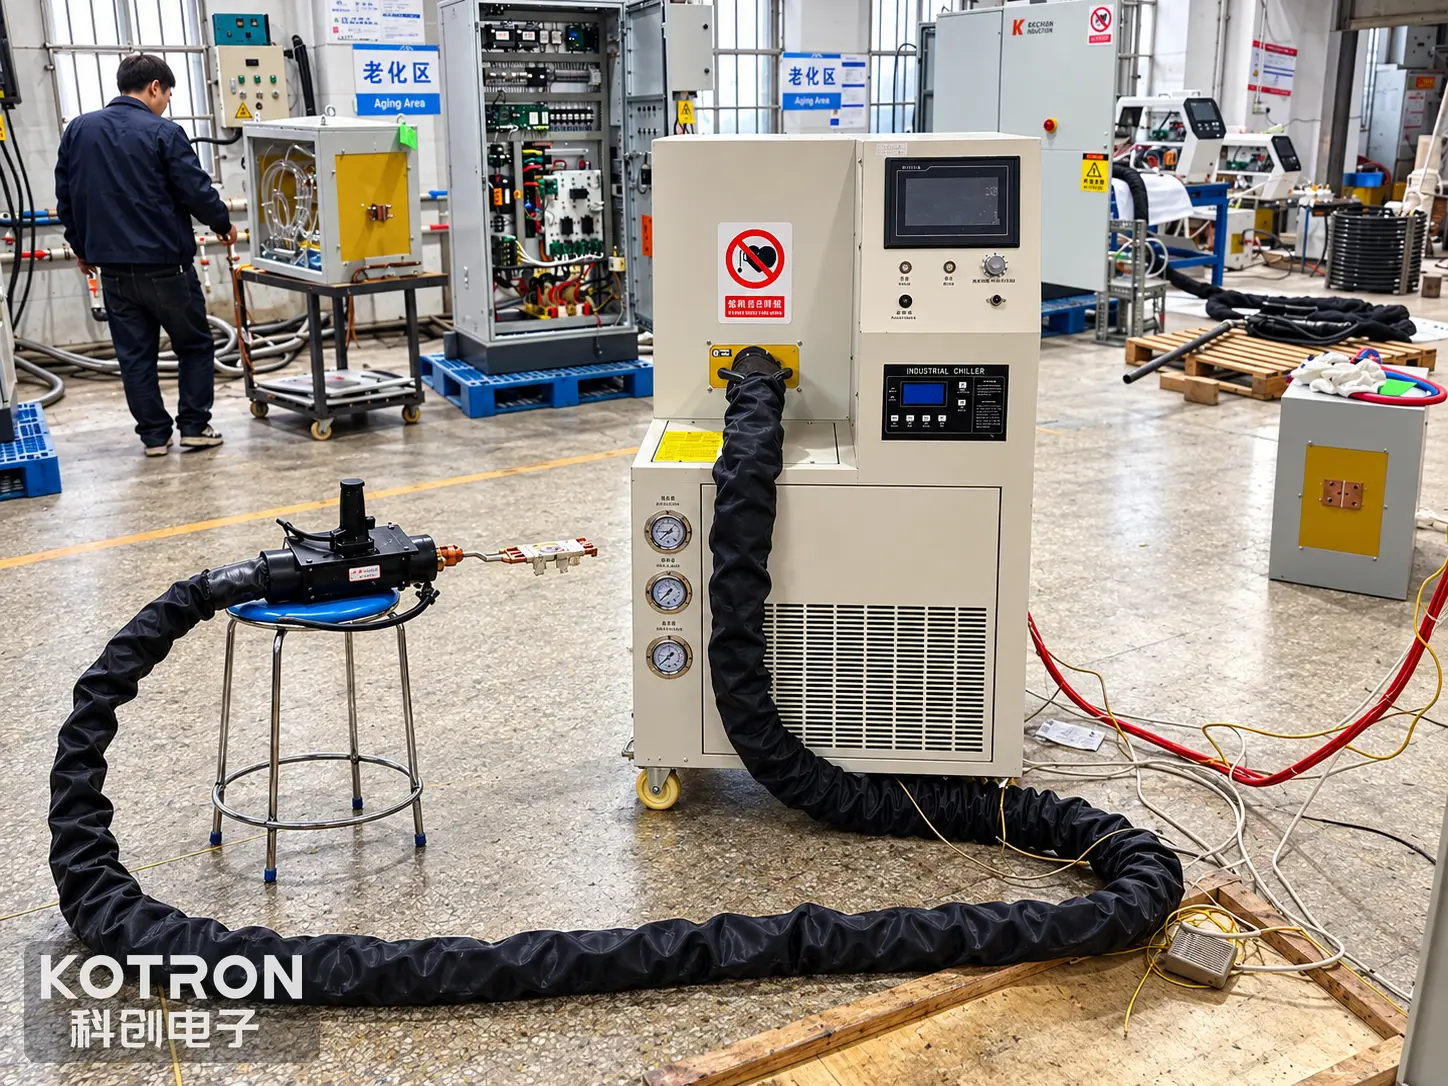
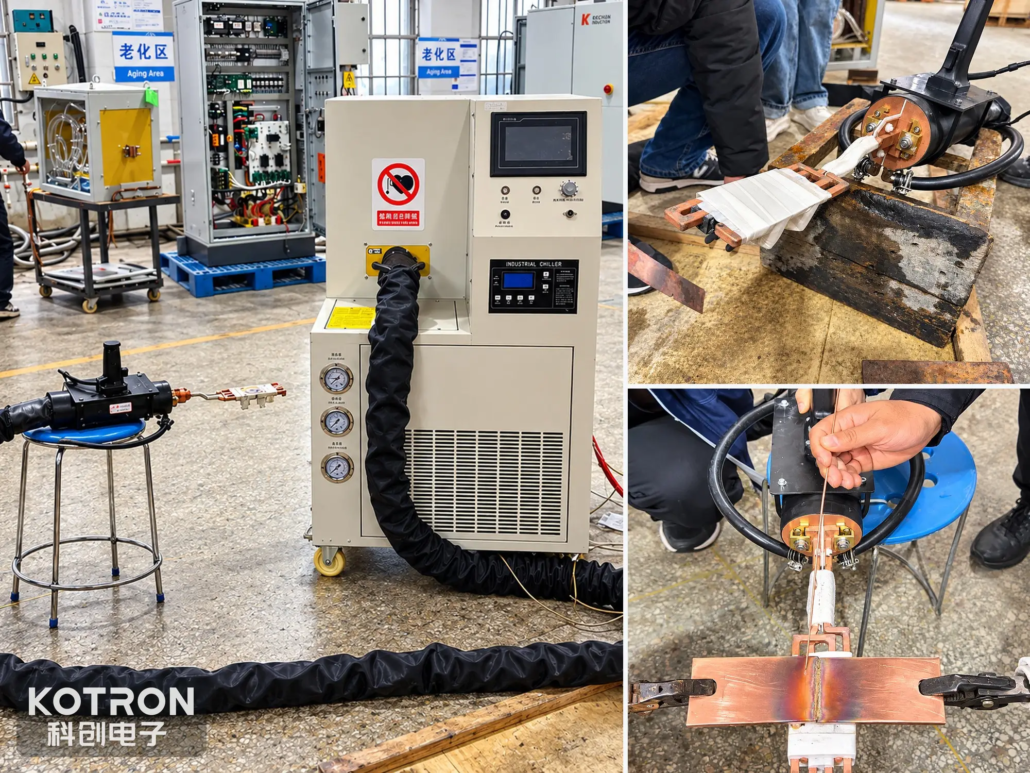
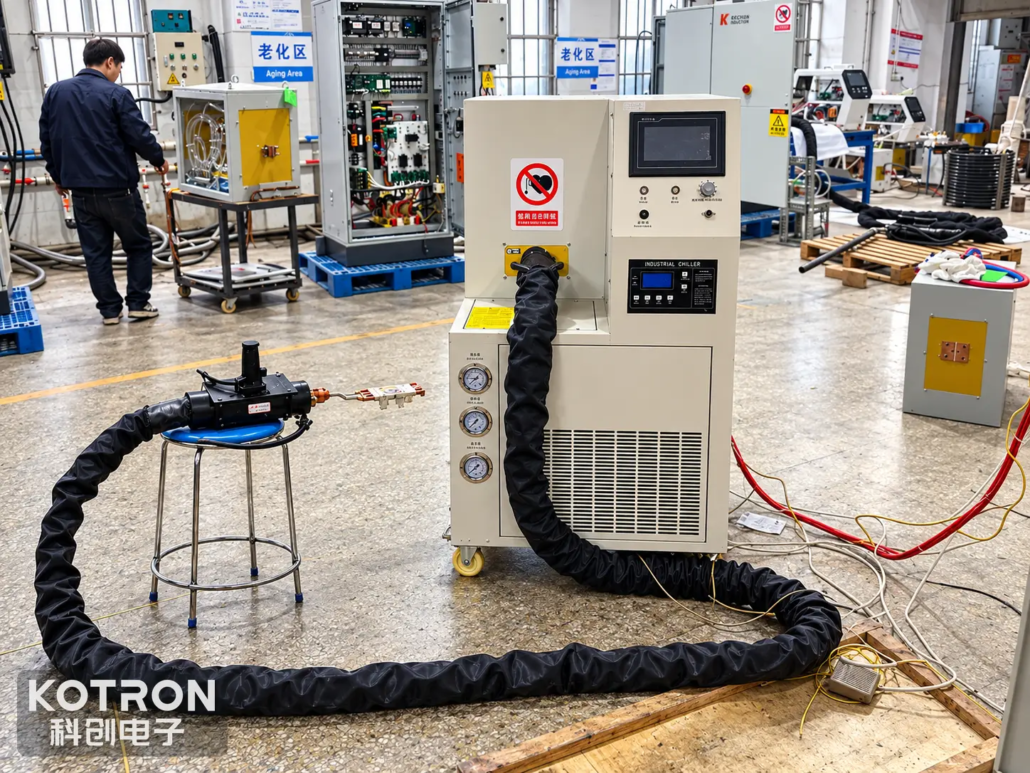
The demonstrated setup uses a handheld induction workhead connected to a larger induction heating and cooling arrangement.
The visible equipment includes:
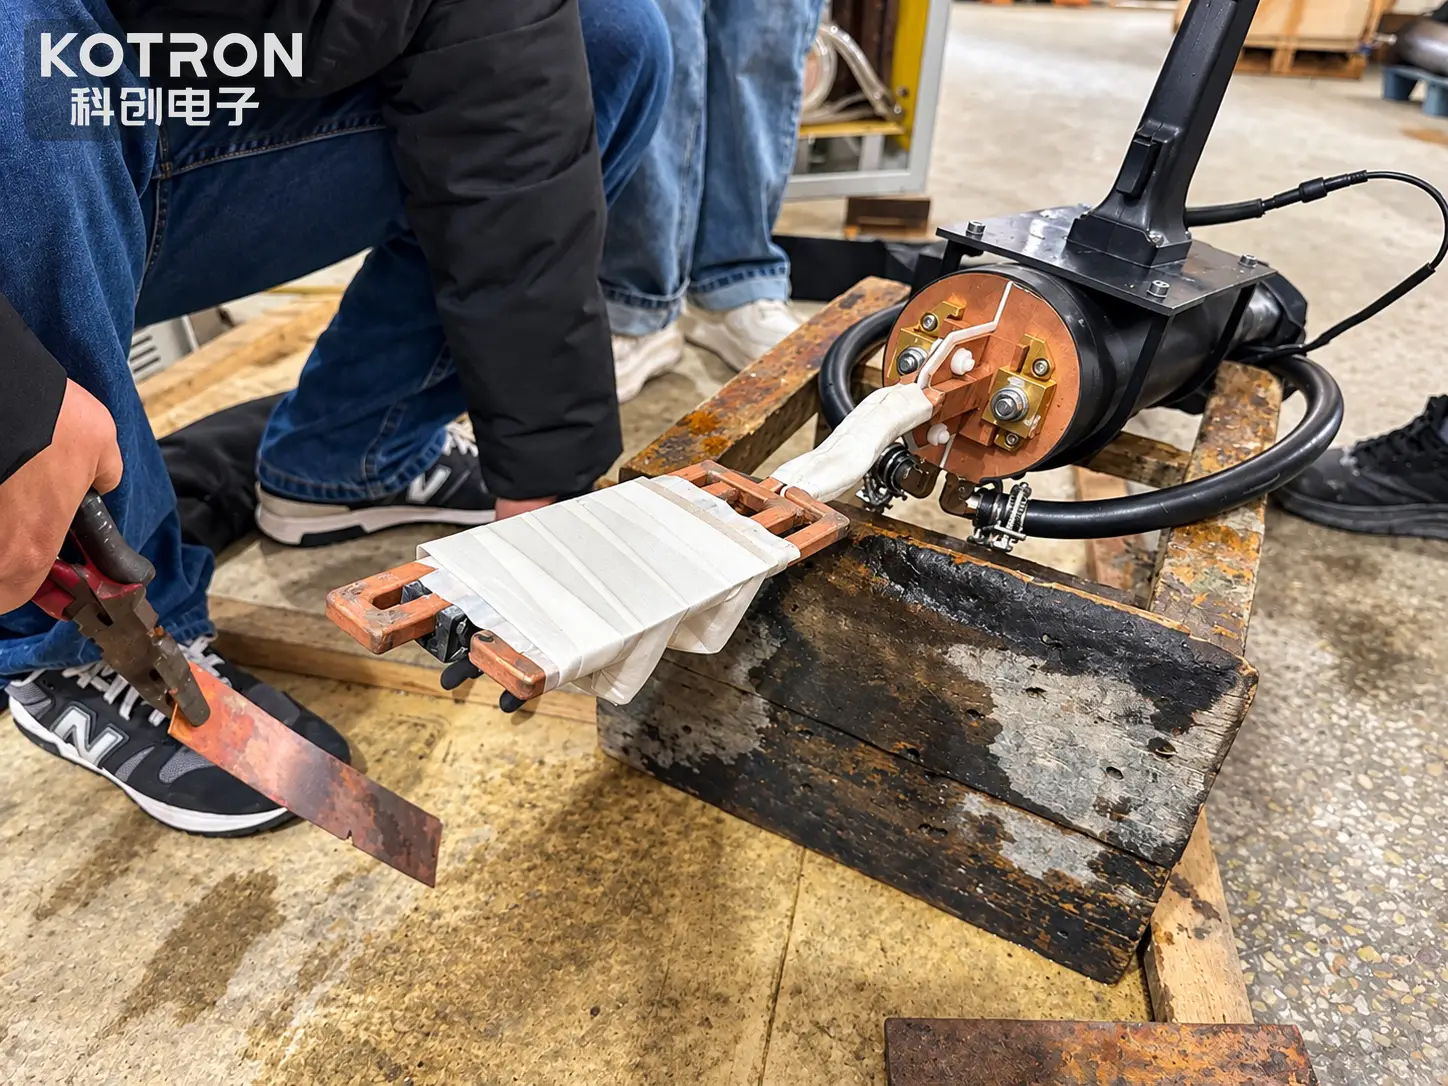
Handheld induction workhead
The operator holds the heating assembly and positions it relative to the copper plate joint.
This arrangement allows the heating location to be adjusted manually during the operation.
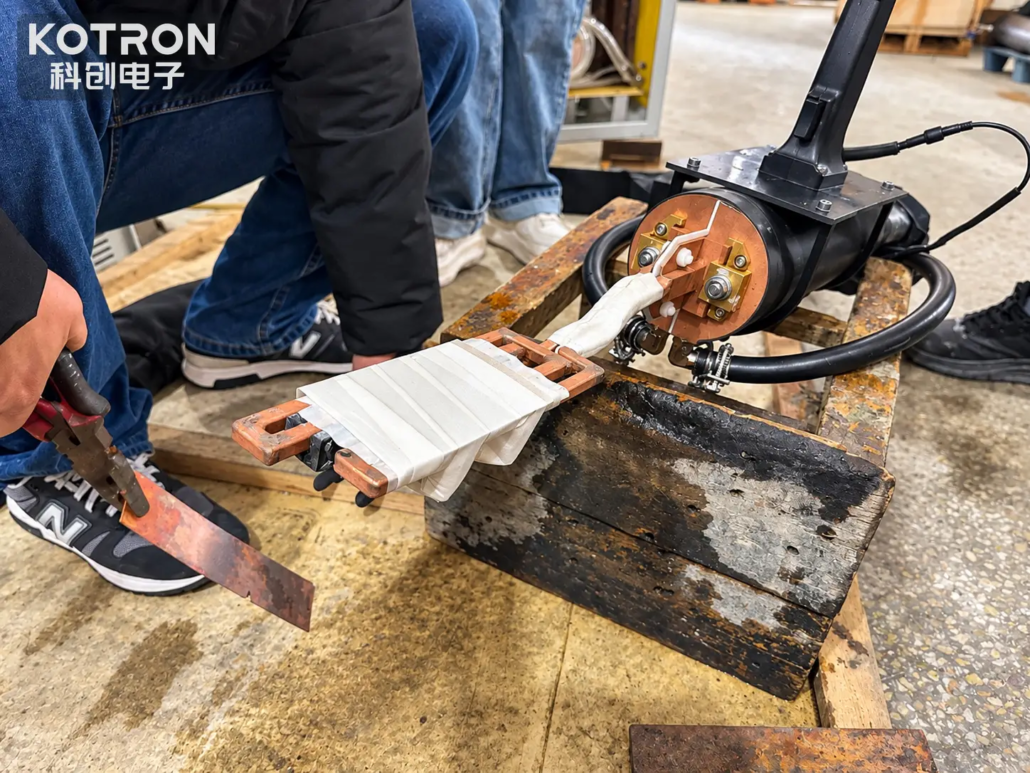
Inductor assembly
The front of the handheld workhead contains the conductive components used to deliver induction heating to the workpiece.
The inductor geometry and its distance from the copper plates affect the coupling between the heating system and the joint.
Zasilanie indukcyjne
The induction power source provides the electrical output required to energize the inductor.
The appropriate power and operating frequency should be selected according to the copper cross-section, strefę nagrzewania, inductor design and desired production cycle.
Cooling arrangement
The workshop setup includes cooling equipment and connected hoses.
Cooling requirements depend on the induction workhead, power supply and selected system configuration.
Mocowanie przedmiotu obrabianego
The copper plates are supported and clamped to maintain their position during the joining process.
For a repeatable production process, the fixture would need to provide consistent alignment while allowing suitable access for the inductor and filler wire.
The available images do not establish a confirmed power rating, zakresu częstotliwości, equipment model or cooling capacity for this particular setup.
Ⅵ. Handheld Brazing Versus Automated Copper Plate Brazing
The system demonstrated in this case uses manual workhead positioning and manual filler wire feeding.
This type of arrangement can be considered where the workpiece geometry, production volume or operating environment makes manually positioned heating practical.
For higher-volume manufacturing, additional automation may be evaluated.
W zależności od zastosowania, an automated copper plate brazing system may require:
•Fixed or automatically positioned inductors
•Dedykowane mocowania przedmiotu obrabianego
•Controlled heating sequences
•Automatic or pre-placed filler metal
•Temperature or process monitoring
•Automated loading and unloading
•Integracja z istniejącym sprzętem produkcyjnym
These are potential system configurations rather than features confirmed in the demonstrated machine.
The appropriate solution depends on production volume, part variation, available floor space, joint requirements and the desired level of operator involvement.
A handheld induction brazing setup and an automatic induction brazing line should therefore not be treated as interchangeable equipment.
Ⅶ. Important Process Factors for Brazing Copper Plate Joints
Successful copper plate brazing depends on more than reaching a visibly high temperature.
Several process variables must be considered together.
Induction power and frequency
Dla zasilanie must provide sufficient heating energy for the copper workpiece.
Operating frequency influences the distribution of induced currents and must be considered together with workpiece geometry and inductor design.
Inductor position and coupling
The distance and orientation between the inductor and copper plates affect heating distribution.
A suitable inductor should provide access to the joint while allowing the required heat to reach the brazing surfaces.
Czas ogrzewania
Insufficient heating may prevent proper filler metal flow, while excessive heating may cause unnecessary oxidation, filler degradation or unwanted effects on the workpiece.
Filler metal and flux
The filler metal must be compatible with the copper components and their service conditions.
Flux or an appropriate controlled atmosphere may be required depending on the brazing alloy, surface condition and process design.
Wspólne przygotowanie
Surface cleanliness, joint clearance and mechanical alignment affect filler wetting and the final brazed connection.
Cooling and inspection
Cooling conditions and subsequent inspection should be defined according to the joint’s intended mechanical, electrical or other service requirements.
For copper plate assemblies, these factors should be evaluated together rather than selecting the induction power supply from plate thickness alone.
Ⅷ. What This Copper Plate Brazing Demonstration Shows
This application provides a practical example of induction heating used in a copper plate joining operation.
The available video confirms the general workpiece arrangement, localized heating method and manual filler wire application.
| Application Detail | Observed Configuration |
|---|---|
| obrabiany element | Flat copper plates |
| Joint arrangement | Butt joint |
| Joining process | Lutowanie indukcyjne |
| Metoda nagrzewania | Miejscowe ogrzewanie indukcyjne |
| Heating operation | Handheld workhead |
| Filler application | Manually fed metallic filler wire |
| Workpiece holding | External clamps and support |
| Equipment arrangement | Induction heating system with cooling equipment |
| Moc i częstotliwość | Not specified |
| Copper grade and dimensions | Not specified |
| Brazing filler composition | Not specified |
| Heating temperature and cycle time | Not specified |
| Joint strength and inspection results | Not provided |
The demonstration establishes the process arrangement and shows filler application during induction heating.
For production qualification, additional information would be needed to evaluate joint strength, filler penetration, electrical performance where applicable, consistency and suitability for service.
Ⅸ. Potential Applications for Copper Plate Induction Brazing
Induction brazing can be considered for flat copper components that require a brazed connection and have geometry suitable for localized induction heating.
Potential workpiece categories include:
Flat copper plate assemblies
Copper plates that need to be joined along prepared edges or at defined connection locations.
Copper strips and flat conductors
Narrower copper components used in assemblies where the joining geometry permits suitable inductor access and brazing filler application.
Electrical copper connections
Some electrical components use brazed copper connections where electrical conductivity, contact geometry and joint reliability are important.
The exact suitability must be evaluated from the design and electrical requirements.
Custom copper fabrication
Special-shaped copper components may require customized inductors, fixtures or joining procedures.
These are potential application categories. The video itself does not identify the final industry or service application of the copper plates.
Z tego powodu, the demonstrated workpiece is described as a copper plate joint rather than automatically classified as an electrical busbar, motor conductor or transformer component.
Ⅹ. Selecting an Induction Brazing System for Copper Plates
A suitable induction brazing system should be selected according to the workpiece and joining process, not simply by choosing a standard power rating.
For an equipment or process evaluation, the following information is particularly useful.
| Informacja | Dlaczego to ma znaczenie |
|---|---|
| Copper material grade | Determines material and joining considerations |
| Plate width and thickness | Affects heating demand and inductor selection |
| Joint drawing | Defines the connection geometry |
| prześwit łączenia | Helps determine filler suitability and flow |
| Brazing filler specification | Establishes relevant brazing requirements |
| Required joint performance | Defines inspection and acceptance criteria |
| Production quantity | Helps determine manual or automated operation |
| Wymagany czas cyklu | Influences power selection and process design |
| Workpiece handling conditions | Affects fixture and workhead arrangement |
| Available cooling and electrical utilities | Affects equipment integration |
For manufacturers considering a handheld induction brazing system, the copper plate drawing and required joining area provide a useful starting point.
Na podstawie informacji o przedmiocie obrabianym, zasilacz indukcyjny, częstotliwość robocza, induktor, fixture and processing method can be evaluated as one solution.
Customers exploring the general equipment platform can also review our portable induction heating equipment, induction brazing applications i induction brazing systems.
Ⅺ. Często zadawane pytania
Can copper plates be joined by induction brazing?
Tak. Copper plates can be brazed using induction heating when the joint design, materiał wypełniający, surface preparation and heating conditions are appropriate.
The induction system supplies the heat needed for brazing, while the selected filler metal forms the connection between the copper surfaces.
Is copper plate induction brazing the same as butt welding?
Nie. A butt joint describes the arrangement of the workpieces.
W lutowaniu indukcyjnym, a filler metal melts and joins the copper plates without intentionally melting the copper base material. Fusion butt welding involves melting the base material or another joining mechanism depending on the welding process.
Can a handheld induction heater be used for copper plate brazing?
Tak. A handheld induction heating arrangement can be evaluated for suitable copper plate joints.
The required workhead, induktor, power supply and cooling configuration depend on the copper dimensions and brazing process.
Does induction brazing require filler metal?
Brazing requires a suitable filler metal to form the joint. Depending on the process, it may be supplied as wire, pręt, preform or another appropriate form.
The demonstration on this page uses manual filler wire application.
How much power is needed to braze copper plates?
There is no single power rating suitable for every copper plate joint.
The required induction power depends on the copper dimensions, obszar podgrzewania, częstotliwość robocza, inductor coupling, filler metal and target heating cycle.
A workpiece drawing and process trial can help establish an appropriate configuration.
Can copper plate induction brazing be automated?
Potentially, Tak.
Przy powtarzalnej produkcji, the heating workhead, workpiece positioning and filler application may be incorporated into a dedicated automated system.
The required configuration depends on the joint design, production rate and process-control requirements.
How can the brazed joint quality be verified?
Inspection should be selected according to the joint’s service requirements.
W zależności od zastosowania, evaluation may include visual inspection, joint section examination, mechanical testing or electrical resistance measurement.
The appropriate acceptance criteria should be established before production.
Ⅻ. Request a Copper Plate Induction Brazing Solution
Copper plate induction brazing requires coordination between the heating equipment, induktor, uchwyt dla przedmiotu obrabianego, filler metal and joint design.
The handheld system shown in this application demonstrates localized induction heating with manual filler wire application at a copper plate butt joint.
For a new copper joining project, we can evaluate an induction heating configuration based on the actual workpiece and process requirements.
Proszę podać:
Copper Plate Drawing + Materiał + Width and Thickness + Joint Type + Brazing Filler + Required Joint Performance + Production Quantity
This information helps determine the suitable heating arrangement, moc indukcyjna, częstotliwość robocza, projektowania induktorów, workpiece positioning and possible automation requirements.
Ready to Evaluate Copper Plate Induction Brazing?
Send your copper plate drawing and joint requirements — we can help determine the right heating arrangement, induction power and inductor design.