
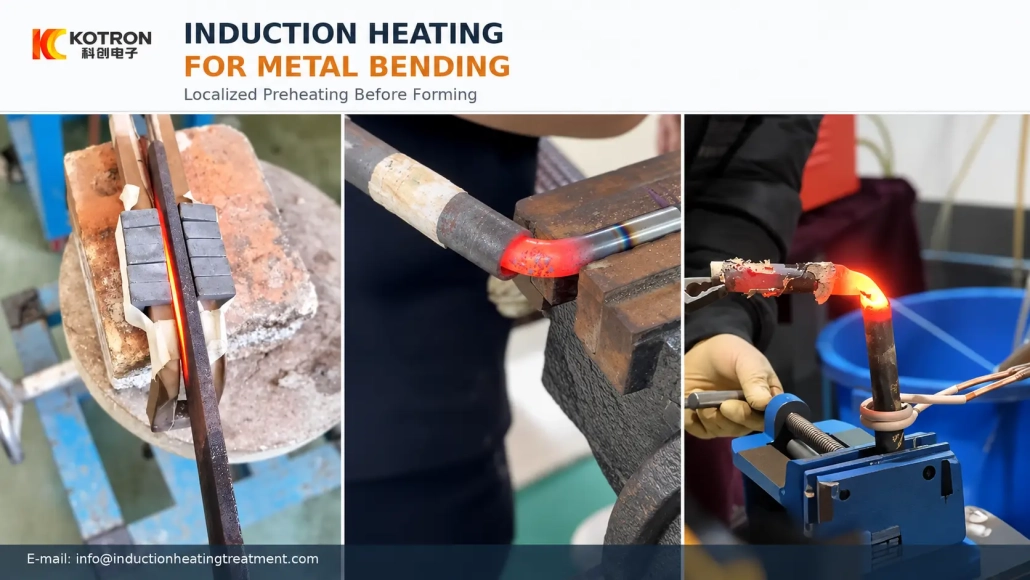
금속 굽힘을 위한 유도 가열: 국지적 예열이 사용되는 시기와 이유
How Localized Induction Heating Supports Bending Without Heating the Entire Workpiece
유도 가열 can be used to heat a selected area of a metal part before or during bending. Instead of heating the entire workpiece, the process concentrates heat around the region that will be formed.
The heating system prepares the material for bending; the actual deformation is still produced by a press, bending arm, roll or other forming equipment.
2. How Localized Induction Heating Supports the Bending Process
3. Induction Preheating and Induction Bending Are Different Equipment Problems
4. Which Parts Can Be Heated Before or During Bending?
5. Does Bending Require a High-Frequency Induction Heater?
6. The Heated Zone Must Match the Bend Line
7. Heating Helps the Process but Does Not Eliminate Bending Defects
8. Induction Heating or Flame Heating Before Bending?
9. What Information Is Needed Before Selecting a System?
1. Why Heat Metal Before Bending?
Many metal parts can be bent at room temperature. For some applications, 하지만, increasing section thickness, reducing the bend radius or changing the material condition can make cold bending more difficult.
The bending operation may require greater force, while local strain can increase the risk of cracking, springback or unacceptable distortion.
Heating the bend area changes the material’s response during forming. In suitable applications, induction preheating before bending can reduce the force needed to deform the part and provide a more workable condition around the bend.
This is particularly relevant to thick plate, heavy structural sections and other parts where cold forming becomes difficult.
암브렐, 예를 들어, has documented induction preheating of steel tower plates before bending. In that application, plates from 6 부터 32 mm thick were locally heated before the separate forming operation.
Preheating is not necessary for every bend. 재료 등급, 단면 두께, bend radius and finished-part requirements still determine whether a heated process is appropriate.
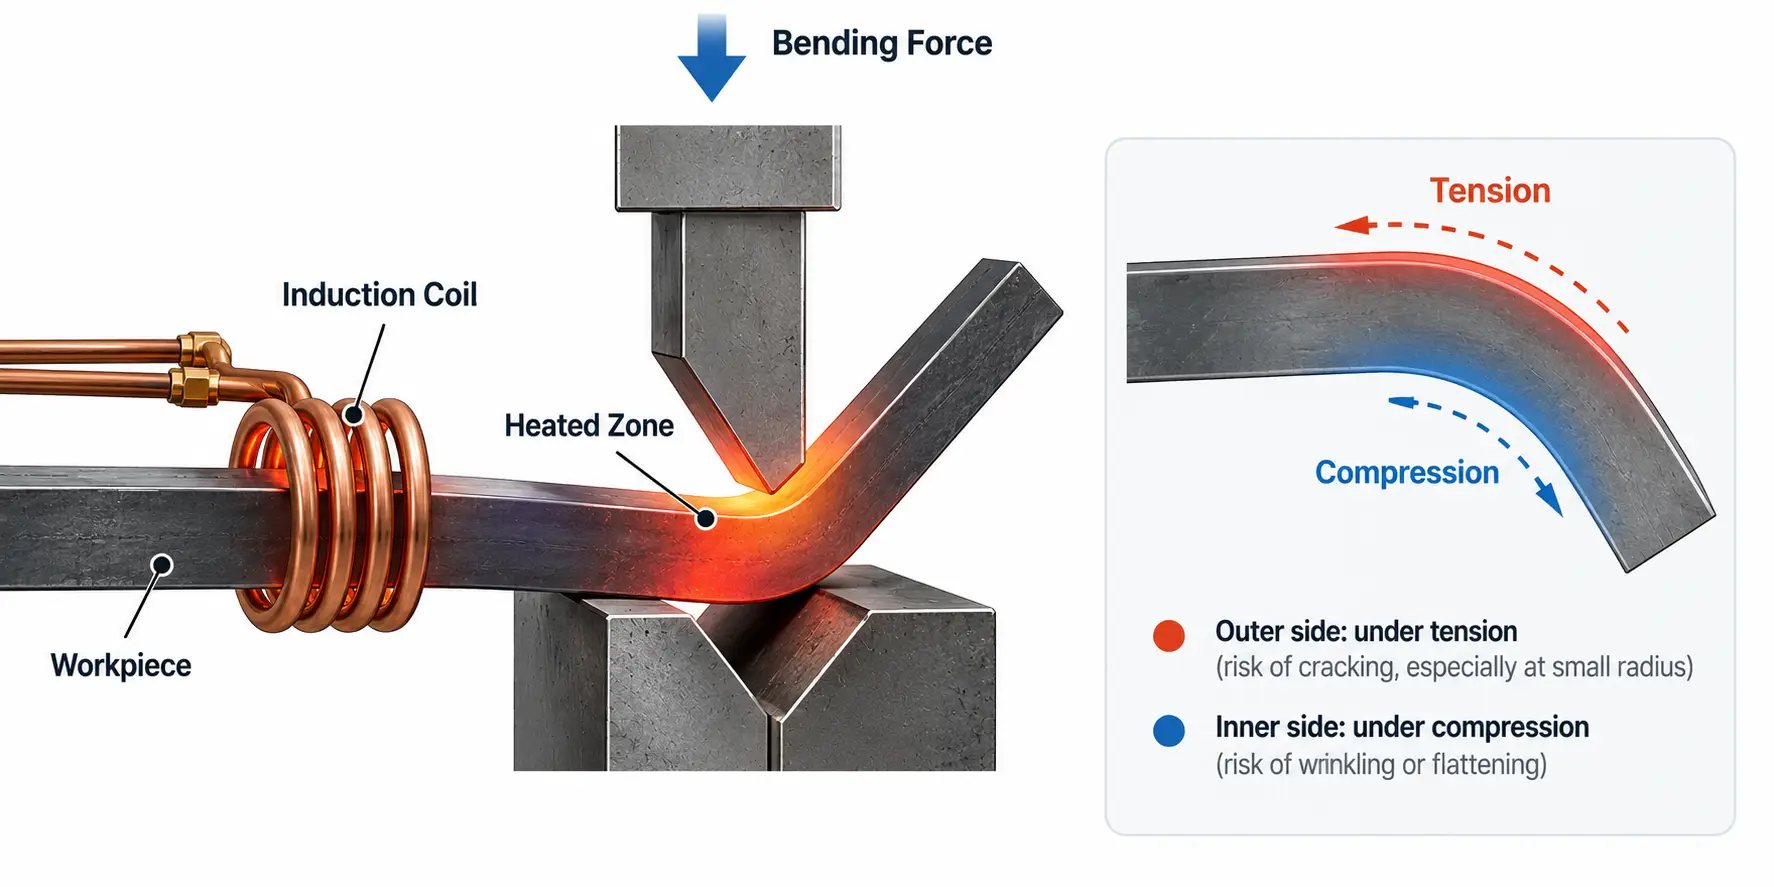
The heated bend zone, with tension on the outer surface and compression on the inner surface.
2. How Localized Induction Heating Supports the Bending Process
For bending applications, the useful feature of induction heating is its ability to establish a defined heated zone close to the area being formed.
A flat plate may require heating along a bend line. A pipe or round tube may require a heated band around its circumference. A square or rectangular section presents a different heating problem because its faces and corners do not have the same relationship to the induction coil.
In continuous induction bending, the heated region is commonly described as a heat band 또는 heated band.
Steel Tube Institute describes induction bending of hollow structural sections as heating only a short length of the section with an electric coil before that heated region passes through the bending process.
The objective is therefore not simply to heat the workpiece as quickly as possible. The location, width and depth of the heated zone need to match the bend and the forming method.
3. Induction Preheating and Induction Bending Are Different Equipment Problems
This distinction matters when selecting equipment.
와 함께 induction preheating before bending, the induction system is primarily the heat source. A manufacturer may already have a suitable press, roll bender or other forming machine and only need controlled local heating before the part enters the bending operation.
The process may look like:
Induction preheating → Existing bending equipment → Finished bend
완전한 induction bending machine is different. 난방, workpiece movement and mechanical bending are coordinated as part of one system.
DHF, 예를 들어, uses the term induction bending machine for equipment designed to bend pipe, I-beams, angles, channels, square pipe and rectangular pipe while controlling heating and cooling of a narrow section.
For pipeline applications, induction bend is also an established manufacturing term. ASME B16.49 covers factory-made steel pipeline bends produced by the induction bending process.
A customer who needs local heating for an existing press therefore does not necessarily need a complete induction bending machine.
This should be clarified before power, frequency or machine layout is selected.
4. Which Parts Can Be Heated Before or During Bending?
Induction heating can be considered for different bending applications when the required forming region can be heated in a controlled way.
Typical workpieces can include:
•Steel plate
•Pipe and tube
•Bars and rods
•Square hollow sections
•Rectangular hollow sections
•Channels
•Beams and other structural profiles
•Other fabricated metal parts requiring local heating before forming
Pipe and hollow structural sections are well-established induction-bending applications. Steel Tube Institute discusses induction bending alongside other bending methods for HSS, while dedicated machine manufacturers also apply the process to shaped structural sections.
The equipment cannot be selected from the part name alone. A thick steel plate, a round pipe and a rectangular structural section may all need hot bending, but their required heating depth, coil geometry and workpiece handling can be very different.
5. Does Bending Require a High-Frequency Induction Heater?
반드시 그런 것은 아닙니다.
High-frequency induction bending is a legitimate industry term, but the word 굽힘 does not by itself determine the correct operating frequency.
주파수 선택 is related to the required heating depth, workpiece geometry, 재료, section thickness and coil arrangement.
A useful example is Ambrell’s steel-plate bending application. The documented test used a 5–15 kHz induction system operating at approximately 13 kHz for steel plates between 6 그리고 32 mm 두께여야 합니다.
That application should not be treated as a universal frequency recommendation. It simply shows why specifying “고주파” before evaluating the workpiece can be misleading.
For a bending project, the better sequence is to define the heated section first and then select a suitable power and frequency range.
6. The Heated Zone Must Match the Bend Line
코일 설계 becomes especially important because different workpiece shapes require different heating patterns.
a steel plate, the process may need to establish a heated strip along the intended bend line.
a round pipe, the heated band may need to extend around the circumference so that the bending section reaches the required thermal condition.
왜냐하면 square or rectangular sections, the relationship between the coil, flat faces and corners becomes more complex. Corners may respond differently from broad faces, so the inductor cannot simply be treated as a larger version of a round-pipe coil.
The required heated zone also has to follow the bending process. A stationary part heated before pressing requires a different arrangement from a section that moves continuously through the coil while bending takes place.
This is why a universal coil is rarely the starting point for an industrial bending project. The inductor should be developed around the actual cross-section, bend location and required movement.
7. Heating Helps the Process but Does Not Eliminate Bending Defects
Induction heating can change the thermal condition of the material, but it does not remove the mechanical effects of bending.
Depending on the part and process, problems can still include:
•균열
•Excessive springback
•Dimensional distortion
•Local flattening
•Surface damage
For tube and pipe, additional concerns may include wall thinning on the outside of the bend, wall thickening or wrinkling on the inside, and loss of roundness.
Heating conditions are only one part of the process. Bend radius, 물질적 상태, 공구, mechanical support and forming sequence still affect the final result.
This is also why increasing heating power should not be used as the automatic response to a bending defect. The cause may lie in the forming setup rather than the heat source.
The finished part, rather than the heater alone, should be used to judge whether the process is suitable.
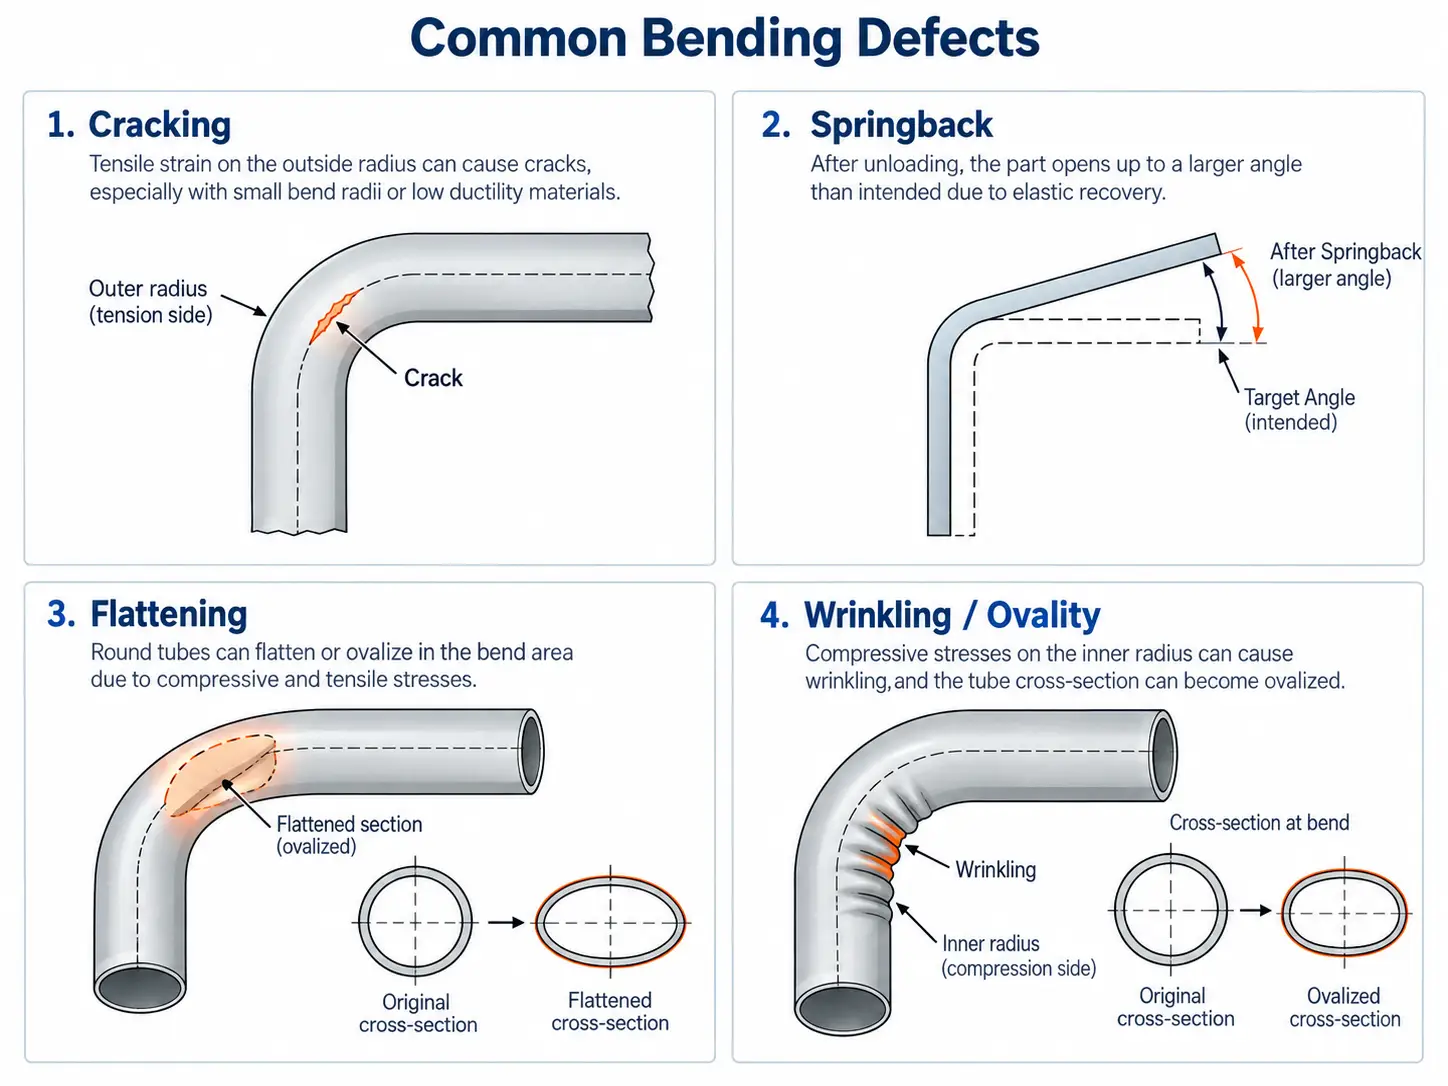
Common defects that can still occur during metal bending, even with localized preheating.
8. Induction Heating or Flame Heating Before Bending?
Flame heating is also used for localized hot bending and remains practical in some fabrication work.
For occasional parts, field work or very large and irregular components, a torch may provide useful flexibility without requiring dedicated induction tooling.
Induction heating becomes more attractive when the process is repeated and the manufacturer needs greater control over where and how the part is heated.
Relevant considerations include:
•How precisely the heated area needs to be positioned
•Whether similar parts are produced repeatedly
•Whether heating time needs to follow a programmed cycle
•Whether the heating station must be integrated with a press or bending machine
•How much the process should depend on operator technique
•Whether temperature or production data need to be monitored
The comparison should therefore be based on the production problem rather than on the heat source alone.
For a one-off fabrication job, induction heating may add unnecessary complexity. For repeated production requiring a defined heating zone and coordinated machine operation, it can be easier to integrate into the process.
9. What Information Is Needed Before Selecting a System?
A useful equipment proposal starts with the bend and the existing production method.
The most relevant information includes:
•Workpiece material and grade
•Part drawing or cross-section
•Plate thickness or tube wall thickness
•Overall workpiece dimensions
•Bend position
•Bend angle
•Bend radius
•Width or length of the area to be heated
•Required forming temperature, if already specified
•Existing press, roll bender or other bending equipment
•Whether heating takes place before bending or during continuous bending
•Whether the workpiece is stationary or moving during heating
•Required production cycle
•Manual or automatic part handling
•Finished-part dimensional or mechanical requirements
One question should be answered early:
Do you need an induction heating system for an existing bending machine, or a complete induction bending system?
Those are different equipment projects.
For an existing press or forming line, the solution may consist mainly of the 유도 전원 공급 장치, matching transformer, custom inductor, temperature monitoring and the required workpiece positioning arrangement.
If heating and bending must occur continuously as one coordinated process, the mechanical feed and bending system also become part of the machine design.
The equipment can then be evaluated in the following order:
Workpiece and bend requirement → 가열 구역 → Heating process → 인덕터 → 전력과 주파수 → Integration with bending equipment
This keeps the equipment selection tied to the actual forming requirement rather than starting from a fixed machine power or frequency.
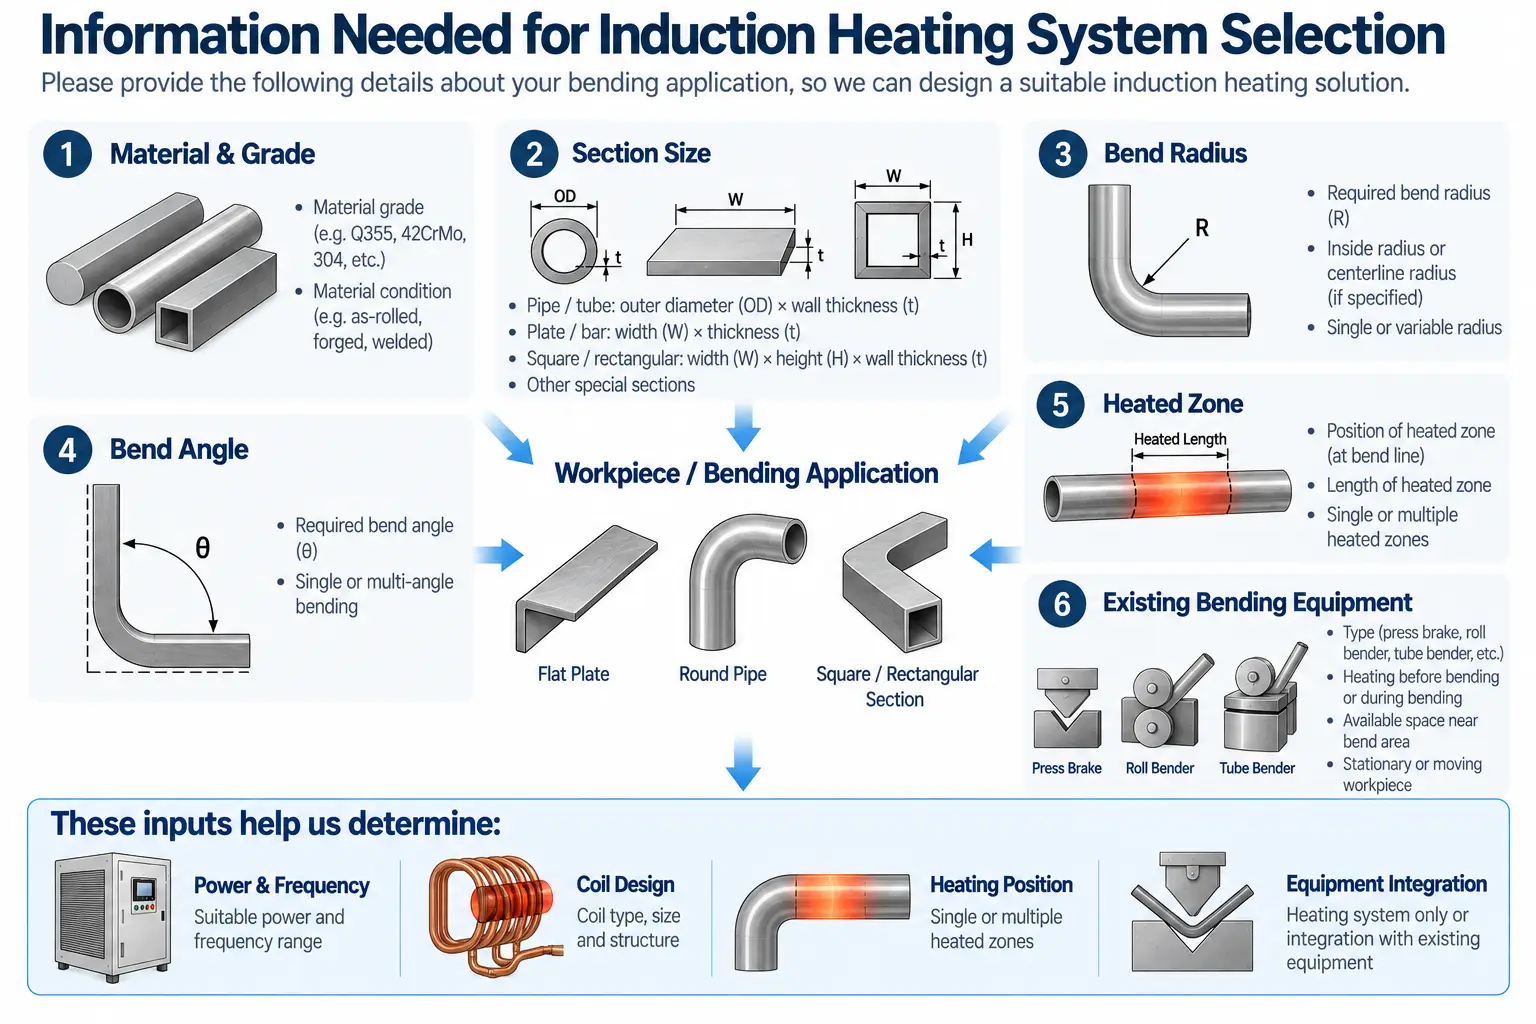
Key workpiece and process inputs for selecting a bending heating system.
답변을 펼치려면 질문을 클릭하세요..
Does induction heating bend the metal itself?
아니요. The induction system only heats a selected area before or during forming. The actual deformation is produced by the press, roll bender or other forming equipment.
What frequency is used for induction bending?
There is no single frequency. It depends on the workpiece geometry, section thickness and required heating depth. A documented steel-plate example used a 5–15 kHz system at about 13 kHz, but that is not a universal setting.
Do I need a complete induction bending machine, or just a heater?
If you already have a press or roll bender, you may only need a controlled heating station. A complete induction bending machine is needed when heating, movement and mechanical bending must be coordinated in one system.
Does preheating eliminate bending defects?
아니요. Heating improves forming conditions but does not remove mechanical defects such as cracking, springback or wall thinning. Bend radius, tooling and forming sequence still matter.
Request a Bending Heating Solution
공작물 도면 보내기, section thickness and bend requirements. We can help you select the right induction heating system or complete bending machine for your forming process.










