V-홈 롤러용 고주파 경화 시스템
Ⅰ. V-Groove Roller Induction Hardening in Operation
영상: Induction heating of a V-grooved rotating component using a custom-profiled copper inductor.
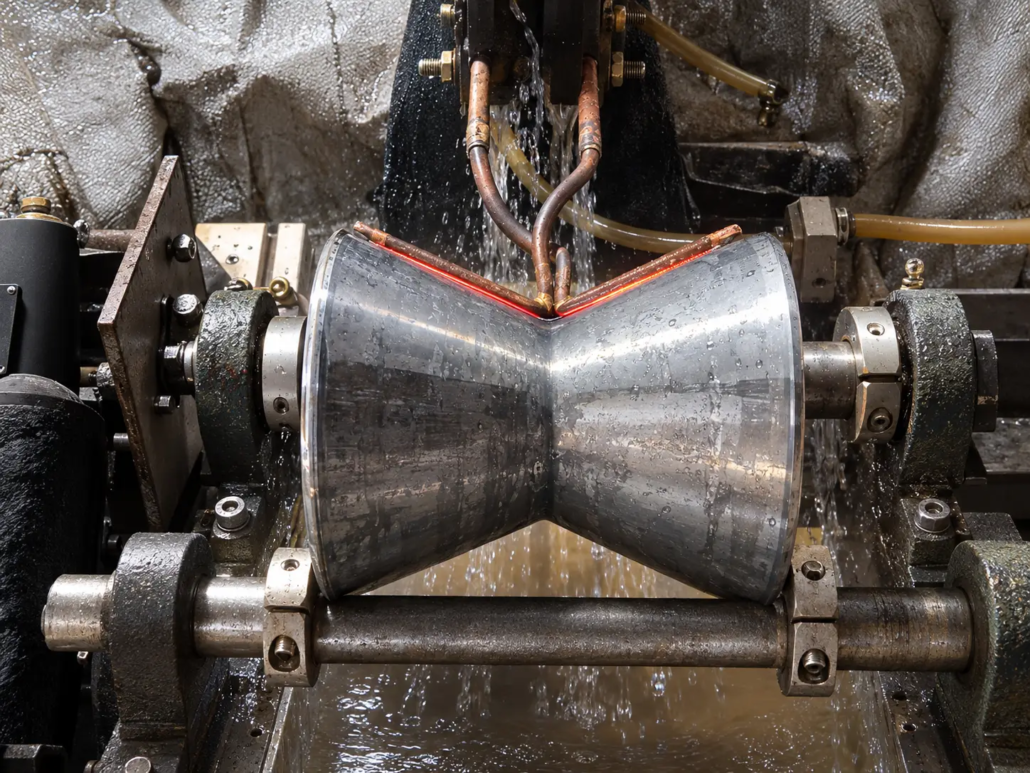
The video shows a metal component mounted horizontally between two supporting fixtures. A V-shaped copper inductor is positioned close to the groove surfaces while the workpiece rotates.
The inductor follows the groove profile, directing heat toward the inclined surfaces and groove root. As the component turns, successive sections of the circumferential groove pass through the heating region.
This arrangement allows the heating process to focus on the V-groove rather than the entire workpiece.
Demonstrated Equipment and Process
| 목 | 설명 |
|---|---|
| 워크피스 | Rotating metal component with a circumferential V-groove |
| 난방 면적 | V-shaped groove surfaces |
| 적용 | Localized induction surface hardening |
| 가열방식 | High-frequency induction heating |
| 인덕터 | Custom-profiled copper coil |
| 공작물 이동 | Horizontal rotation |
The footage shows localized heating and liquid around the working area, but does not establish the complete quenching arrangement or finished hardness results.
Ⅱ. V-Groove Workpieces and Industrial Applications
V-shaped grooves are used on rollers, wheels, pulleys and other rotating components. Where the groove surfaces are subject to wear or contact loading, 인덕션 경화 can be used to produce a specified hardened region in suitable steels.
Our equipment covers a range of grooved components, 포함하여:
•V-Groove Guide Rollers: Grooved running surfaces used in mechanical guiding and positioning systems.
•V-Groove Track Wheels: Wheels with inclined contact surfaces running against matching tracks.
•V-Belt Pulleys and Grooved Sheaves: Belt- and rope-guiding components with circumferential grooves.
•V-Profile Forming Rollers: Profiled working surfaces used in metal forming and rolling applications.
•Grooved 샤프트, Hubs and Sleeves: Rotational components with annular V-shaped grooves requiring localized surface treatment.
These applications differ in size, 재료, loading conditions and hardening requirements. The equipment is therefore developed around the actual part rather than a fixed roller design.
For each workpiece, the first consideration is which surfaces require hardening: the groove flanks, the root, or a defined area extending across the profile.
Ⅲ. Profiled Inductor Design and Rotary Heating
The main challenge in V-groove induction hardening is controlling the heating pattern across surfaces that do not share the same geometry.
The groove flanks are inclined, while the root forms a narrower transition between them. Their distance from the induction coil and local electromagnetic coupling conditions can differ, affecting how quickly each region heats.
Custom-Profiled Inductor
이 copper inductor is shaped to follow the V-groove profile. Its position and clearance are selected to direct heating toward the specified surfaces.
Coil design takes account of the groove angle, 너비, 깊이, root radius and workpiece diameter, along with material properties and the required hardening pattern.
Matching the coil to the groove does not automatically produce equal temperatures across the profile. The relationship between coil clearance, 작동 주파수, heating power and duration must be evaluated, particularly at the groove root.
For demanding hardening patterns, trial heating and inductor adjustments may be needed.
Rotary Workpiece Fixture
The demonstrated system holds the workpiece horizontally and rotates it relative to the inductor.
The fixture supports the component, maintains alignment and keeps the groove in the intended heating position. Rotation speed is coordinated with heating power and duration to develop the required circumferential heating pattern.
Changes in roller diameter, groove profile or workpiece weight may call for different supports, locating arrangements or inductor dimensions.
Quenching the Groove Surfaces
Induction surface hardening requires suitable heating followed by cooling under conditions that produce the specified hardened structure.
For V-shaped grooves, quenchant access to the inclined flanks and root needs particular attention. Differences in cooling distribution can affect the resulting hardness profile and effective case depth.
The quenching arrangement is designed alongside the heating process. Depending on the equipment layout, cooling may take place at the heating position or at a separate station.
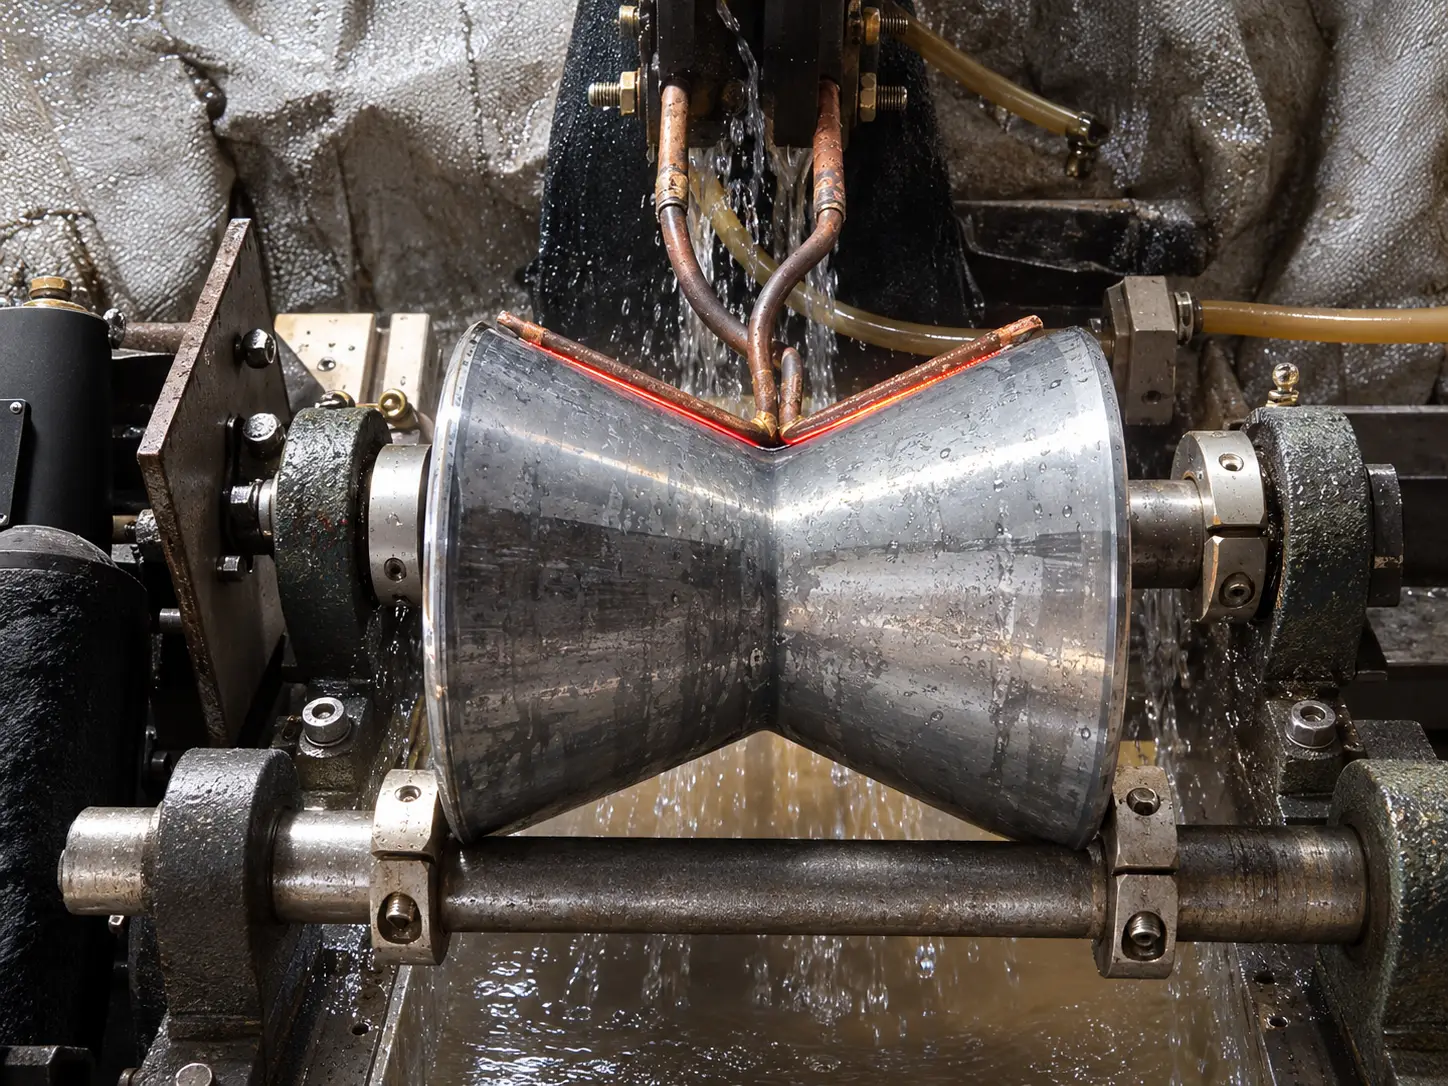
V-groove roller workpiece being quenched after induction heating.
Final hardness, case depth and dimensional changes must be verified through appropriate inspection rather than inferred from the visible heating pattern.
Ⅴ. 기계 구성 및 프로세스 제어
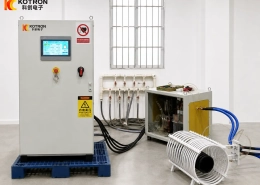
The system brings together the induction power supply, profiled inductor, rotating fixture and the equipment required to complete the hardening cycle.
| 구성 요소 | 장비 구성 |
|---|---|
| 유도 전원 공급 장치 | Output power and frequency selected for the material, groove dimensions and heating cycle |
| Profiled Inductor | Coil shape and clearance matched to the required groove heating area |
| Rotary Fixture | 공작물 지원, alignment and controlled rotation |
| 가열 제어 | Coordination of power, heating time and workpiece movement |
| 담금질 장비 | Cooling arrangement developed for the groove geometry and hardening specification |
| 자동화 | 로드 중, positioning and cycle control as required by production |
Power Supply and Controls
Our induction heating equipment includes digitally controlled power supply options. 전력 조절, heating duration and workpiece rotation can be coordinated through the selected control arrangement.
The required electrical configuration is established together with the inductor. Power and operating frequency cannot be selected reliably from the nominal roller diameter alone.
Production Arrangement
The video demonstrates a horizontal rotary heating setup. For other grooved components, fixture dimensions, workpiece handling and machine layout are adapted to the manufacturing process.
A manually loaded machine may suit smaller batches, while automated loading and coordinated cycle control can be incorporated for repeated production.
The final equipment arrangement must also provide suitable access for inductor maintenance, workpiece changeover and quenching operations.
자주 묻는 질문
답변을 펼치려면 질문을 클릭하세요..
What materials are suitable for V-groove induction hardening?
Induction hardening requires enough carbon to form a hardened layer, so medium- and high-carbon steels and suitable alloy steels are typical. Hardness and case depth depend on the material, heating cycle and quench.
Why does the workpiece rotate during V-groove hardening?
Rotation carries each circumferential section of the groove through the heating region, so the flanks and root reach a consistent temperature instead of only the area facing the inductor.
How is the inductor matched to my V-groove geometry?
The inductor is profiled from the groove angle, 너비, depth and root radius, together with the workpiece diameter and required hardening area. Coil-to-workpiece clearance and the heating cycle are set with the profile to establish the intended heating pattern.
What information do you need to prepare a technical proposal?
A workpiece drawing or photos, the material or steel grade, main dimensions and V-groove profile, the required hardening area, and production quantity or cycle requirements. Target hardness and effective case depth help refine the proposal.
Ⅴ. Request a Customized V-Groove Induction Hardening Solution
We provide induction hardening equipment for V-groove rollers, guide wheels, pulleys, sheaves, forming rollers and other grooved rotational components.
To discuss your application, 보내주세요:
•공작물 도면 또는 사진
•재질 또는 강종
•Main dimensions and V-groove profile
•필요한 경화 면적
•Production quantity or cycle requirements
이미 지정된 경우, include your target hardness, effective case depth and inspection requirements.
With these details, we can review the heating method, 인덕터 설계, rotary fixture and quenching requirements, then propose an appropriate equipment configuration.
Send Us Your V-Groove Workpiece Details
We will review your workpiece and process requirements and propose an appropriate equipment configuration.