
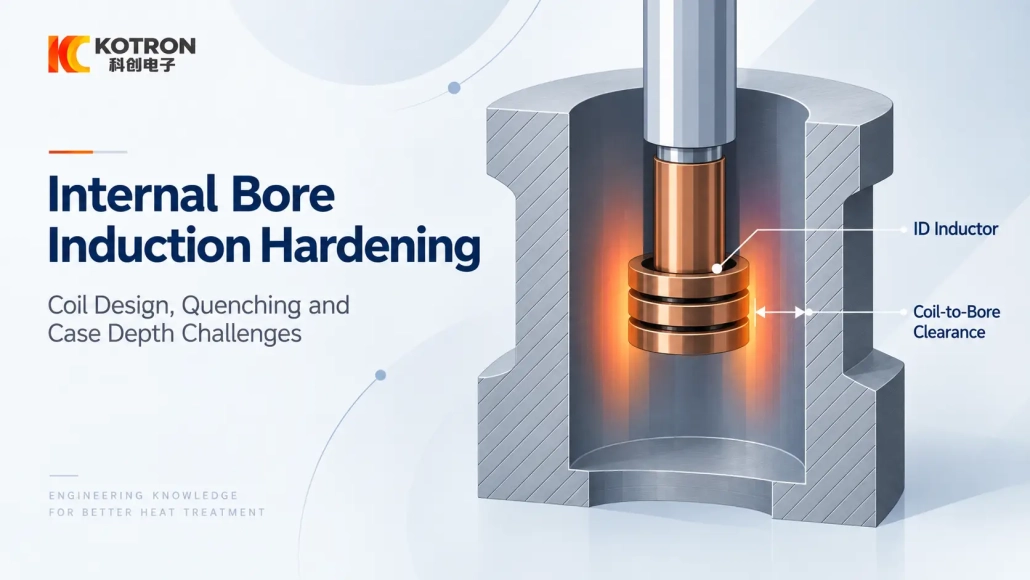
Hartowanie indukcyjne otworu wewnętrznego: Projekt cewki, Wyzwania dotyczące hartowania i głębokości obudowy
How Bore Geometry, ID Inductor Position and Quenching Affect the Final Hardened Zone
Hartowanie indukcyjne can be applied to internal bores, but the process is constrained by the space available inside the part. The inductor must reach the required area, maintain a suitable relationship with the bore surface, and leave enough access for quenching.
Z tego powodu, na średnica wewnętrzna (ID) proces hartowania is normally evaluated from the actual part geometry rather than from bore diameter alone.
2. ID Inductor Design, Clearance and Positioning
3. Quenching Inside the Bore
4. What Controls Case Depth in Bore Hardening?
5. What Should Be Checked When the Result Is Wrong?
6. What Information Is Needed for an Initial Evaluation?
1. Can an Internal Bore Be Induction Hardened?
The first question is not the machine size or power rating. It is whether the part itself is suitable for the required hardening result.
Material hardenability, geometria otworu, the location of the hardened area and access for the inductor all matter. A relatively open bore may be straightforward to reach, while a narrow, deep or recessed bore can place much tighter limits on the tooling.
The required treatment zone also changes the problem. A short hardened band close to the bore entrance does not require the same inductor arrangement as a zone located deeper inside the component.
A part drawing—preferably a sectional drawing showing the required hardened area—is therefore more useful than a bore diameter by itself.
2. ID Inductor Design, Clearance and Positioning
A bore-hardening inductor has to operate inside the workpiece rather than around its outside surface.
It must fit into the available space while maintaining an appropriate coupling relationship with the area being heated. Średnica otworu, głębokość, insertion path and hardened-zone location all influence the shape of the ID induction hardening coil or internal inductor.
Centering is another practical issue. If the inductor sits noticeably closer to one side of the bore wall, the circumferential heating pattern may change. Przy powtarzalnej produkcji, the fixture or machine movement may therefore need to control the relative position of the part and inductor.
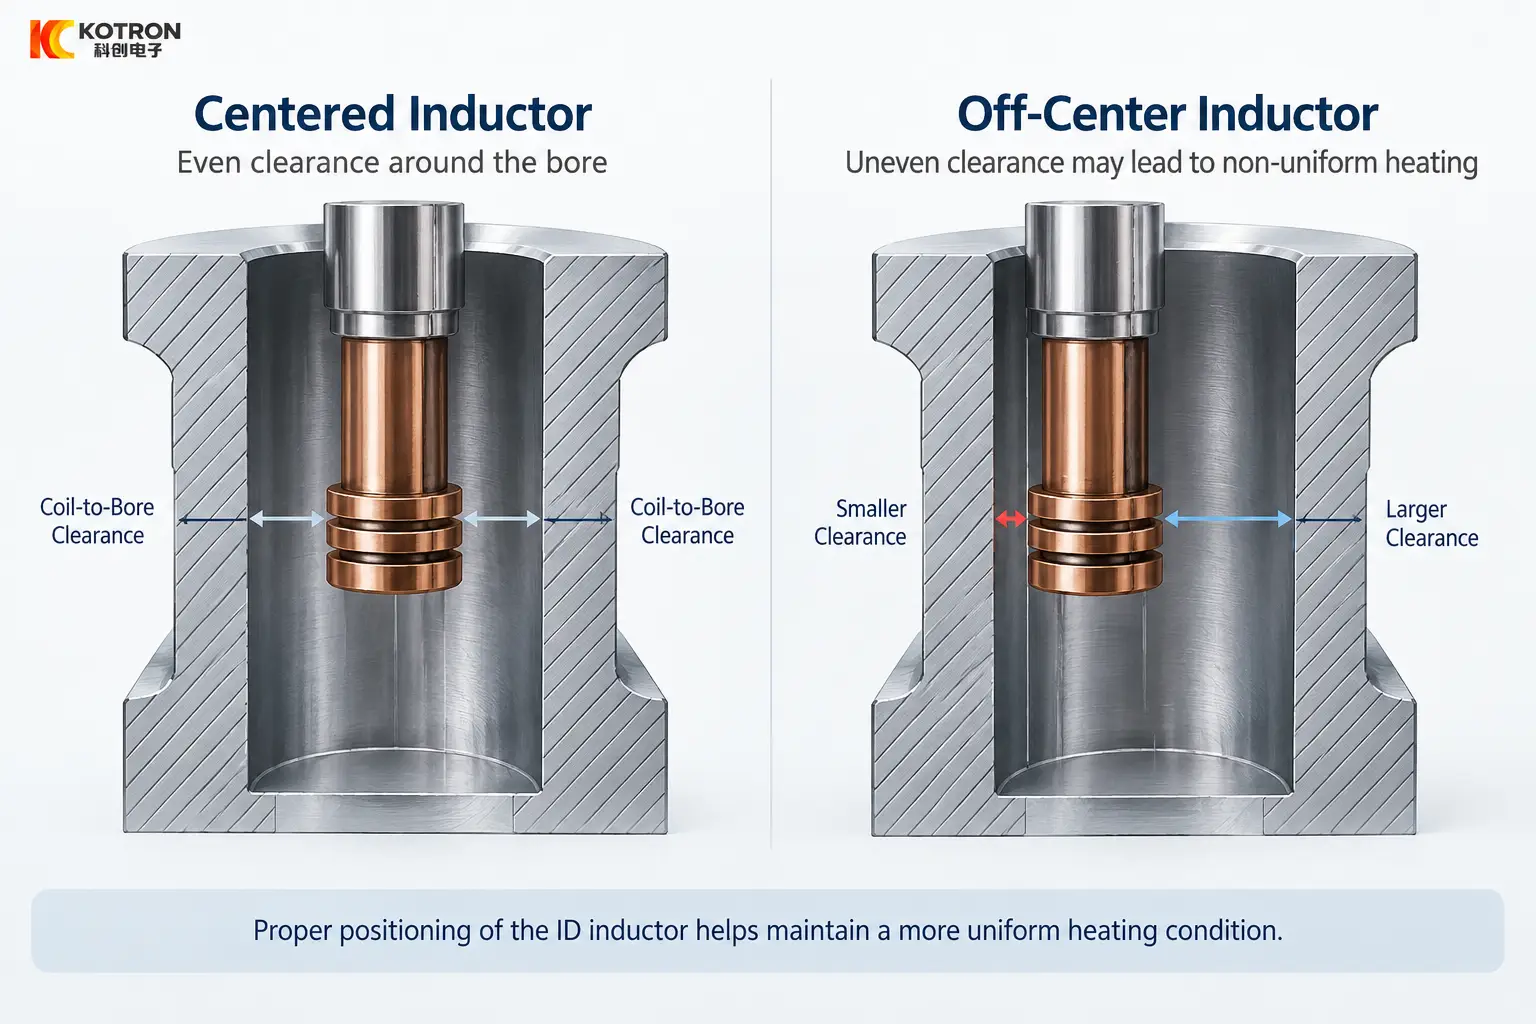
Centered versus off-center ID inductor clearance inside a bore.
The surrounding section geometry matters as well. A nominally round bore can still have different thermal conditions around its circumference if the amount of surrounding material varies from one side to another.
This is why a coil that physically fits inside the bore is not automatically a suitable hardening inductor.
3. Quenching Inside the Bore
Heating the target surface is only one part of the process. The heated zone must also be quenched in a way that supports the specified hardness and case depth.
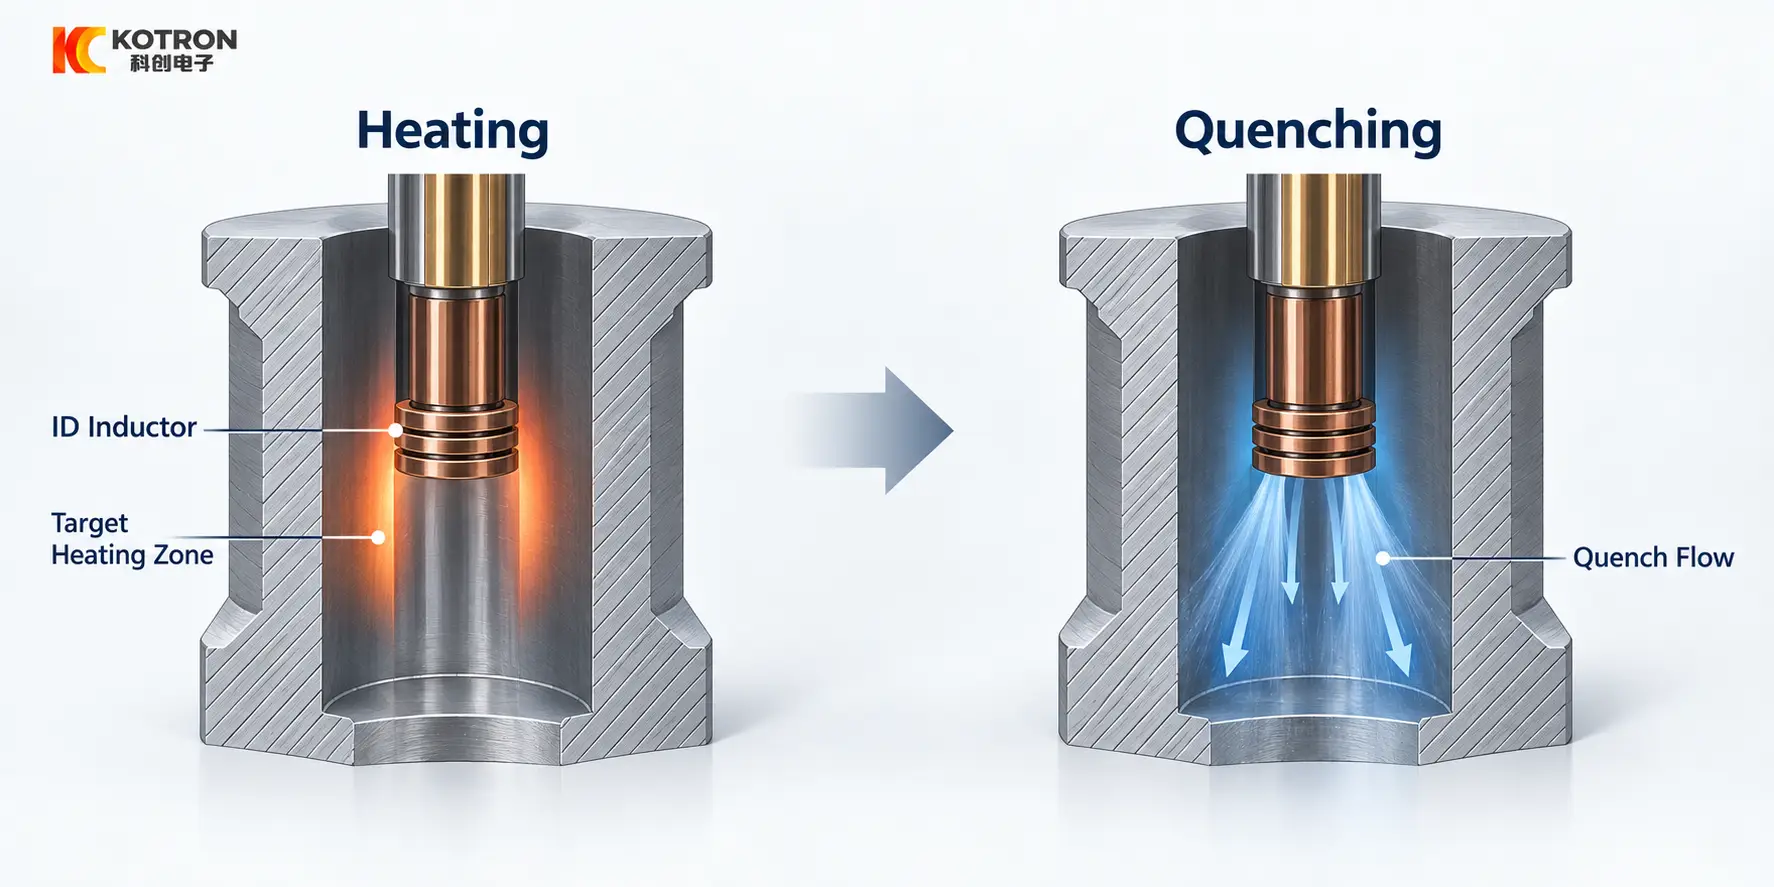
Heating followed by quenching inside an internal bore.
Internal surfaces can restrict coolant access, particularly when the hardened area is located deeper inside the part. Głębokość otworu, workpiece orientation and available space around the inductor can all affect the quenching arrangement.
W zależności od zastosowania, quenching may be provided by separate tooling or incorporated into the inductor assembly. Neither arrangement should be treated as universally preferable; the choice depends on the geometry and required treatment zone.
The visible heating pattern should not be taken as proof of the final hardness pattern. The hardened result is produced by the combined effect of material response, heating and subsequent cooling.
4. What Controls Case Depth in Bore Hardening?
Częstotliwość pracy is one factor in case-depth development, but it should not be considered independently.
The actual hardened depth also depends on the material, czas nagrzewania, delivered power, inductor-to-surface relationship, local geometry and quenching conditions.
This is particularly relevant in ID induction hardening, where tooling space may already limit the possible inductor geometry.
A target case depth therefore does not, samodzielnie, define the required frequency or power supply. Those choices have to be made together with the bore dimensions, hardened-zone location and process layout.
5. What Should Be Checked When the Result Is Wrong?
When the hardened result does not match the drawing or specification, the first step is to separate positioning, heating and quenching issues.
| Zaobserwowany wynik | Areas to Check First |
|---|---|
| One side of the bore heats more strongly | Inductor centering, local clearance, surrounding section geometry |
| Hardened zone is too high or too low | Axial inductor position, głębokość włożenia, fixture position |
| Heated length does not match the required zone | Geometria cewki indukcyjnej, efektywna długość ogrzewania, położenie obrabianego elementu |
| Surface reaches the expected heating condition but hardness is low | Reakcja materialna, cykl ogrzewania, hartowanie |
| Case depth varies around the bore | Sprzężenie, geometria części, przepływ ciepła, warunki hartowania |
| Required zone is difficult to reach | Głębokość otworu, internal features, inductor access |
| Part-to-part variation is high | Fixture repeatability, pozycja cewki indukcyjnej, process settings |
These checks help identify where to investigate, but final acceptance should be based on the specified hardness, hardened-zone location and case depth where required.
A surface that appears evenly heated does not necessarily have the correct final hardened result.
6. What Information Is Needed for an Initial Evaluation?
Do wstępnej recenzji, the most useful information is usually simple:
— A part drawing or clear photo
— Materiał, jeśli jest znany
— Średnica i głębokość otworu
— The area that needs to be hardened
Jeśli docelowa twardość, głębokość obudowy lub wymagania produkcyjne są już zdefiniowane, they can be added later or included with the first enquiry.
Z tą informacją, the feasibility of the bore hardening process, ID inductor arrangement, quenching method and equipment configuration can be reviewed before detailed machine selection.
Klucz na wynos
Hartowanie indukcyjne wnętrza otworu is a fit-and-access problem before it is a heating problem. The inductor must reach the required zone, hold its position relative to the bore wall and leave room for quenching. The final result is confirmed by the specified hardness, hardened-zone location and case depth—not by how evenly the surface appears heated.
Często zadawane pytania
Kliknij pytanie, aby rozwinąć odpowiedź.
Can any internal bore be induction hardened?
Nie. Material hardenability, geometria otworu, hardened-zone location and inductor access all matter. A narrow, deep or recessed bore places much tighter limits on the tooling than an open bore.
Does operating frequency alone determine case depth?
Nie. The hardened depth also depends on the material, czas nagrzewania, delivered power, inductor-to-surface relationship, local geometry and quenching conditions.
Does an evenly heated surface guarantee a correct result?
Nie. The hardened result is produced by material response, heating and cooling together. A surface that appears evenly heated may still have incorrect hardness, zone location or case depth.
What should I check first when the result is wrong?
Separate positioning, heating and quenching issues. Start with inductor centering, axial position, efektywna długość ogrzewania, coupling and fixture repeatability.
Jakie informacje muszę przesłać w celu wyceny?
A part drawing or clear photo, materiał, jeśli jest znany, średnica i głębokość otworu, and the area to be hardened. Twardość docelowa, case depth and production requirements can be added later.
Wyślij nam rysunek części
Wyślij rysunek lub wyraźne zdjęcie swojego elementu wraz z materiałem i obszarem, który ma być utwardzany. We’ll review the bore hardening process, ID inductor arrangement, quenching method and equipment configuration for your application.



