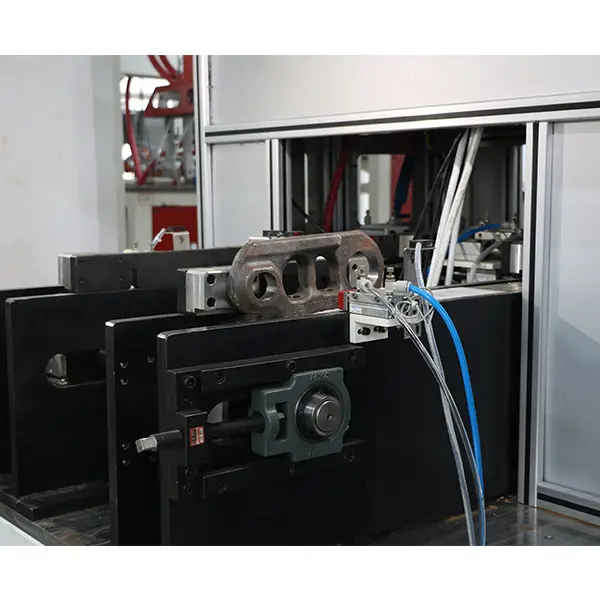
خط التقسية الحثي لوصلة المسار مع التقسية للحفارات والجرافات
Ⅰ. Track Link Hardening and Tempering Line Overview
Crawler track links are important components of tracked undercarriage assemblies used in construction and earthmoving machinery.
The tread surface, also called the rail surface, forms the contact area between the track link and the undercarriage rollers. This working surface requires suitable mechanical properties to withstand repeated contact and wear during operation.
KECHUANG’s track link hardening line is designed to treat the specified tread area while coordinating the subsequent tempering and cooling operations.
The complete production process consists of:
①Workpiece Loading
②التسخين بالحث
③البرودة
④التلطيف
⑤Post-Tempering Cooling
⑥Workpiece Transfer
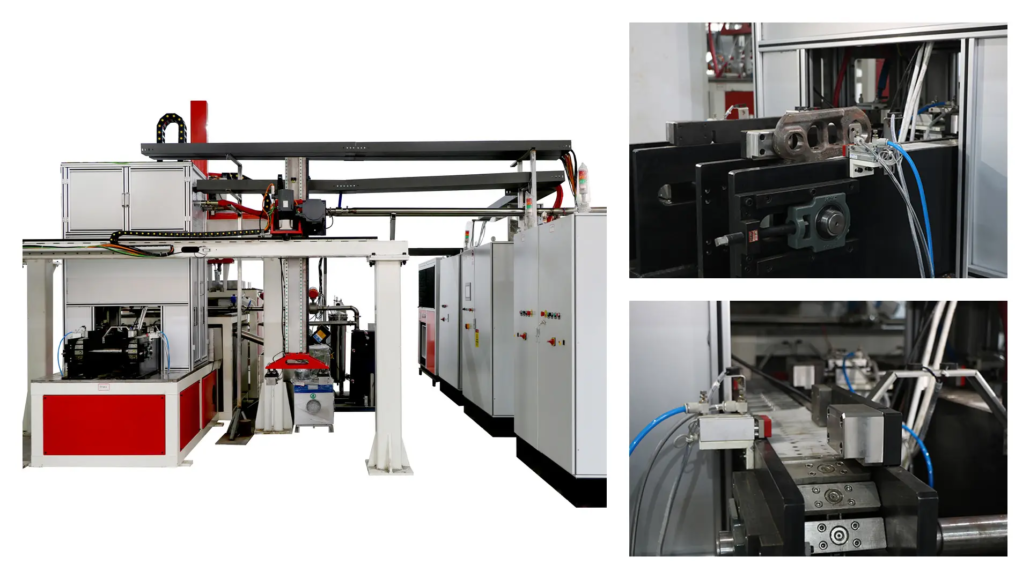
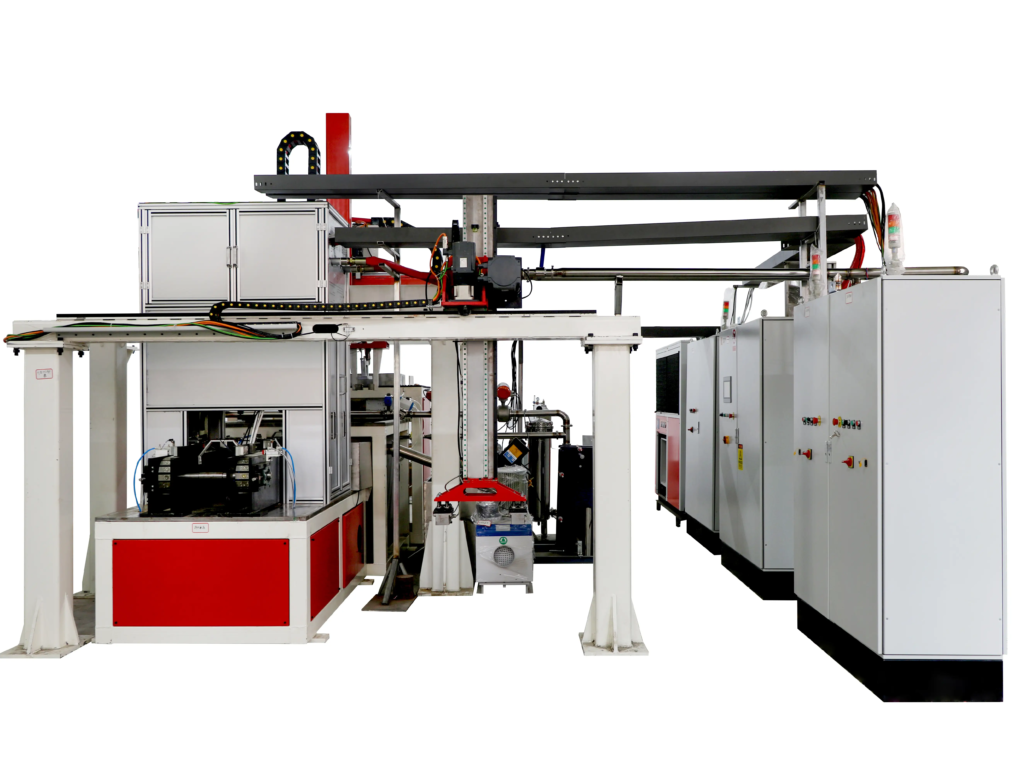
The production line incorporates dedicated processing positions, a mechanical transport system and coordinated operating controls.
Its horizontal hardening machine uses a dual-workpiece arrangement, while the transport configuration supports dual-channel and batch processing applications.
The exact equipment layout and processing sequence are determined by the workpiece specifications and production requirements.
Ⅱ. Track Link Tread Surface Hardening
Track links have a different geometry from conventional shafts, rods and cylindrical parts. Their connecting holes, irregular cross-sections and defined roller-contact surfaces require dedicated workholding and heating arrangements.
Tread Surface Treatment
The primary treatment area is the track link tread or rail surface.
Induction heating is used to heat the required surface region before quenching. The induction coil and workpiece positioning system are designed around the specified treatment area.
The required heating pattern depends on the material, surface geometry, coil position and operating conditions.
Workpiece Requirements
The equipment configuration takes account of:
•Track link material and initial heat treatment condition
•Link pitch and overall dimensions
•Tread surface geometry and treatment location
•صلابة السطح المطلوبة
•Effective hardened case depth
•Production quantity and workpiece variety
Different track link specifications may require adjustments to the fixture, induction coil and operating program.
Hardening results must be verified against the customer’s material and inspection requirements.
Ⅲ. Induction Heating and Quenching Process
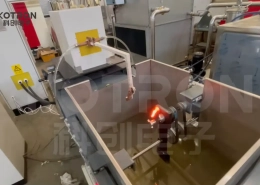
The hardening machine combines controlled workpiece positioning, induction heating and quenching.
تحديد موضع الشغل
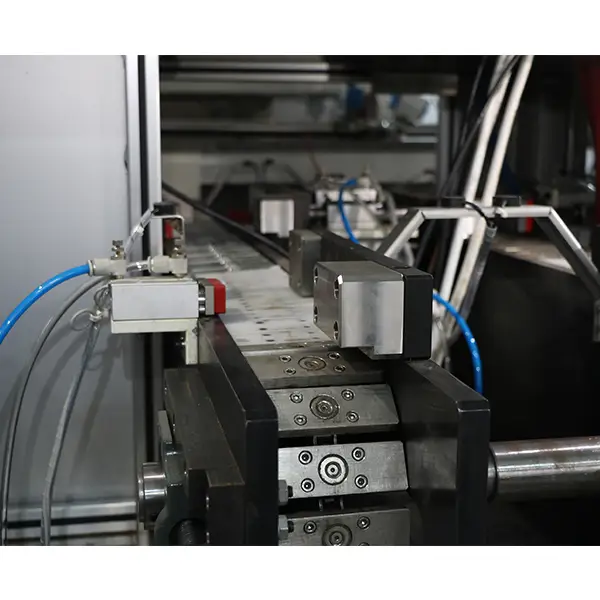
The track link is located and supported by dedicated mechanical fixtures.
The documented machine design uses guide-wheel positioning and provides for adjustment of the clearance between the inductor and workpiece.
These features help establish the required relationship between the induction coil and the tread surface during processing.
التسخين بالحث
The induction power supply delivers energy to the ملف الحث, generating an alternating electromagnetic field that heats the selected conductive region of the workpiece.
The heating arrangement is matched to the track link geometry and required hardening area.
Depending on the selected processing program, the machine supports different operating methods, بما في ذلك:
•Fixed-position timed hardening
•Programmed positioning and مسح
•Section-by-section positioning
•Stepwise preheating and quenching
The appropriate operating method depends on the workpiece geometry and heat treatment requirements.
البرودة
بعد التسخين, the specified surface region is quenched under conditions selected for the track link material.
The quenching system is coordinated with the heating sequence and workpiece positioning mechanism.
The documented equipment includes quenching-liquid collection, filtration and supporting cooling-water and pump-control systems.
The required quenching conditions are established according to the target hardness, hardened depth and material properties.
Ⅳ. Tempering and Post-Tempering Cooling
Tempering forms part of the complete track link heat treatment production line.
بعد التبريد, the track link proceeds to the التخطيط الحراري منصة. Tempering is used to adjust the properties of the hardened material according to the required mechanical performance.
The appropriate tempering conditions depend on the material grade and specified heat treatment requirements.
Tempering Section
The production line includes a dedicated tempering operation following the hardening process.
The heating method, temperature and operating sequence of the tempering equipment are established according to the selected line configuration.
Post-Tempering Cooling
بعد هدأ, the workpiece passes through a subsequent cooling stage.
The cooling operation is coordinated with the transport system to support movement through the production sequence.
The arrangement of the hardening, tempering and cooling sections is determined by the required production process and available equipment layout.
Ⅴ. Horizontal Dual-Workpiece Machine and Transfer System
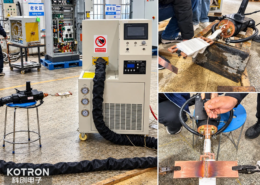
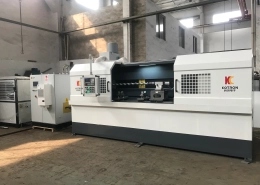
The KECHUANG equipment uses a horizontal, programmable hardening machine with a dual-workpiece processing arrangement.
The mechanical structure supports workpiece positioning, induction heating operations and controlled movement.
Dedicated Workpiece Fixtures
The fixture system accommodates the geometry of crawler track links.
Guide-wheel positioning helps locate the workpiece, while the induction coil clearance can be adjusted according to the selected processing requirements.
Fixtures and guides are configured for the applicable track link dimensions and treatment area.
Mechanical Movement and Support
The documented machine structure includes positioning and supporting mechanisms, a workpiece rotation mechanism, lifting and guiding components, and a counterbalance arrangement.
These components form part of the machine’s mechanical design. Their specific operation and coordination depend on the selected equipment configuration.
Dual-Channel Workpiece Transfer
A conveyor system moves workpieces through the production arrangement.
The equipment is designed to support dual-channel operation and batch treatment of crawler track links.
The dual-workpiece machine arrangement and dual-channel transfer arrangement describe different aspects of the equipment. They do not necessarily mean that two workpieces are heated simultaneously.
Adaptation to Different Track Link Pitches
The equipment is intended to accommodate track links with different pitches.
The applicable size range, adjustment method and fixture configuration are established according to the customer’s workpiece drawings.
Ⅵ. CNC/PLC Control and Auxiliary Systems
The track link hardening line integrates electrical control, mechanical movement and induction power regulation.
Programmable Process Control
The equipment can use a CNC or PLC-based control system together with variable-frequency speed control.
The control arrangement supports workpiece positioning and scanning operations, while communication between the PLC and induction power supply coordinates the heating sequence.
For CNC-equipped configurations, processing programs can be prepared and stored for different workpiece requirements.
This allows the machine to operate according to the selected track link specification without requiring continuous manual adjustment during the programmed hardening cycle.
Electrical Equipment Arrangement
The documented machine design places the control cabinet and transformer cabinet separately.
This arrangement provides access to the relevant electrical equipment and supports adjustment and maintenance.
The machine also includes a mounting and adjustment arrangement for the hardening transformer.
Supporting Machine Systems
The published equipment configuration includes:
•Quenching-liquid collection system
•Quenching-liquid filtration system
•Cooling-water circuit and pump-control system
•Door-control system
•Workpiece transport control
•Lifting and guiding mechanism
•Counterbalance mechanism
•Water-mist collection system
The production line documentation also identifies an energy and quality-control analysis system.
The specific measurements, analysis functions and available interfaces of this system should be defined in the equipment specification for the selected project.
Ⅶ. Machine Configuration and Technical Requirements
The complete line combines the main hardening machine with the tempering, التبريد, transfer and auxiliary equipment required for the selected production process.
تكوين المعدات الرئيسية
| نظام | وظيفة |
|---|---|
| آلة تصلب | أفقي, dual-workpiece programmable processing arrangement |
| مزود الطاقة بالحث | Provides energy for induction heating |
| لفة التحفيز | Designed for the specified track link tread surface |
| تركيبات الشغل | Supports and positions the track link |
| Guide-Wheel Positioning | Helps establish the required workpiece position |
| Transformer Assembly | Supports the induction heating arrangement and its adjustment |
| Mechanical Movement | Provides positioning, scanning and related machine movement functions |
| نظام التبريد | Cools the heated treatment area |
| Quenching-Liquid Collection and Filtration | Supports quenching-liquid handling |
| Tempering Section | Performs the subsequent tempering operation |
| Post-Tempering Cooling | Provides cooling after tempering |
| Conveyor and Transfer System | Moves workpieces between processing positions |
| CNC/PLC Control | Coordinates workpiece movement and machine operation |
| Auxiliary Systems | Cooling-water control, door control, mist collection and other supporting mechanisms |
Technical Parameters for Equipment Selection
The following parameters are established according to the customer’s track link specifications and production requirements.
| المعامل | Selection Requirement |
|---|---|
| Applicable Workpiece | Crawler track links |
| Treatment Area | Track link tread / rail surface |
| Primary Hardening Method | Induction heating and quenching |
| Production Process | تصلب, tempering and post-tempering cooling |
| ترتيب المعالجة | Horizontal dual-workpiece hardening machine |
| Transfer Arrangement | Dual-channel and batch-processing capability |
| قوة الحث | Selected according to the heating requirements |
| تردد التشغيل | Matched to the heating pattern and required hardening depth |
| Applicable Link Pitch | Determined by fixture and transfer configuration |
| Target Hardness | According to customer specifications |
| عمق الحالة الفعال | According to material and treatment requirements |
| قدرة الإنتاج | Determined by the complete processing sequence |
| نظام التحكم | CNC or PLC-based configuration |
القوة الفعلية, التردد, processing dimensions, production capacity and heat treatment parameters are specified for the selected equipment.
The final configuration must be matched to the material, track link geometry and required treatment results.
Ⅷ. Applications and Customized Equipment Selection
ثم يقوم track link induction hardening and tempering line is intended for manufacturers processing crawler undercarriage components.
Potential applications include suitable track link designs used in:
•حفارات
•Bulldozers
•Crawler tractors
•Mining and earthmoving machinery
•Other tracked industrial equipment
The applicable workpiece range depends on the material, geometry and required treatment conditions.
How to Select the Right Track Link Hardening Line
Equipment selection begins with the actual track link.
The link pitch and geometry determine the fixture and transfer requirements. The specified tread surface and hardening depth guide the induction coil design and processing conditions.
Required production quantity and workpiece variety influence the machine layout, transport configuration and program requirements.
Where hardness and case-depth specifications are available, process trials may be necessary to establish and verify the required heating, ظروف التبريد والتلطيف.
Request a Customized Track Link Hardening and Tempering Line
KECHUANG provides customized induction hardening equipment and integrated heat treatment systems for crawler track link manufacturing.
For an equipment evaluation, من فضلك أرسل:
•Track link drawings or photos
•درجة المادة
•Link pitch and main dimensions
•Required tread surface treatment area
•Target hardness and effective case depth
•Expected production quantity
إذا كان متاحا, please also provide tempering requirements, inspection standards and your existing production-line layout.
Our engineering team can evaluate the induction heating assembly, تحديد المواقع الشغل, transfer system, ترتيب التبريد, tempering section and operating controls according to your manufacturing requirements.
الأسئلة المتداولة
انقر فوق سؤال لتوسيع الإجابة.
+What does the track link induction hardening line treat?
The line hardens and tempers the tread (السكك الحديدية) surface of crawler track links — the contact area between the link and the undercarriage rollers that must withstand repeated contact and wear during operation.
+Can the machine handle different track link pitches?
نعم. المباراة, induction coil and operating program are adjusted for each link pitch and geometry. CNC-equipped configurations store programs for different specifications, so the machine can switch between track link types without continuous manual adjustment.
+Does the production line include tempering?
نعم. بعد التبريد, the track link proceeds to a dedicated tempering section, followed by post-tempering cooling before automated transfer. Tempering adjusts the hardness and mechanical properties of the quenched material. For a related fully automated line, راجعنا automatic induction hardening and tempering line.
+What determines the induction coil design and hardening parameters?
The track link material, tread surface geometry, required surface hardness and effective case depth determine the coil design, نمط التدفئة وظروف التبريد. Hardening results are verified against the customer’s material and inspection requirements.
+What do I need to send for an equipment evaluation?
Send track link drawings or photos, درجة المادة, link pitch and main dimensions, the required tread surface treatment area, target hardness and effective case depth, and expected production quantity. Tempering requirements and inspection standards are also helpful.
Request a Customized Track Link Induction Hardening Line
Send your track link drawings for a free equipment evaluation. Our engineering team will assess the induction heating assembly, تحديد المواقع الشغل, transfer system, ترتيب التبريد, tempering section and operating controls for your manufacturing requirements.