Epoxy-Coated Prestressing Steel Strand Production Line
Ⅰ. See a Real Epoxy-Coated Steel Strand Line
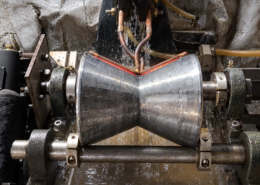
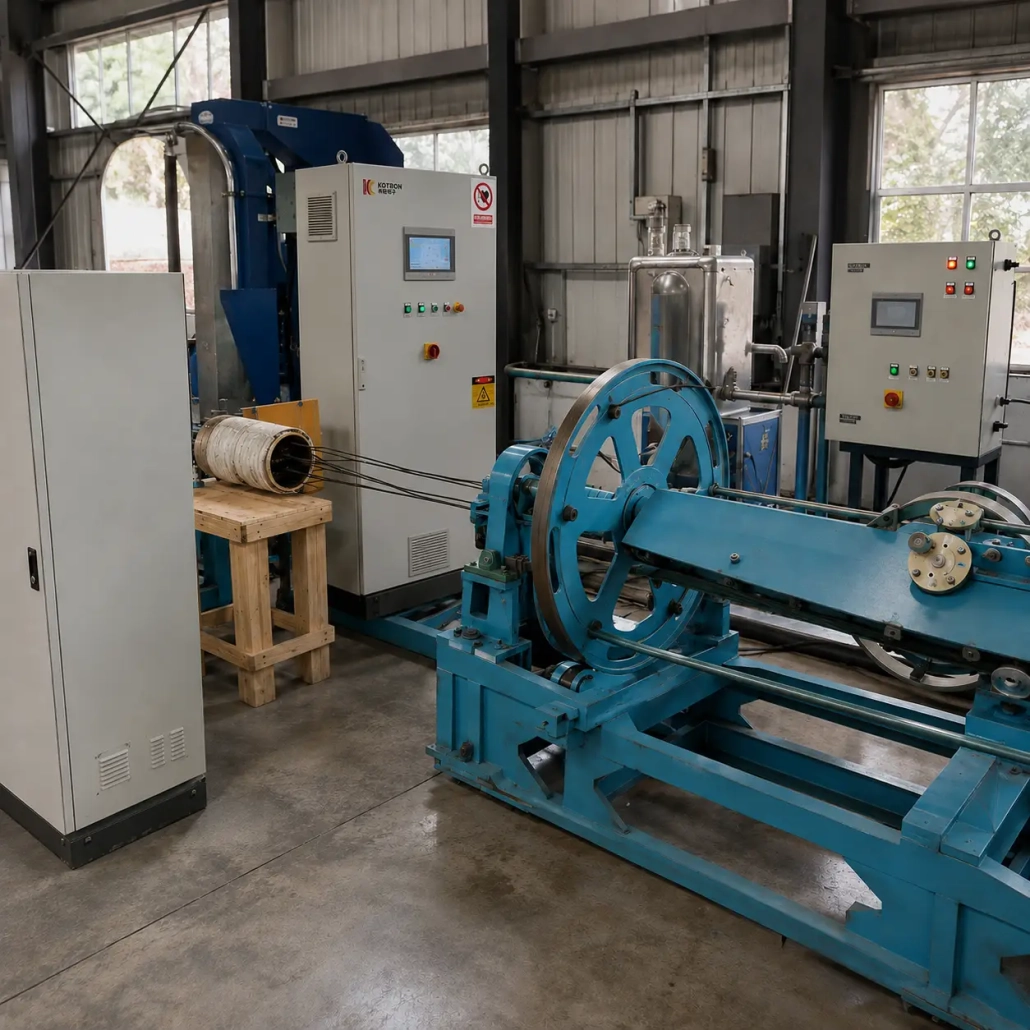
The video shows one steel strand processing line built around a specific production requirement. You can see the continuous strand passing through the heating section together with the mechanical handling units used along the line.
For another project, the equipment sequence, line length and individual stations may be different. We use the actual product and process requirement as the starting point rather than asking every customer to use the same standard line.
A typical line follows a continuous process:
1. Pay-off
2. Surface Preparation
3. Induction Heating
4. Strand Opening
5. Epoxy Coating
6. Restranding
7. Curing / Cooling
8. Inspection
9. Traction
10. Take-up
Ⅱ. How the Epoxy-Coated Steel Strand Production Line Works
A typical line follows a continuous process: Pay-off → Surface Preparation → Induction Heating → Strand Opening → Epoxy Coating → Restranding → Curing / Cooling → Inspection → Traction → Take-up
The exact sequence depends on the type of epoxy-coated strand to be produced.
The incoming PC strand is first released under controlled tension and prepared for coating. Surface condition is important because oil, rust, scale or other contamination can affect coating adhesion.
The strand then passes continuously through the induction heating section. Heating conditions are matched to the strand specification, line speed and coating process instead of being set to one universal temperature.
Where the coating process requires access between the individual wires, the strand is opened before or around the coating section. Epoxy powder is then applied to the heated steel surface. The opening and coating arrangement can be developed according to the required strand structure and coating method.
After coating, the wires are returned to the required strand geometry. The coated strand then passes through the required curing and cooling stages before inspection and final take-up.
1
Pay-off
2
Surface Preparation
3
Induction Heating
4
Strand Opening
5
Epoxy Coating
6
Restranding
7
Curing / Cooling
8
Inspection
9
Traction
10
Take-up
Ⅲ. Main Equipment in the Production Line
A complete line can be assembled from several functional sections.
Pay-off and Tension Control
Feeds the strand into the line while maintaining suitable tension for continuous processing.
Surface Preparation
Cleans and prepares the strand surface before heating and coating. The final method is selected according to the incoming strand condition and coating requirement.
Induction Heating System
Continuously heats the moving strand before epoxy powder application. The inductor, power supply and operating frequency are selected around strand size and production speed.
Strand Opening Unit
Controls the strand geometry where individual wires need to be separated for the coating process.
Epoxy Powder Coating Section
Applies epoxy powder to the heated steel strand. The coating section can be configured around the required product and process.
Restranding Unit
Returns the opened wires to the required strand arrangement after coating.
Curing and Cooling Section
Provides the necessary downstream thermal process and reduces strand temperature before inspection and winding.
Traction and Take-up
Maintains continuous movement through the line and rewinds the finished strand for subsequent handling.
Individual stations can be changed, added or integrated with existing customer equipment.
Ⅳ. Continuous Induction Heating for Steel Strand
Induction heating is one of the key sections of the line.
Unlike batch heating, the strand travels continuously through a through-type induction coil. Heat is generated directly in the steel as it moves through the electromagnetic field, allowing the heating section to operate as part of the continuous coating process.
The important point is not simply to reach a high temperature quickly.
Strand diameter, steel mass, line speed, required temperature, heating length, frequency, available power and coil design have to work together.
A line running a different strand diameter or at a different speed may therefore require a different induction heating configuration.
Our induction heating systems use IGBT power conversion with DSP digital control. Depending on the selected configuration, operating values such as voltage, current, power and frequency can be monitored, while the heating system can communicate with the line control system.
Temperature measurement and closed-loop control can also be configured where required by the process.
The induction coil itself is not treated as a universal component. Its internal diameter, effective heating length, insulation structure and connection to the power supply are developed according to the strand and line arrangement.
For customers upgrading an existing coating line, the induction heating section can also be evaluated as an individual subsystem rather than requiring replacement of the complete production line.
Ⅴ. Customized Around Your Strand and Production Target
Customization is not limited to changing the machine dimensions.
The product being manufactured directly affects the design of the line.
| Customer Requirement | Line Configuration Affected |
|---|---|
| Strand diameter and structure | Guides, opening unit, inductor and tooling |
| Target line speed | Heating capacity, coating section and cooling length |
| Coating process | Strand opening, coating and downstream processing |
| Required production capacity | Line speed and equipment configuration |
| Coil size / coil weight | Pay-off and take-up system |
| Factory space | Equipment layout and line length |
| Existing equipment | Interface and integration design |
| Automation requirement | PLC, HMI, monitoring and communication |
For this reason, two lines producing epoxy-coated PC strand may look quite different even though the final product belongs to the same general category.
A customer with an existing strand line may only need surface preparation, induction heating and coating-related equipment. A new plant may require a complete line from pay-off to finished-strand take-up.
We can configure either approach according to the project.
Ⅵ. Additional Line Configuration
Automation and Control
PLC and HMI control can be used to coordinate strand movement, heating and other production stations. Depending on the project, operating parameters, alarms, process recipes, temperature information and production records can also be incorporated into the control system.
Technical Configuration
There is no single meaningful power, frequency or production-speed specification for every epoxy-coated strand line. Induction power, operating frequency, line speed, coil size, pay-off capacity and take-up capacity are selected after the required product and production target are known.
Quality Inspection
Inspection stations can be integrated according to the finished-strand requirement, including coating surface inspection, coating thickness measurement and continuity or pinhole detection where required.
Applications
Epoxy-coated prestressing strand is used where corrosion protection is required in prestressed and anchored structures. Applications may include bridges, civil engineering, ground anchoring and certain underground or mining support projects, depending on the strand specification.
Ⅶ. Frequently Asked Questions
Click a question to expand the answer.
Can the line be customized for different strand diameters?
Yes. Strand diameter affects the guides, opening mechanism, induction coil, heating requirement and other parts of the line. The suitable operating range should be defined before the final mechanical design.
Can you supply only the induction heating section?
Yes. A project does not necessarily have to start with a completely new line. The induction heating power supply, matching system and customized through-type inductor can be developed for integration with an existing production process.
How do you select induction heating power?
Power should not be selected from strand diameter alone. Strand mass, target temperature, heating length, required line speed and process conditions all affect the result.
Can an existing production line be upgraded?
In many cases, individual process sections can be redesigned or integrated with existing equipment. The practical solution depends on the existing line layout, control system and required finished product.
Is every epoxy-coated strand line the same?
No. The line arrangement depends on the strand structure, coating process, production speed, required inspection and degree of automation. The production line shown in our video should be treated as one project example, not a fixed standard configuration.
Request a Customized Production Line Proposal
If you are planning a new epoxy-coated PC strand production line or upgrading an existing line, send us your basic strand specification, coating requirement and target production capacity.
We can evaluate the process layout, induction heating system, strand handling equipment and automation configuration around your project.
Send Your Strand Specification →
Discuss Your Production Line →