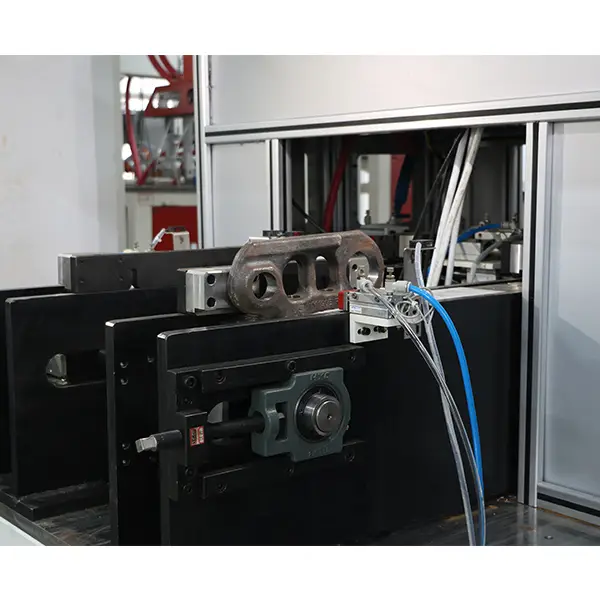
Automatic Track Link Tread Induction Hardening and Tempering Line
Ⅰ. Track Link Heat Treatment Line in Operation
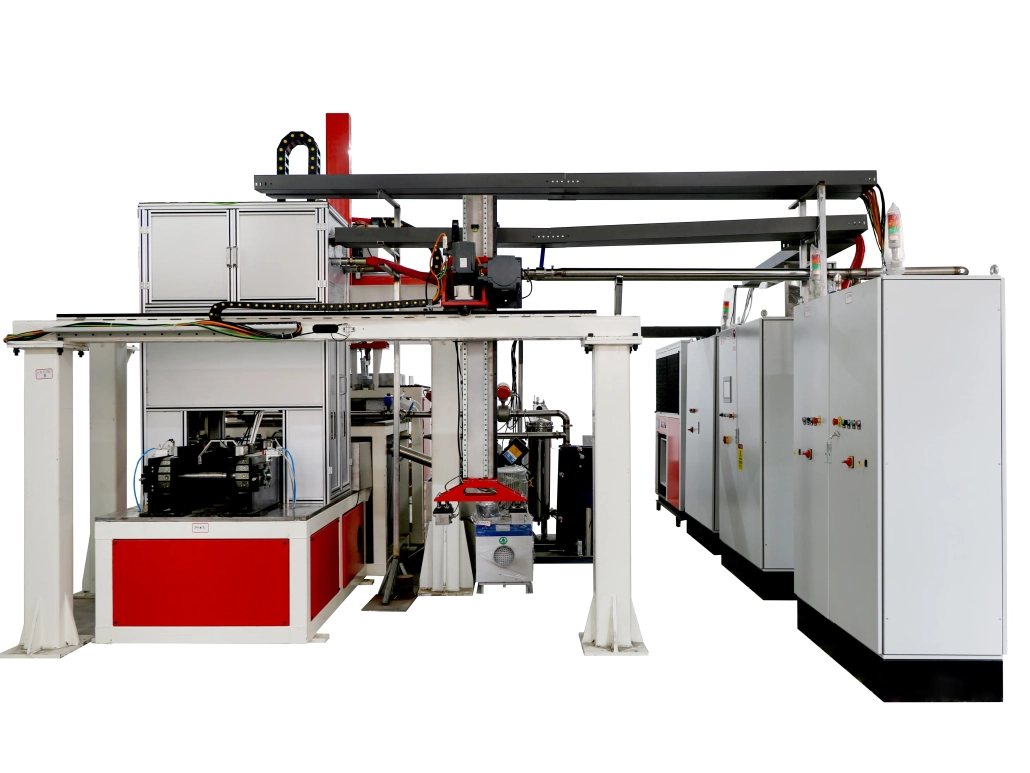
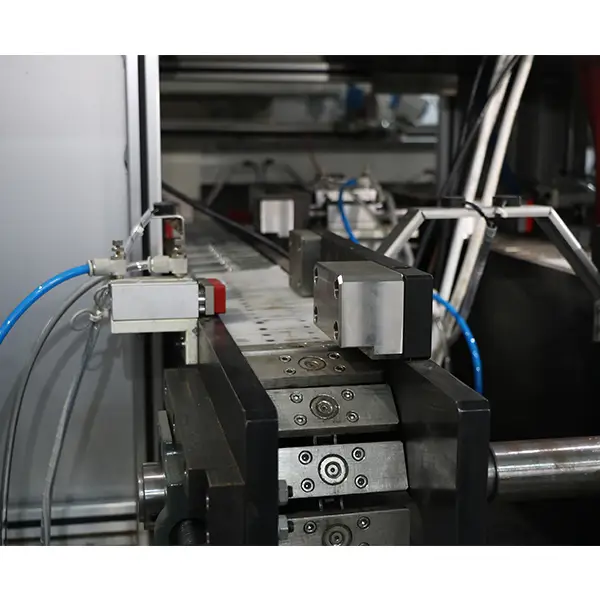
The clips show the automatic line running crawler track links through the full heat treatment process — gantry loading, induction heating, quenching, tempering and unloading. The vertical close-up focuses on the double-station hardening section.
Track links move from station to station in one continuous sequence, without manual handling between steps.
Ⅱ. How the Automatic Heat Treatment Line Works
This system is built as a complete production line, not a standalone hardening machine. The project brings together:
— One double-station intelligent induction hardening machine
— Tempering equipment
— Auxiliary automation equipment
— Gantry automatic loading
— Workpiece transfer
— Automatic counting
— Automatic unloading
— Energy and quality control analysis
The line connects with the unloading section of the upstream double-side milling process, so workpieces continue directly into heat treatment. The main production sequence is:
Double-Side Milling → Line Transfer → Gantry Loading → Induction Heating → Quenching → Tempering → Cooling → Counting → Unloading
After the track links enter the line, the gantry loading system places them at the hardening station. The tread then passes through induction heating and quenching. Hardened parts continue through tempering and cooling before counting and unloading, all coordinated as one automatic production sequence.
Ⅲ. Double-Station Processing for Left- and Right-Hand Track Links
The hardening section uses a double-station configuration. Left- and right-hand track links are loaded in one cycle and processed at the same time. The two parts are clamped once and complete the required processing simultaneously.
This arrangement is built around the production characteristics of crawler track links. Each left- and right-hand pair is treated as one workpiece set rather than two separate standalone operations.
The line also handles track links with different pitches within the applicable processing range. Tooling and process settings are matched to the workpiece being produced.
Ⅳ. Induction Hardening and Tempering of the Track Link Tread
The tread — the running surface — is the main area this line treats. In service, the surface sees repeated contact, wear and impact. Induction hardening strengthens that working surface while the rest of the component is left untreated.
The process starts with medium-frequency induction heating of the tread. Once the required area reaches temperature, the workpiece enters the quenching stage for rapid cooling and surface hardening.
The process does not stop at quenching. The hardened track link continues to the tempering section, followed by cooling after tempering. Hardening and tempering are therefore integrated into the same automatic line.
The complete sequence is:
Induction Heating → Quenching → Tempering → Cooling
This gives the line a different role from a conventional single-purpose induction hardening machine.
Ⅴ. DSP Medium-Frequency Induction Heating
The hardening section uses DSP-controlled medium-frequency induction heating equipment. DSP digital control manages the heating process, with power set through the program and adjustable manually when required.
Medium-frequency heating brings the track link tread to temperature before quenching. The induction power supply operates together with the hardening machine and automatic line control, not as an independent heating unit. See the medium-frequency induction heating system page for the power supply range.
For repeated production, heating parameters are incorporated into the programmed process, so the heating stage stays coordinated with loading, positioning, quenching and subsequent tempering.
Ⅵ. Technical Configuration and Process Monitoring
The following table describes the current XZZ-300kW double-station automatic hardening project configuration.
| Item | Configuration |
|---|---|
| Equipment | XZZ-300kW Double-Station Automatic Hardening Equipment |
| Hardening Machine | 1 Double-Station Intelligent Induction Hardening Machine |
| Tempering | Tempering Equipment |
| Loading Method | Gantry Automatic Loading |
| Heating Method | DSP Medium-Frequency Induction Heating |
| Workpiece | Crawler Track Link |
| Treated Area | Track Link Tread / Running Surface |
| Processing Arrangement | Left- and right-hand track links processed simultaneously |
| Clamping | Left- and right-hand links completed with one clamping cycle |
| Main Functions | Loading, heating, quenching, tempering, counting and unloading |
| Upstream Connection | Can connect with the unloading section of the double-side milling process |
| Quality Monitoring | Energy and Quality Control Analysis System |
The XZZ-300kW designation refers to this project configuration and should not be treated as a fixed specification for every track link heat treatment line. Other workpiece-specific lines, such as the automatic gear induction hardening machine, follow the same approach of matching tooling and process settings to the workpiece.
Energy and Quality Control. The line carries an energy and quality control analysis system that monitors the induction hardening process during production. On a continuously running line, this reports the stability and consistency of the heating stage across repeated cycles. The monitoring system is part of the line itself, not a separate manual inspection step.
Ⅶ. Frequently Asked Questions
What part of the track link is heat treated?
The line treats the track link tread, also referred to as the running surface.
Does the line include tempering?
Yes. The process includes induction heating, quenching, tempering and cooling after tempering.
Can left- and right-hand track links be processed together?
Yes. The double-station hardening machine lets left- and right-hand links be clamped once and processed simultaneously.
Can the line process different track link pitches?
Yes, within the applicable processing range. Tooling and process settings are matched to the workpiece specification.
Can the line connect with upstream machining equipment?
Yes. In this project the line connects with the unloading section of the preceding double-side milling process for continuous workpiece transfer.
The automatic track link tread induction hardening and tempering line combines workpiece handling, induction heating, quenching, tempering and process monitoring in one production system. Its double-station arrangement allows corresponding left- and right-hand track links to be processed together, while the automatic conveying and gantry loading equipment connect the different production stages into one continuous process.
Spec Your Track Link Hardening Line
Tell us the track link pitch, material and required case depth. We will match tooling, process settings and the line configuration to your workpiece.