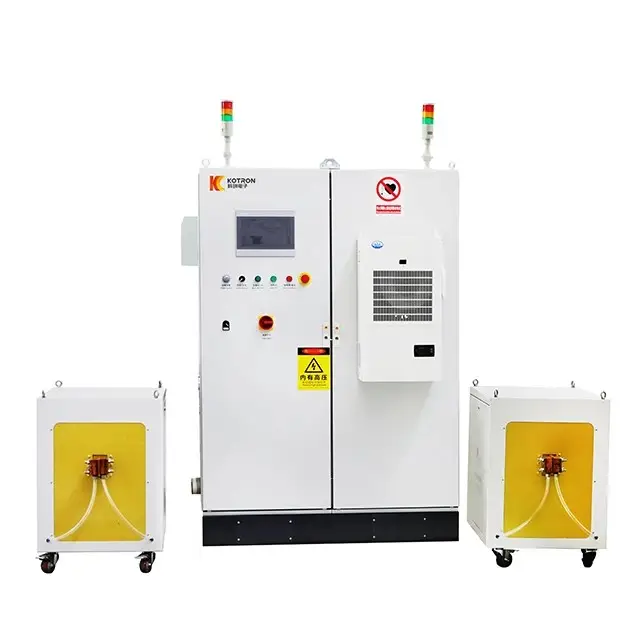
Induction heating treatment production line for Steel wire
Induction heating treatment production line for Steel wire is a highly efficient and energy-saving continuous processing equipment, specifically engineered for the softening, recrystallization, or spheroidizing annealing of metal wires (such as high-carbon steel, stainless steel, and alloy steel wires). By utilizing induction heating to replace traditional gas furnaces or resistance furnaces, this line significantly enhances production efficiency and temperature control precision.
Product Details
I. Core Components of the Production Line
| Module | Function Description |
|---|---|
| Uncoiling System | Automatic bobbin uncoiler integrated with servo tension control (±3N accuracy), capable of adapting to wire speeds ranging from 10 to 500 meters per minute. |
| Induction Heating Unit | Multi-stage medium/high-frequency inductor (frequency: 1–50 kHz), with a power output of 50–1000 kW, supporting segmented temperature control (400–1100°C). |
| Cooling and Slow Cooling System | Water-cooling tunnel (for rapid cooling) combined with air-cooling/atomized cooling (for controllable slow cooling), featuring adjustable cooling rates from 1 to 100°C per second. |
| Atmosphere Protection Device | Nitrogen/hydrogen sealed enclosure (oxygen content ≤10 parts per million), designed to prevent oxidation and achieve bright annealing (surface roughness Ra ≤0.6 micrometers). |
| Intelligent Control System | PLC-based control system integrated with temperature closed-loop feedback, wire speed-power control, energy consumption monitoring, and data traceability (compatible with MES integration). |
| Post-Processing Module | Online oil coating/coating application, eddy current flaw detection, automatic coiling (onto bobbins or drums), and support for fixed-length cutting and coil changeover. |
II. Technical Characteristics and Advantages
-
High Efficiency and Energy Savings
- Rapid Heating: Induction heating acts directly on the steel wire’s surface, achieving a heating rate of 100–500°C per second (5–10 times faster than traditional furnaces), with wire speeds reaching up to 500 meters per minute for Φ0.5mm steel wire.
- Low Energy Consumption: With an electrothermal conversion efficiency of ≥85%, the comprehensive energy consumption is only 0.15–0.3 kWh per kilogram (30–50% of that of traditional gas furnaces).
-
Precise Temperature Control and Quality Enhancement
- Segmented Temperature Control:
- Preheating zone: 400–600°C
- Soaking zone: target temperature (e.g., 750–900°C for high-carbon steel)
- Slow cooling zone: 500–300°C
Temperature fluctuations are controlled within ±5°C.
- Microstructural Uniformity:
Through rapid austenitization and controlled cooling, the grain size meets ≤Grade 8 (ASTM standard), with tensile strength variations ≤±15 MPa.
- Segmented Temperature Control:
-
Flexibility and Environmental Friendliness
- Multi-Material Compatibility:
By adjusting the frequency (high frequency for thin wires, medium frequency for thick wires) and power, the line is compatible with Φ0.2–10mm steel wires (including high-carbon steel, stainless steel, and titanium alloy). - Zero Emissions: Free from combustion exhaust gases and featuring nitrogen recycling, the line complies with ISO 14001 environmental standards.
- Multi-Material Compatibility:
III. Typical Technical Parameters
| Project | Parameter Range | Application Scenario |
|---|---|---|
| Wire Diameter Range | Φ0.2–10 mm | Steel cord, tire bead wire, spring wire, welding wire |
| Annealing Temperature | 400–1100°C (material-specific; e.g., 1050°C for 304 stainless steel) | Recrystallization annealing, spheroidizing annealing, solution treatment |
| Wire Speed | 50–500 m/min (Φ0.5mm steel wire can reach 500 m/min) | High-speed continuous production (integrated with drawing/plating lines) |
| Cooling Rate | 1–100°C/s (programmable adjustment for water/air cooling) | Controlling pearlite proportion and eliminating internal stress |
| Annual Production Capacity | 10,000–200,000 tons (dependent on wire diameter and speed) | Large-scale wire manufacturing plants, special metal products enterprises |
V. Selection and Usage Recommendations
-
Process Requirement Analysis:
- Material and annealing type: high-carbon steel (spheroidizing annealing), stainless steel (solution annealing), alloy steel wire (recrystallization annealing).
- Surface quality requirements: whether bright annealing (with protective atmosphere) is needed or oxidation is acceptable (with subsequent pickling).
-
Priority of Key Configurations:
- Induction Frequency:
- For Φ0.2–2 mm steel wire: 50–100 kHz high frequency for rapid surface heating;
- For Φ2–10 mm steel wire: 1–10 kHz medium frequency for deep penetration heating.
- Cooling System:
- Water cooling: suitable for rapid cooling of high-strength steel wires (e.g., piano wire);
- Air-cooling/mist cooling: suitable for slow cooling of medium-low carbon steel wires to prevent embrittlement.
- Induction Frequency:
-
Maintenance and Cost Control:
- Daily inspection of inductor insulation and cooling water flow (≥20 liters per minute), with monthly calibration of the temperature measurement system.
- Adoption of domestic nitrogen generators instead of imported gas storage tanks to reduce gas supply costs.