Induction Heating System for Steel Tube End Forming
Ⅰ. Watch Induction Heating for Steel Tube End Forming
Video: Medium-frequency induction heating of a steel tube end followed by press forming.
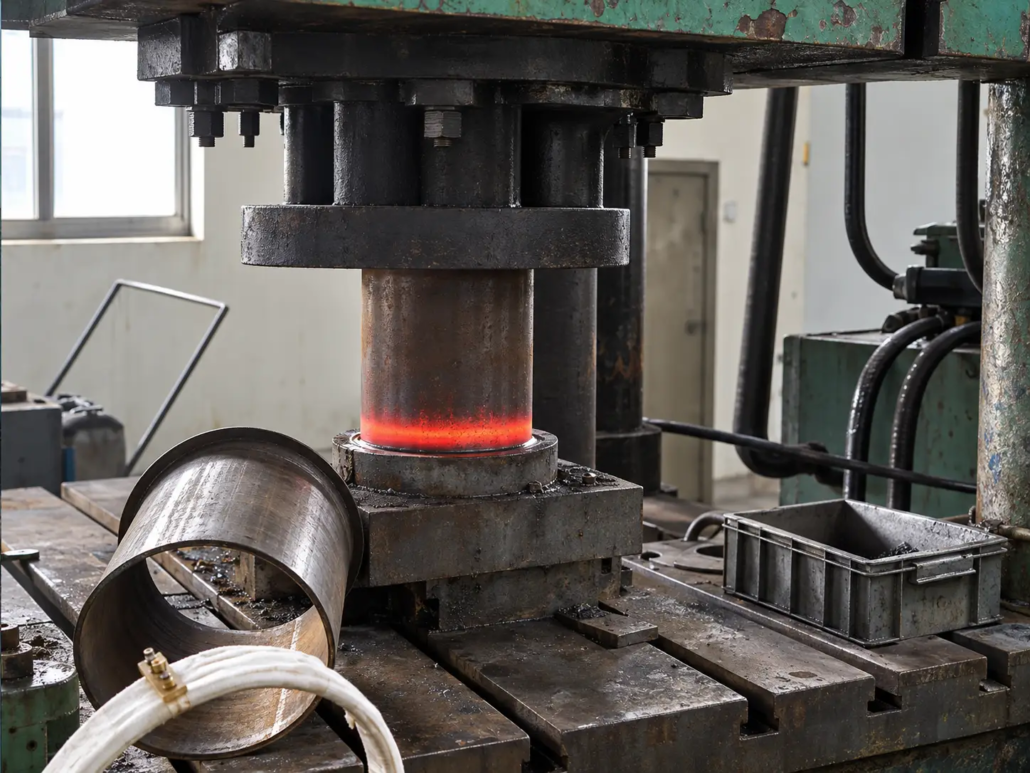
The video demonstrates localized induction heating before a mechanical tube end forming operation.
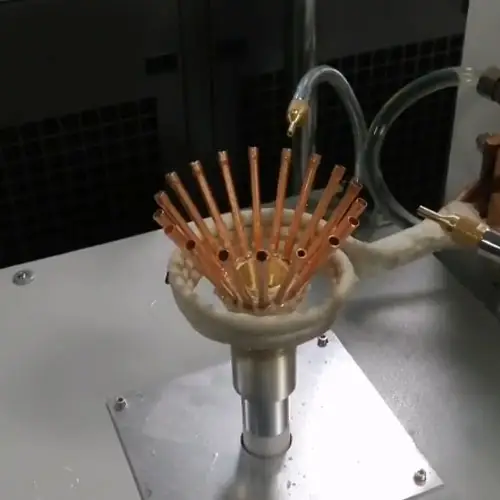
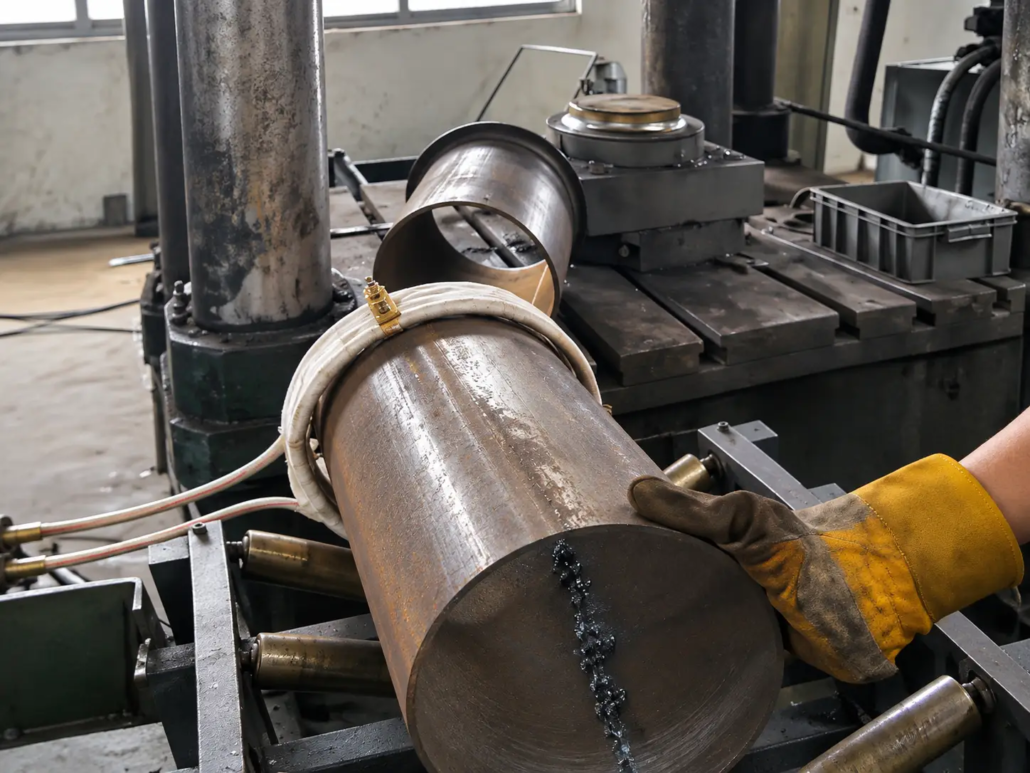
A circular induction coil surrounds the tube near its end, concentrating heating in the section to be formed. The heated tube is then processed using a press and forming tooling.
The demonstration shows how induction heating can be combined with mechanical forming without requiring the entire tube to undergo the same heating cycle.
Application Details
| Item | Description |
|---|---|
| Workpiece | Round steel tube |
| Heating Area | Tube end |
| Heating Method | Medium-frequency induction heating |
| Application | Tube end forming |
| Demonstrated Process | Tube end expansion |
| Forming Equipment | Press with forming tooling |
| Inductor | Circular induction coil for localized tube-end heating |
The video shows the heating and forming operations. The steel grade, heating temperature, dimensional tolerances and finished-part inspection results have not been specified.
Ⅱ. Tube End Forming Applications
Tube end forming changes the geometry of a selected tube section through mechanical deformation. Depending on the material, wall thickness and required dimensional change, forming may be performed cold or with localized heating.
Induction heating is particularly relevant when the required deformation is difficult to achieve under cold-forming conditions.
Tube End Expansion
Tube end expansion increases the diameter of a selected tube section.
For applications involving substantial diameter changes, localized heating may reduce forming resistance and improve the material’s ability to accommodate deformation.
This is the primary application demonstrated in the video.
Tube End Flaring
Flaring forms the tube opening outward, typically producing a tapered or flared profile.
The required heating conditions depend on the flare geometry, steel grade and wall thickness. Flaring tooling must be designed for the intended finished shape.
Tube End Reduction
Tube end reduction decreases the diameter of a selected section using suitable forming dies.
For certain materials and reduction requirements, induction heating may be used before forming. The suitability of this approach depends on the material, forming ratio and tooling arrangement.
Expansion, flaring and reduction are distinct forming operations. Each requires an appropriate process and die design.
Potential Industrial Applications
| Industry | Typical Application |
|---|---|
| Hydraulic Equipment Manufacturing | Tube ends prepared for fittings and connections |
| Automotive Tube Manufacturing | Formed ends of selected steel tubular components |
| Industrial Tube Fabrication | Tube expansion, reduction and connection preparation |
| Mechanical Equipment Manufacturing | Custom tubular components requiring end forming |
| Structural Tube Fabrication | Selected tube-end forming and joining applications |
These are potential application areas rather than confirmed end uses of the workpiece shown in the video.
Ⅲ. Why Use Localized Induction Heating Before Forming?
Cold tube end forming can become difficult when the required deformation exceeds what the material can accommodate under the selected processing conditions.
Possible defects include cracking, splitting, wrinkling and excessive wall thinning. Their occurrence depends on the steel grade, wall thickness, forming ratio and die design.
For suitable materials, localized induction heating can reduce resistance to deformation and improve formability by raising the temperature of the section being formed.
This approach allows the heating process to focus on the tube end while the remaining length receives less direct heat input.
The objective is to establish a suitable forming condition in the required region, rather than heat the complete tube uniformly.
Heating Temperature and Distribution
The tube end must reach a temperature appropriate for the material and forming operation.
Insufficient heating may leave the material difficult to deform. Excessive heating can introduce unnecessary oxidation, dimensional changes or undesirable metallurgical effects.
Heating power, frequency, duration and inductor design must therefore be selected together.
Forming Quality
Localized heating may help reduce cracking associated with excessive cold-forming strain, but it does not eliminate forming defects.
Final dimensions, wall thickness and surface condition also depend on the initial tube geometry, temperature distribution, die profile and forming operation.
The heating system and forming tooling must be evaluated as parts of the same process.
Ⅳ. Customized Induction Coil and Workpiece Tooling
The induction coil determines where electromagnetic energy is coupled into the tube and influences the resulting heating distribution.
For tube end forming, the coil is generally designed around the tube diameter and the required heated length.
Induction Coil Design
The main design considerations include:
— Tube outside diameter and wall thickness.
— Material and magnetic properties.
— Required heated length.
— Coil-to-workpiece clearance.
— Heating temperature and cycle requirements.
— Available space for positioning and handling.
A circular inductor can provide heating around the tube circumference. The actual temperature distribution depends on the coil geometry, electrical settings, workpiece properties and heating duration.
Different tube sizes or heating requirements may require changes to the inductor or operating parameters.
Workpiece Positioning
The tube must be positioned so that the intended forming section is located within the heating area.
Supports, stops or positioning fixtures may be used to establish the required insertion depth and maintain clearance between the tube and inductor.
The tooling arrangement is selected according to tube length, weight, dimensions and the production method.
Ⅴ. Equipment Configuration and Selection
The induction heating system can be supplied as a separate heating station for an existing press or incorporated into a more integrated tube end forming arrangement.
The equipment configuration is determined by the required heating cycle, forming operation and production conditions.
| Equipment Component | Configuration |
|---|---|
| Induction Power Supply | Power and frequency matched to the heating requirement |
| Induction Coil | Customized to the tube dimensions and heated length |
| Workpiece Fixture | Tube support and positioning |
| Process Control | Power and heating-time regulation; temperature feedback where required |
| Equipment Cooling | Matched to the power supply and inductor |
| Press Integration | Workpiece transfer and coordination with forming equipment |
| Automation | Loading and handling according to production requirements |
Power Supply and Control
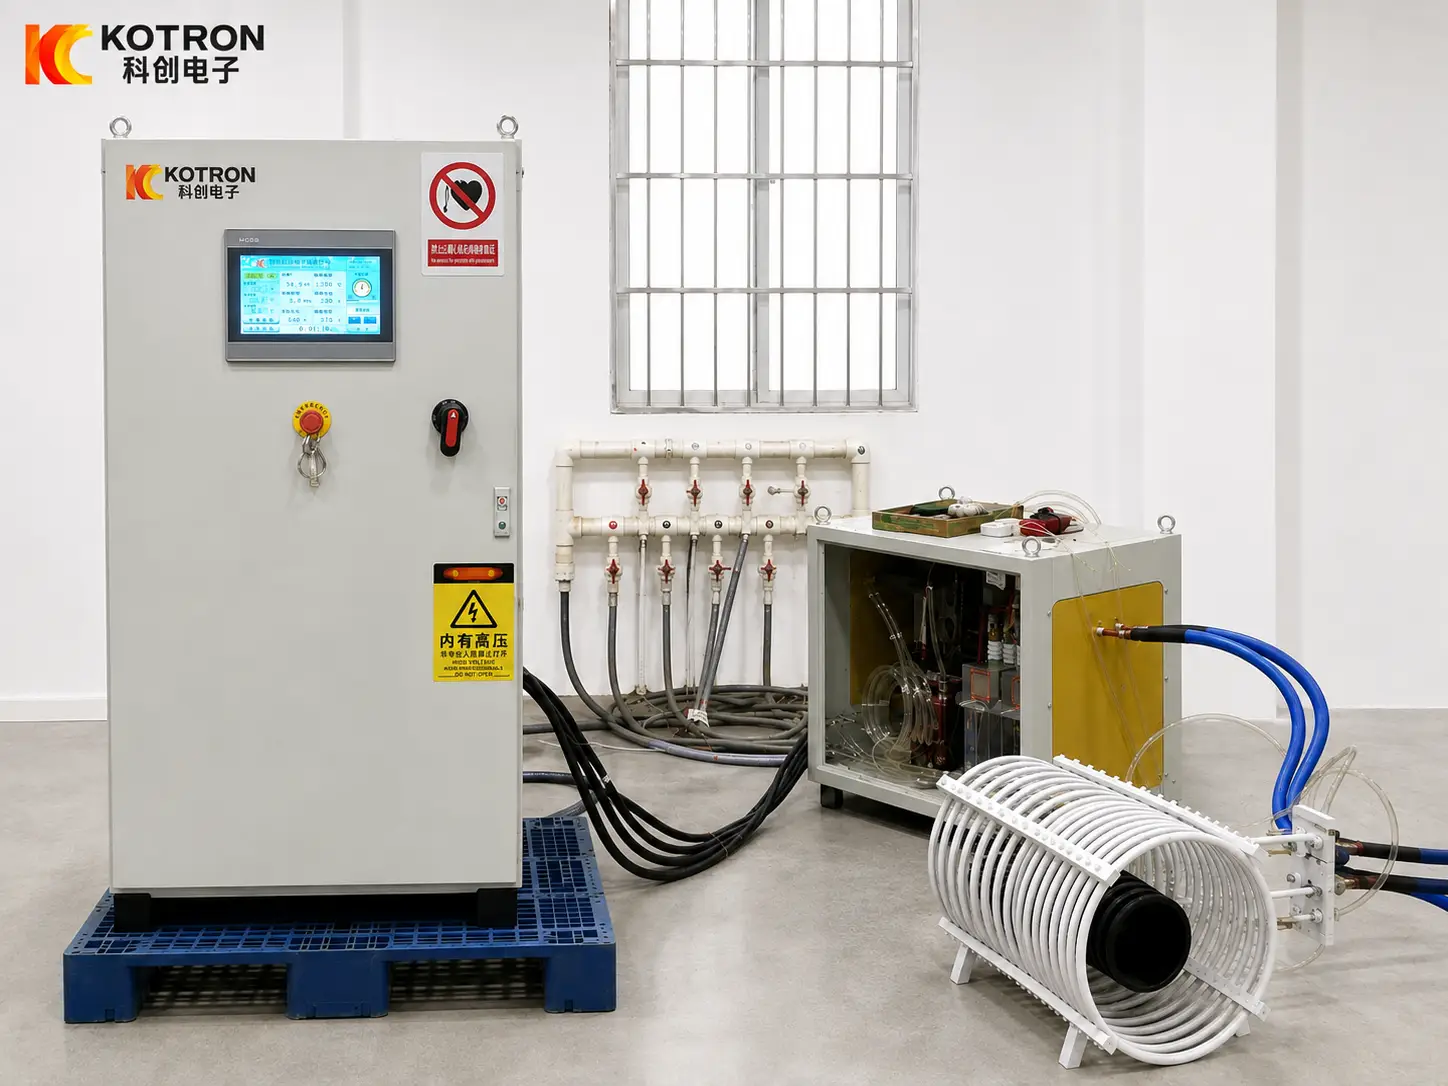
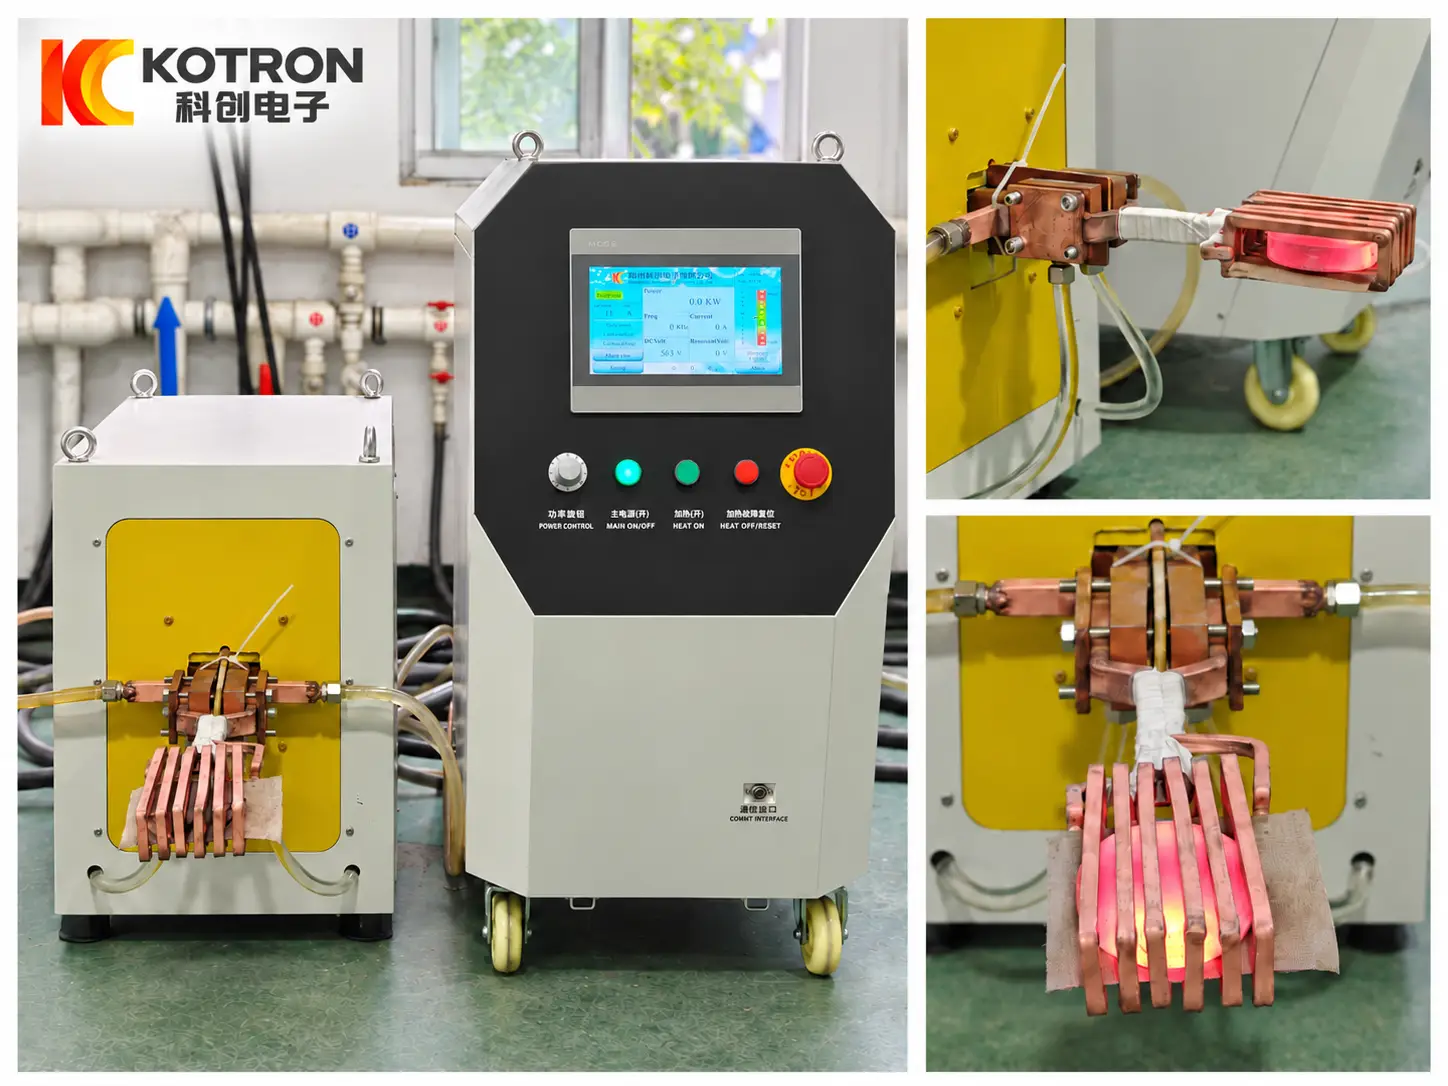
The demonstrated application uses medium-frequency induction heating. KOTRON’s available equipment includes digitally controlled power supplies, with temperature-feedback control available in suitable configurations.
The final electrical configuration is selected together with the inductor and required heating cycle.
Press Integration and Production
The interval between heating and forming must be considered because the tube begins losing heat after leaving the induction coil.
A manually operated heating station may suit occasional production, while repeated manufacturing may justify automated positioning and transfer.
For demanding forming requirements, process trials can help establish suitable heating conditions and verify the finished dimensions, wall thickness and surface condition.
Ⅵ. Frequently Asked Questions
Click a question to expand the answer.
Can induction heating help prevent cracking during tube end expansion?
For suitable materials, localized heating can improve formability and reduce the risk of cracking associated with excessive cold-forming strain. The result still depends on the material, temperature, forming ratio and tooling.
Can one induction heating system process different tube diameters?
Different tube sizes may be processed within the designed electrical and mechanical range. Changes in diameter, wall thickness or heated length may require different inductors, fixtures or heating settings.
Can the system be used for both tube expansion and reduction?
The same induction heating equipment may support both applications when their heating requirements are compatible. The forming operations require suitable tooling and may need different heating conditions.
Can the induction heater work with an existing press?
Yes. The heating equipment can be evaluated for integration with an existing forming machine. Workpiece positioning, transfer time, available space and process coordination must be considered.
Is induction heating before tube forming the same as annealing?
Not necessarily. Heating a tube end before press forming is a preparation step intended to establish suitable deformation conditions.
Annealing is a defined heat-treatment process with its own thermal cycle and metallurgical objectives. The demonstrated application is therefore described as induction heating for tube end forming rather than induction annealing.
Ⅶ. Request a Customized Tube End Induction Heating Solution
If your application requires steel tube end expansion, reduction or another forming operation, KOTRON can evaluate a suitable induction heating system based on your workpiece and production requirements.
For an initial technical proposal, please provide:
— Tube drawing or photographs.
— Material or steel grade.
— Outside diameter and wall thickness.
— Required forming operation and finished dimensions.
— Production quantity or required cycle time.
If you already have a forming press, information about the existing equipment will also help KOTRON evaluate the heating arrangement and integration requirements.
Based on these details, KOTRON can assess the induction power supply, customized coil, workpiece positioning and required process control.
Need induction heating for steel tube end forming?
Send your tube drawing and KOTRON will evaluate a customized tube end induction heating solution.