
Induction Heating for Automotive Parts: A Practical Buyer’s Guide
For factories that need stable, repeatable heating in production—copper tube brazing, carbide tool brazing, pipe preheating, surface hardening, or heat treatment—the right induction heating equipment directly determines product quality, production speed, and operating cost. This guide covers what production managers, automation integrators, and purchasing teams should know before selecting an induction heating system.
Reader Roadmap
Production Manager? Jump to Section 4 (Applications) & Section 6 (Selection Process).
Automation Integrator? Focus on Section 3 (Automation & Monitoring).
Purchasing / Buyer? Start with Section 5 (Common Mistakes) & Section 6 (Selection Process).
| 1. Why equipment selection matters | 2. How the technology works |
| 3. Key selection factors | 4. Industrial application examples |
| 5. Common buying mistakes | 6. A simple selection process |
1. Why Equipment Selection Matters
An induction heater delivers fast, localized, and controllable heat without direct flame contact. But when equipment is selected incorrectly:
- Unstable heating quality—parts look hot, but actual joint temperature, case depth, or uniformity varies part to part. In brazing and hardening, small differences cause weak joints, cracking, or inconsistent hardness.
- Wrong power or frequency—too little power kills production speed; too much makes control harder and shortens coil life. Wrong frequency causes uneven heating or insufficient penetration depth.
- Automation and monitoring gaps—a system that works in manual testing may fail in automated production if PLC communication, real-time feedback, recipe management, and alarm signals are limited.
2. How the Technology Works
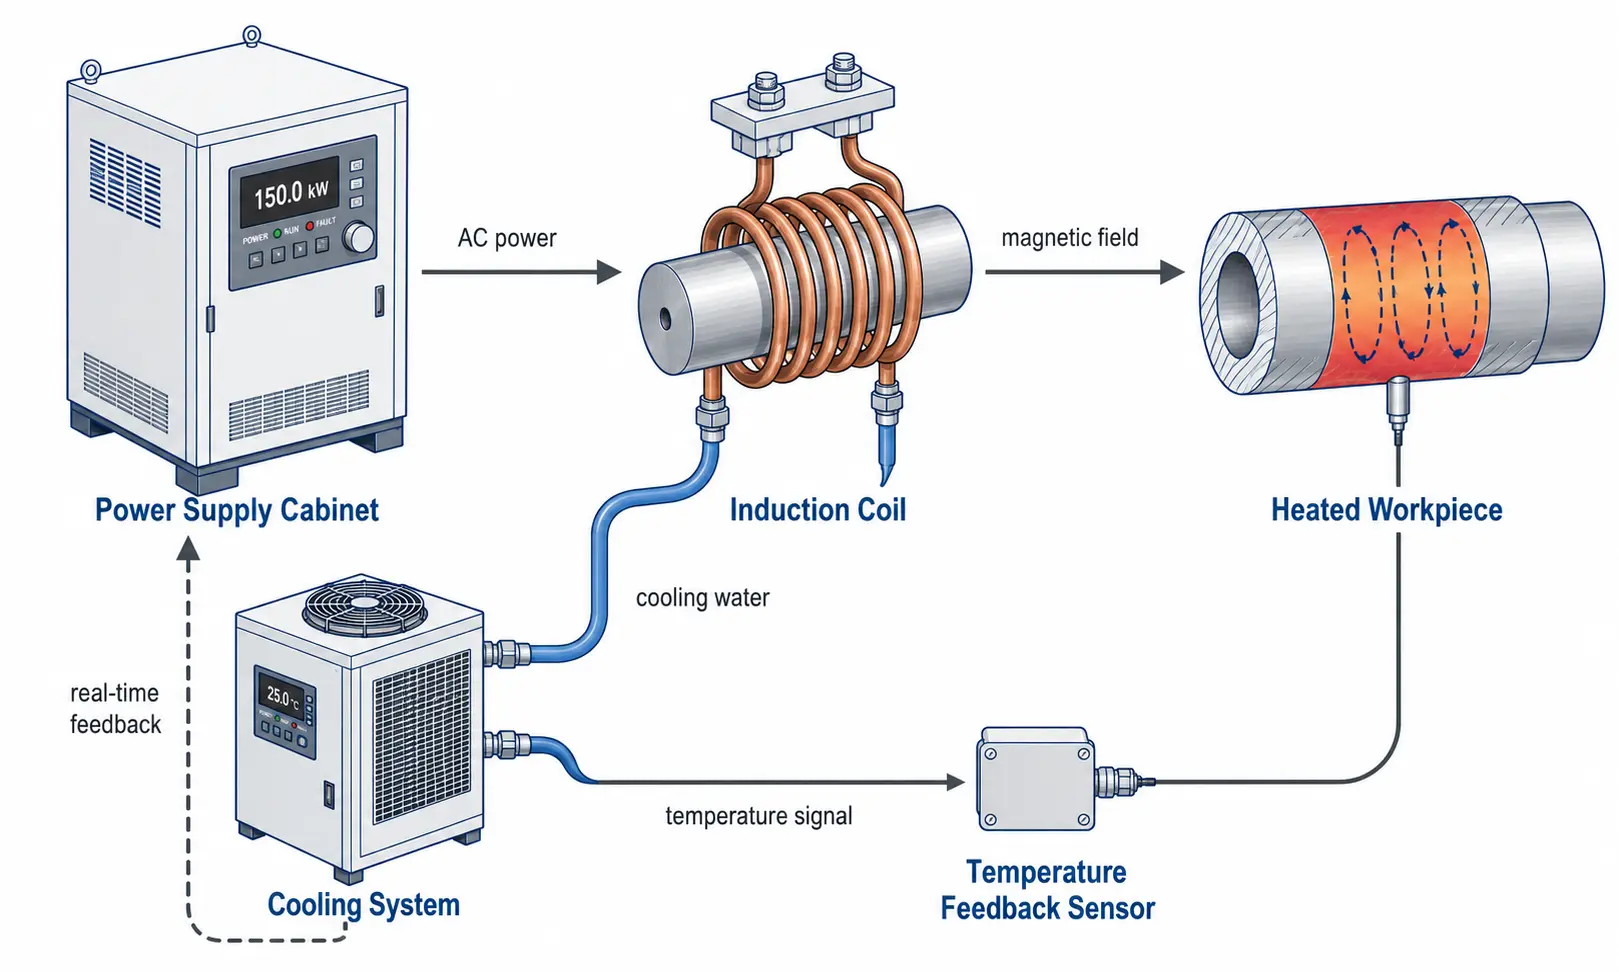
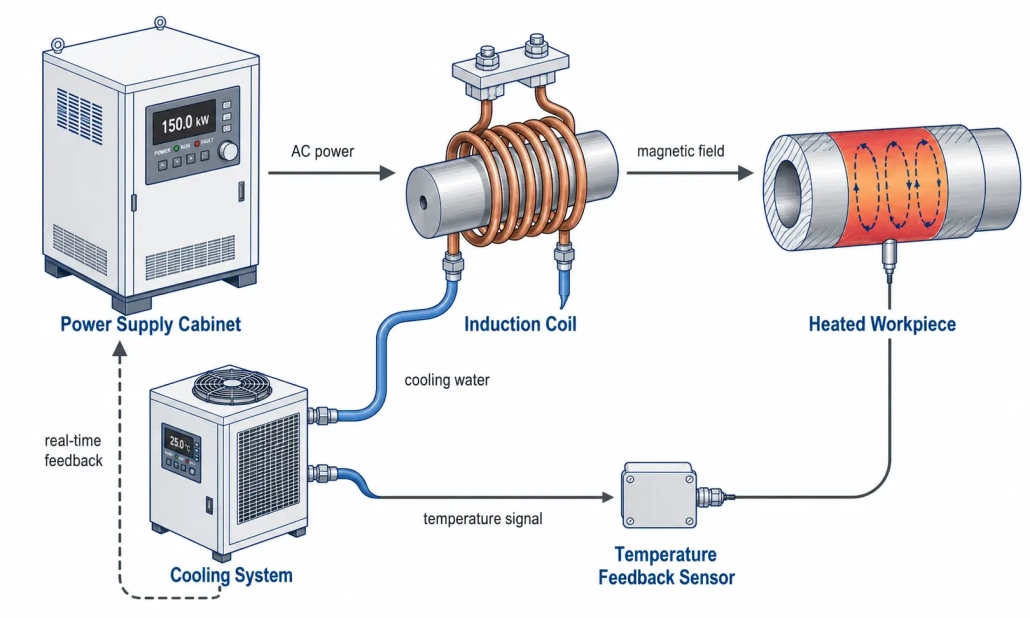
An induction heating system uses an alternating magnetic field to generate eddy currents inside a conductive workpiece. Heat is produced inside the metal itself—not transferred from an external flame. Four elements form one integrated system: the power supply delivers controlled energy, the coil converts it into a magnetic field, the workpiece absorbs it as heat, and the cooling system keeps everything stable. Because heating is non-contact, the process is clean, repeatable, and suited to automated lines. For the underlying physics, see our How Does Induction Heating Work? guide.
3. Key Selection Factors
Power Rating
How fast the system reaches target temperature within your cycle time. Size for your heaviest realistic part, not your average. A supply running at 60–70% capacity lasts longer than one pegged near 100% for full shifts. For detailed power calculations across applications, see our complete power selection guide.
Frequency Range
Controls heating depth. Higher frequency (100–400 kHz) = shallow surface heat for small parts and thin cases. Medium frequency (10–100 kHz) = general-purpose. Lower frequency (1–10 kHz) = deep penetration for large sections. Match to part size and heating objective—don’t pick from a catalog alone. See our frequency classification guide.
Coil Design
The coil is a process tool, not an accessory. Coil shape, turns, copper tube size, water cooling, and distance from the part all determine heating uniformity and efficiency. Even a top-tier power supply cannot compensate for a poorly designed coil.
Workpiece Material & Geometry
Steel heats efficiently. Copper and aluminum are more conductive—they need higher current and tighter coil coupling. Always provide material grade, dimensions, and the specific heating zone when talking to suppliers.
Automation Interface
If the system will integrate with robotic loading, rotary tables, or conveyor lines, confirm remote start/stop, PLC communication protocol, recipe storage, fault outputs, and real-time data output before ordering.
Cooling System
Induction equipment generates heat in the coil, power electronics, and output transformer. Size the chiller for sustained heat rejection, not peak rating—undersized cooling causes mid-shift trips and shortens component life. See our water cooling guide.
Process Monitoring
In production, repeatability beats maximum speed. Real-time power, energy, and temperature monitoring help flag missing parts, poor coil positioning, abnormal cycles, and batch-to-batch drift before scrap piles up.
4. Industrial Application Examples
Copper Tube Brazing
Clean, localized joint heating for HVAC, refrigeration, and fluid system assemblies. Replaces manual flame brazing with repeatable, operator-independent cycles.
- Material: Copper tube, brass or copper fittings
- Size: Tube OD typically 1/4″ to 2″
- Temperature: 640–730°C (BCuP silver-phosphorus filler)
- Coil: Ring-style or split coil with tight clearance (1–3 mm gap)
- Frequency: 15–50 kHz for general tube sizes
Carbide Tool Brazing
Carbide tool induction brazing process
Controlled heating at the carbide-steel interface so brazing alloy flows properly without thermal damage to the insert or uneven bonding.
- Material: Tungsten carbide insert, alloy steel shank
- Size: Insert mass 30–600 g
- Temperature: 650–700°C (BAg silver filler)
- Coil: Pancake or shaped coil concentrating heat at the joint
- Frequency: 150–250 kHz for localized interface heating
Pipe Heating & Welding Preheating
Uniform preheating before welding, post-weld heat treatment, or coating removal. Heating uniformity around the circumference is critical.
- Material: Carbon steel, alloy steel, stainless steel pipe
- Size: Pipe OD typically 2″ to 24″+
- Temperature: 150–350°C (preheat), 600–760°C (PWHT)
- Coil: Split or clamshell coil for pipe access
- Frequency: 1–10 kHz for deeper penetration on thick walls
Induction Hardening & Heat Treatment
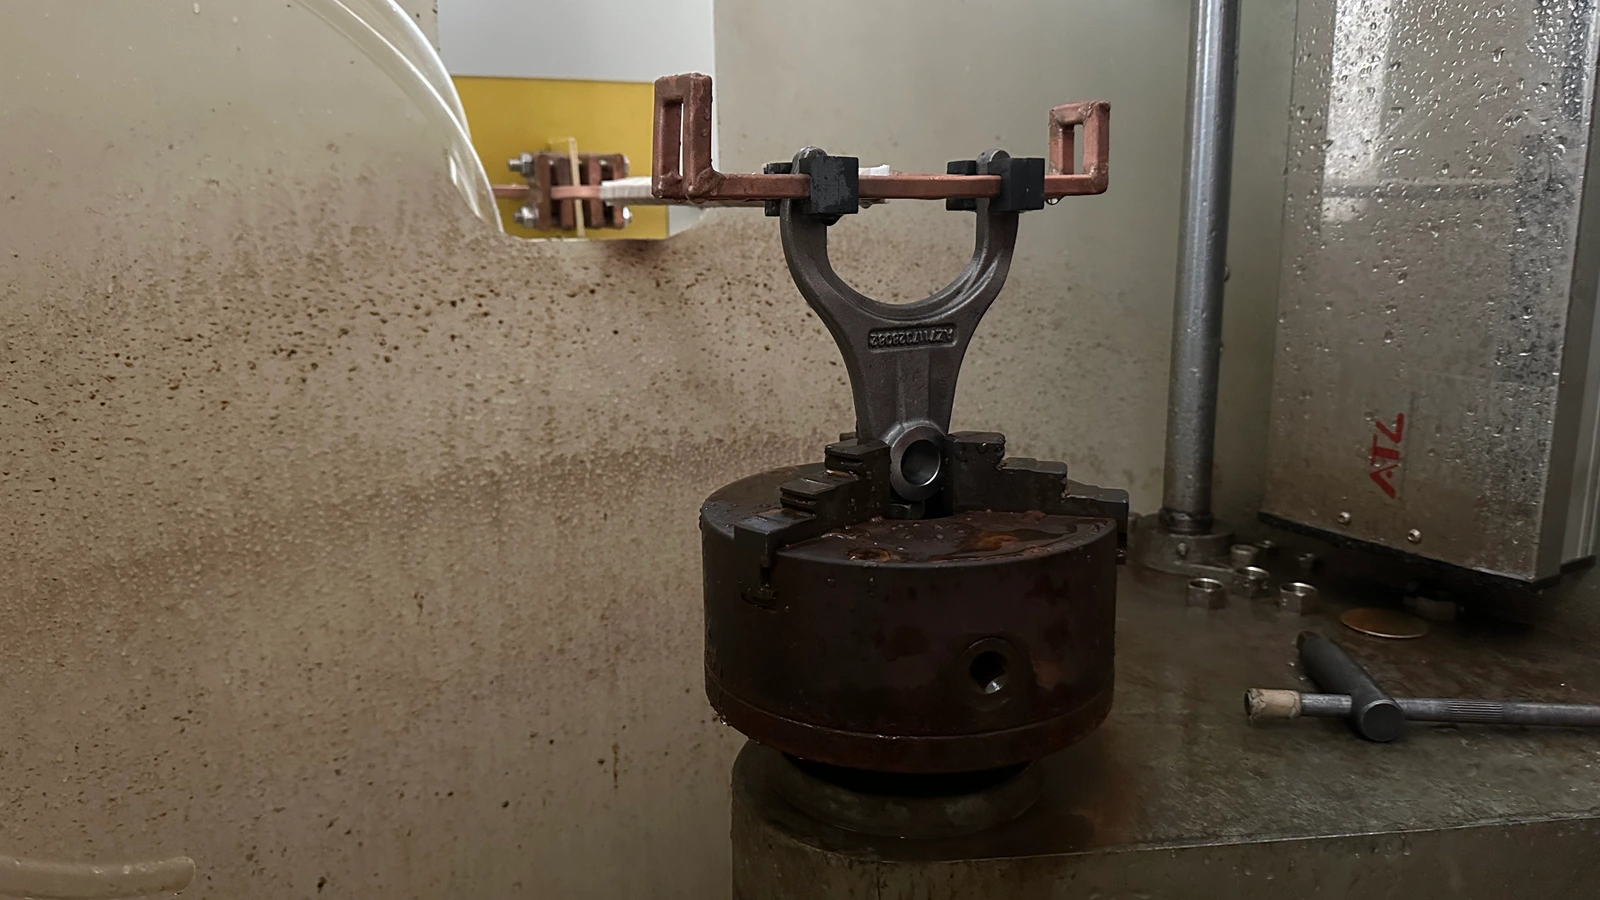
Fast surface heating followed by quenching to increase wear resistance on shafts, gears, pins, rollers, and shift forks.
- Material: Medium-carbon steel, alloy steel (1045, 4140, 4340)
- Size: Part diameter 10–80 mm typical
- Temperature: 850–950°C (austenitizing), followed by quench
- Coil: Single or multi-turn encircling coil, scan or static
- Frequency: 10–50 kHz for case depth 1–3 mm; 100–400 kHz for <1 mm
5. Common Buying Mistakes
| Mistake | What It Really Costs |
|---|---|
| Choosing by price alone | A lower upfront number hides weak frequency matching, undersized cooling, or limited controls. The long-term cost shows up in scrap rate, downtime, and maintenance. |
| Ignoring frequency | Two 15 kW induction heaters with different frequencies produce completely different results on the same part. Always match frequency to part material, size, and heating depth. |
| Treating the coil as an afterthought | The best power supply cannot fix a bad coil. Coil design controls where heat goes. Budget for application-specific coils, not generic ones. |
| Expecting one setup to handle everything | A flexible power supply can serve multiple part families, but coils, recipes, and fixtures usually need to be dedicated per family. |
| Skipping process monitoring | Without power, energy, or temperature data, you cannot prove quality to your customer or catch process drift before it becomes a reject batch. |
6. A Simple Selection Process
If you are evaluating induction heating equipment and don’t know where to start, work through these five steps in order. Each step narrows the field and gives you concrete numbers to discuss with suppliers.
| Step | What to Define | Why It Narrows Your Options |
|---|---|---|
| 1. Define the workpiece | Material grade, dimensions, mass, and the specific area that needs heating. | Material and mass determine minimum power. The heating zone determines coil shape and size. |
| 2. Set the heating objective | Brazing, hardening, preheating, or through-heating? Target temperature? Required cycle time? | Temperature + time = power. Process type (surface vs. through-heating) points to frequency range. |
| 3. Match power & frequency | Calculate required kW from mass, temperature rise, and time. Select frequency from heating depth and part size. | Eliminates 80% of available models. Now you’re comparing 3–5 viable options instead of 50. |
| 4. Specify coil & cooling | Coil geometry for part access. Cooling water flow rate, pressure, and chiller capacity for your duty cycle. | Coil defines heating uniformity. Cooling defines uptime—undersize it and the system trips mid-shift. |
| 5. Confirm automation & monitoring | PLC protocol, remote I/O, recipe count, temperature feedback, data logging, alarm outputs. | A supply that works in manual mode may not integrate with your line. Confirm interfaces before ordering. |
Work through these five steps, and you will have a shortlist of equipment that fits your actual production—not just a pile of datasheets. When you’re ready to discuss specifics, bring your workpiece drawings and target cycle time to the conversation. For a deeper look at power sizing, see our induction heating power selection resources.
7. Key Takeaway
Selecting an induction heating system for automotive parts comes down to matching five things to your actual production: power to your part mass and cycle time, frequency to your heating depth, coil geometry to your workpiece shape, cooling to your duty cycle, and controls to your automation level. Get these five right, and the rest falls into place. Early technical evaluation with real part samples prevents costly selection mistakes that are far more expensive than the price difference between an adequate supply and the right one.
Frequently Asked Questions
How do I choose the right power for an induction heating application?
Start with workpiece material, mass, target temperature, and required cycle time. Calculate the theoretical energy needed, add 30–50% for coil coupling losses, then validate with a real part test. Catalog numbers are a starting point, not a final answer.
Is high frequency or medium frequency better?
Neither is universally better. Choose based on required heating depth: high frequency (100–400 kHz) for shallow surface heating under 1 mm; medium frequency (10–100 kHz) for general brazing and case depths of 1–3 mm; low frequency (1–10 kHz) for deep through-heating of large sections.
Can one induction heating system handle multiple part types?
A flexible power supply with wide frequency range and stored recipe profiles can serve multiple part families. However, dedicated coils and fixtures are almost always needed per part family. Expect to invest in application-specific tooling even if the power supply stays the same.
What information should I prepare before contacting a supplier?
Workpiece drawings with material grade and dimensions, the specific heating zone, target temperature, required cycle time or production rate, available facility power and cooling water, and any automation interface requirements. A sample part is worth more than a dozen emails.
Need Help Selecting Induction Heating Equipment?
Tell us your workpiece material, heating area, target temperature, and cycle time—our engineers will recommend a power supply and coil configuration matched to your production.










